

Working Principle and Characteristics of Pulsed Powder Pneumatic Conveying
HeadPowder, a leading manufacturer in the field, specializes in advanced pneumatic conveying systems, particularly the pulsed powder type. This technology is widely used in various industrial applications for efficient and reliable powder transport. The following sections will delve into the working principle and key characteristics of this system.
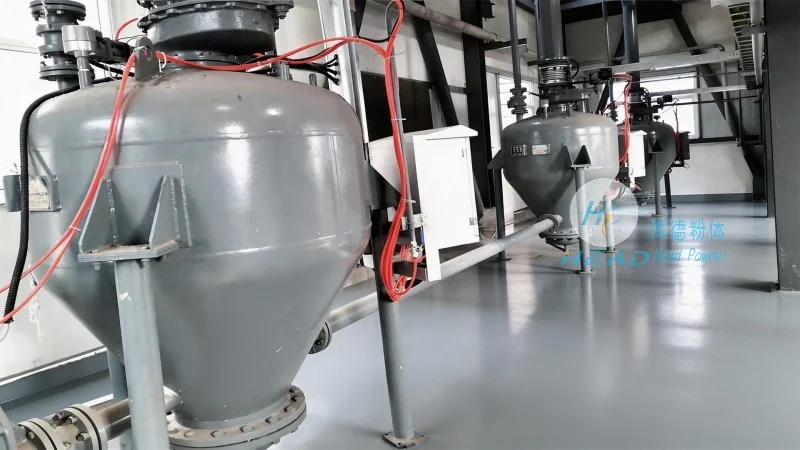
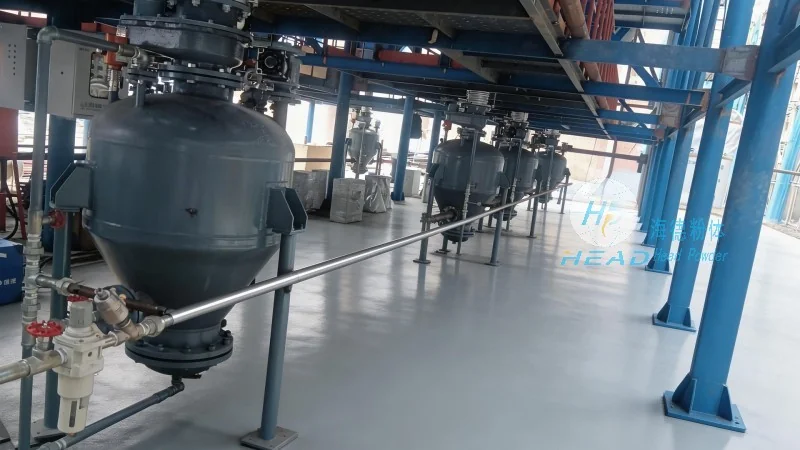
Working Principle of Pulsed Powder Pneumatic Conveying
The pulsed powder pneumatic conveying system operates by utilizing a compressed air source to create a series of pulses that propel powder particles through a pipeline. The process begins with the powder being fed into a hopper, where it is then drawn into the conveying line by the pressure differential generated by the pulses. The compressed air, delivered in short bursts, creates a high-velocity flow that carries the powder particles forward. This method ensures that even fine or cohesive powders can be transported over long distances without clogging or degradation. The system typically includes components such as a hopper, a pulse generator, a filter, and a receiver, all working in tandem to maintain consistent flow and pressure.
Key Characteristics of Pulsed Powder Pneumatic Conveying
Several distinct characteristics make pulsed powder pneumatic conveying an attractive option for industrial applications. First, it offers high efficiency in transporting powders, with the ability to handle a wide range of particle sizes and moisture contents. The system is also known for its flexibility, as it can be easily adjusted to accommodate different powder types and conveying distances. Another notable feature is its low maintenance requirements, as the components are designed to withstand continuous operation without frequent repairs. Additionally, the system provides excellent control over the conveying process, allowing for precise regulation of flow rates and pressure. This level of control is crucial in applications where product quality and consistency are paramount. The use of compressed air as the primary medium also contributes to a clean and hygienic operation, which is essential in industries such as food, pharmaceuticals, and chemicals.
Applications and Benefits
HeadPowder's pulsed powder pneumatic conveying systems are applied in numerous industries, including food processing, pharmaceutical manufacturing, chemical production, and mining. The benefits of this technology extend beyond efficiency, as it also reduces material handling costs and minimizes product loss during transport. The system's ability to handle abrasive or corrosive powders makes it suitable for harsh environments, while its compact design allows for installation in limited spaces. Furthermore, the system's reliability ensures minimal downtime, which is critical for maintaining production schedules. In summary, pulsed powder pneumatic conveying offers a robust and versatile solution for powder transport, aligning with the needs of modern industrial operations.