With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Phosphorus pentachloride (PCl₅) is a critical chemical compound widely used in various industrial applications, including pharmaceuticals, agrochemicals, and chemical synthesis. The efficient and safe handling of PCl₅ powder is essential due to its reactivity and potential hazards. This article explores the working principle and key features of the PCl₅ powder conveying system equipment designed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
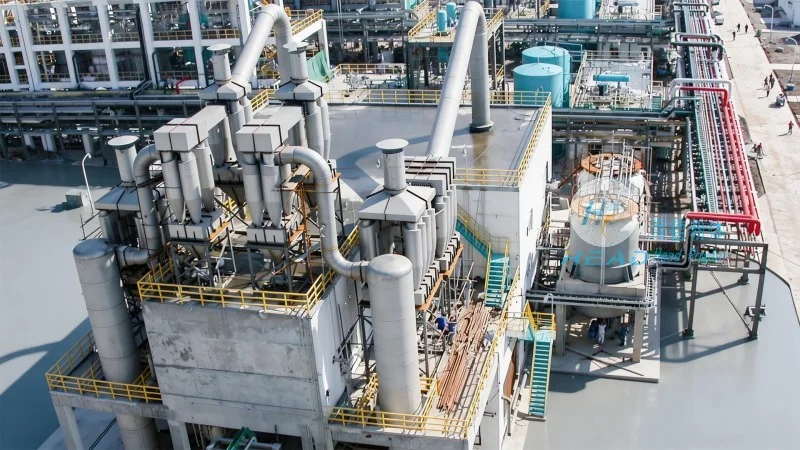
The PCl₅ powder conveying system operates on a closed-loop mechanism to ensure safe and controlled transport of the material. The system typically consists of several interconnected components, including a hopper for material storage, a rotary valve for controlled discharge, a conveyor (such as a pneumatic or mechanical conveyor), and a dust collection system. The process begins with the PCl₅ powder being fed into the hopper from a storage silo or batch container. A rotary valve then regulates the flow of powder into the conveyor, preventing overfilling and maintaining a consistent feed rate. The conveyor transports the powder to the destination, such as a reactor or processing unit, while the dust collection system captures any airborne particles to ensure environmental compliance and operator safety.
A key aspect of the system's operation is the use of a sealed, inert gas environment, often nitrogen or dry air, to prevent the PCl₅ from reacting with moisture or oxygen in the air. This inert gas atmosphere is maintained throughout the conveying process, reducing the risk of exothermic reactions and ensuring the material remains stable. The system also incorporates sensors and controls to monitor pressure, temperature, and flow rates, providing real-time feedback to operators and enabling automatic adjustments if necessary.
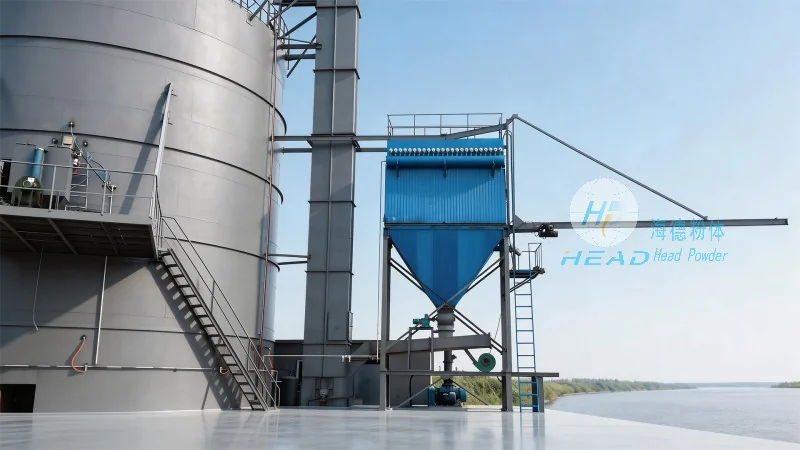
The PCl₅ powder conveying system from Shandong HeadPowder Engineering Co., Ltd. is engineered with several advanced features that enhance performance, safety, and reliability. One of the primary features is its fully enclosed design, which minimizes exposure to the environment and reduces the risk of dust contamination or material degradation. The system is constructed from corrosion-resistant materials, such as stainless steel or specialized alloys, to withstand the chemical properties of PCl₅ and prevent contamination of the product.
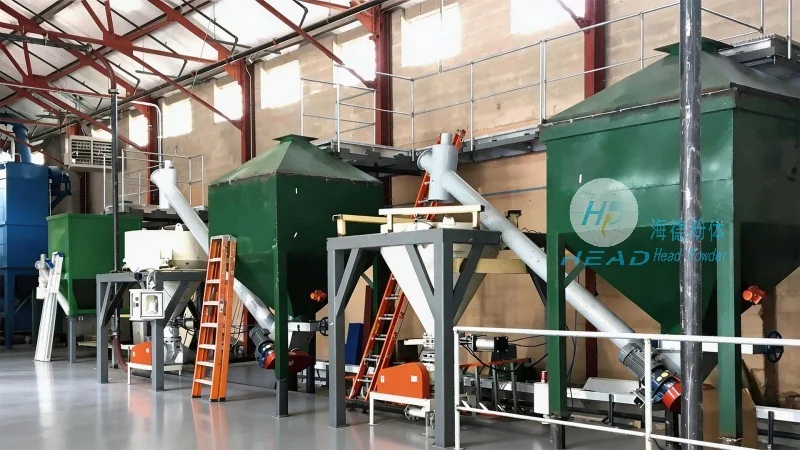
Another significant feature is the integration of a dust suppression and filtration system. This system captures and filters any airborne particles, ensuring compliance with environmental regulations and protecting operators from inhalation hazards. The filtration system typically includes high-efficiency particulate air (HEPA) filters or similar technology to achieve sub-micron particle capture rates.
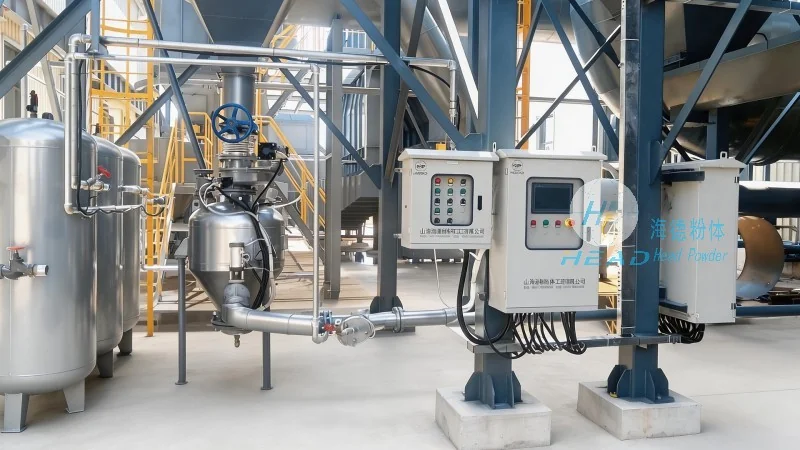
The conveying system also features adjustable speed and flow controls, allowing operators to optimize the transport rate based on process requirements. This flexibility is crucial for maintaining consistent material feed to downstream equipment, such as reactors or mixers. Additionally, the system includes emergency shut-off valves and pressure relief devices to prevent over-pressurization and ensure safety in case of system malfunctions.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a reputable manufacturer specializing in powder handling and conveying systems. The company is headquartered in Shandong, China, and has established a strong presence in the chemical processing industry with its innovative and reliable equipment solutions. With a focus on safety, efficiency, and customer satisfaction, headpowder provides tailored solutions for various chemical applications, including the handling of hazardous materials like phosphorus pentachloride.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top