

Working Principle and Features of Stone Aggregate Pneumatic Conveying Equipment
For industries dealing with stone aggregates, efficient material handling is crucial. The pneumatic conveying system, particularly designed for stone aggregates, offers a reliable solution. This article explores the working principle and key features of such equipment, highlighting its advantages and practical applications.
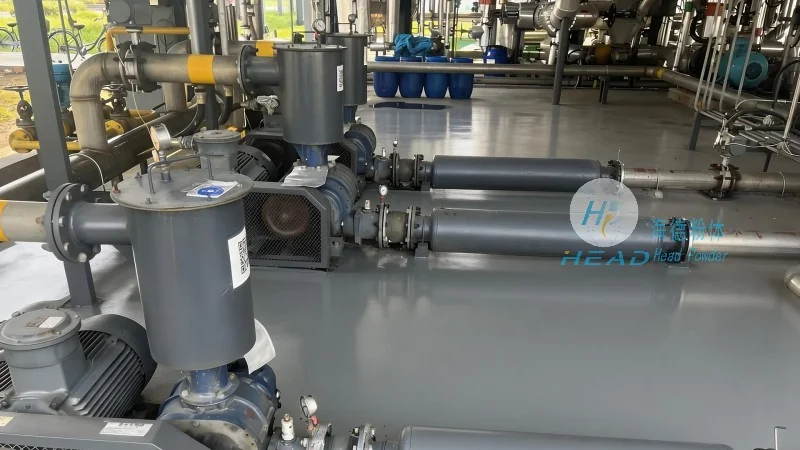
Introduction to Stone Aggregate Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in providing advanced pneumatic conveying solutions for various industrial applications. The company’s expertise lies in developing equipment tailored to handle stone aggregates, ensuring optimal performance and durability. This equipment is essential for transporting bulk materials like gravel, crushed stone, and other aggregates with precision and efficiency.
Working Principle of Stone Aggregate Pneumatic Conveying Equipment
The core mechanism of stone aggregate pneumatic conveying equipment involves the use of air as the medium to transport solid particles. The system typically operates on the principle of creating a pressure differential or using vacuum to move the material through a pipeline. The process begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. As the air is introduced, it creates a flow that carries the aggregates along the pipeline. The equipment uses a combination of positive pressure (pressure conveying) or negative pressure (vacuum conveying) to ensure consistent and controlled movement of the material. The design includes components such as a blower, filter, and control valves to regulate the air flow and material transport. The blower generates the necessary air pressure, while the filter removes dust and particles to maintain air quality and system efficiency. The control valves allow operators to adjust the flow rate and pressure, ensuring the system operates within optimal parameters. The entire process is automated, with sensors monitoring the material level and air pressure to prevent blockages and ensure smooth operation.
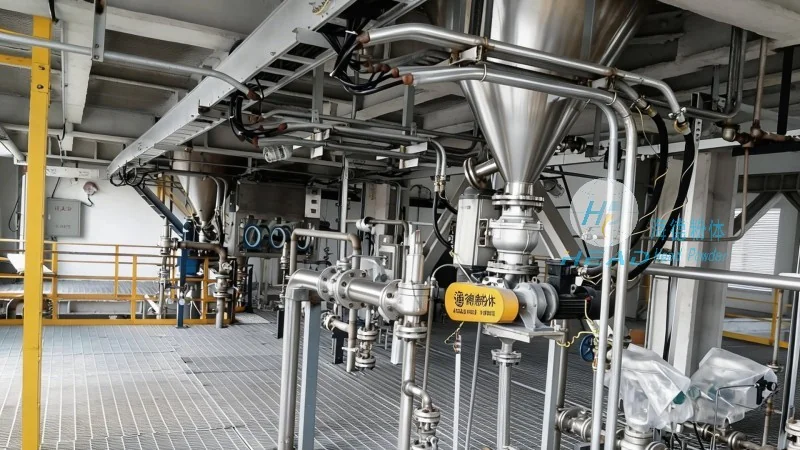
Key Features of Stone Aggregate Pneumatic Conveying Equipment
Stone aggregate pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is characterized by several key features that enhance its performance and usability. Firstly, the equipment is designed for high efficiency, capable of transporting large volumes of stone aggregates over significant distances with minimal energy consumption. The robust construction ensures durability and long service life, even under harsh operating conditions. The system is also equipped with advanced control systems that provide real-time monitoring and adjustment, allowing for precise control over the material flow. Another notable feature is the low maintenance requirement, as the design minimizes moving parts and uses wear-resistant materials to reduce downtime. The equipment is also compatible with various types of stone aggregates, including different sizes and compositions, making it versatile for diverse industrial needs. Additionally, the system is designed to be safe and reliable, with features such as automatic shut-off and overload protection to prevent accidents and equipment damage. The integration of modern technology, such as digital controls and sensors, further enhances the equipment's functionality and ease of operation.
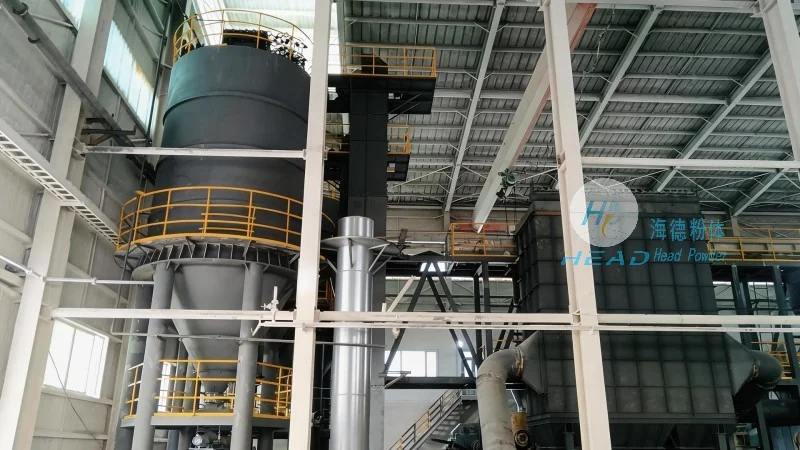
Advantages of Using Stone Aggregate Pneumatic Conveying Equipment
Implementing stone aggregate pneumatic conveying equipment offers numerous advantages for industrial operations. One of the primary benefits is the reduction in labor costs, as the system automates the material handling process, minimizing the need for manual labor. The equipment also improves safety by eliminating the need for manual handling of heavy or dusty materials, reducing the risk of accidents and health issues. Another significant advantage is the improvement in material quality, as the system prevents contamination and degradation during transport. The equipment also enhances operational efficiency by providing consistent and reliable material flow, reducing downtime and increasing productivity. Furthermore, the system is compact and can be integrated into existing facilities, making it a cost-effective solution for upgrading material handling processes. The low maintenance requirements and long service life of the equipment contribute to overall cost savings and operational reliability. The ability to transport materials over long distances without the need for intermediate storage or handling also streamlines the production process, improving overall workflow.
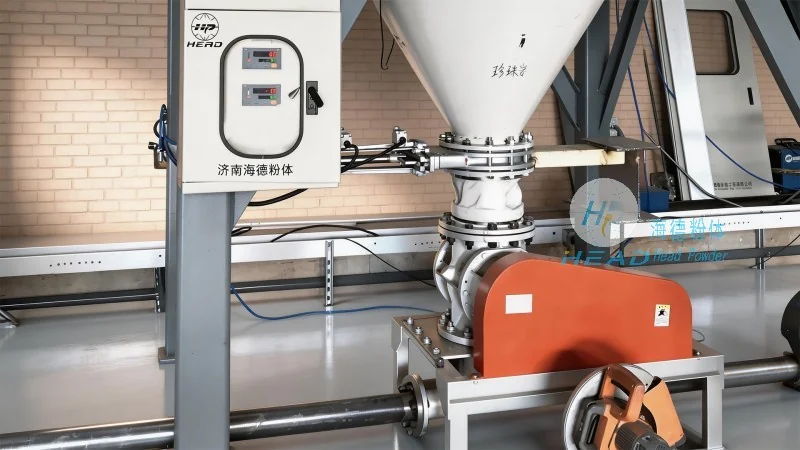
Applications and Industries
The stone aggregate pneumatic conveying equipment is widely used in various industries that require the handling of bulk stone aggregates. These include the construction industry, where it is used for transporting gravel, crushed stone, and other aggregates to construction sites. The equipment is also utilized in the mining industry for transporting crushed ore and other materials from processing plants. Additionally, it is employed in the aggregate production industry for moving raw materials between processing stages. The equipment is also suitable for use in the road construction industry, where it is used to transport aggregates for road surfacing and foundation work. The versatility of the system makes it applicable in various other sectors, including the chemical and food processing industries, where it can be adapted to handle different types of bulk materials.
Conclusion
Stone aggregate pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. represents a reliable and efficient solution for handling bulk stone aggregates. The equipment operates on a well-defined working principle, utilizing air as the transport medium to move materials through pipelines. Its key features, including high efficiency, durability, and advanced control systems, make it an ideal choice for various industrial applications. The advantages of using this equipment, such as reduced labor costs, improved safety, and enhanced operational efficiency, contribute to its widespread adoption in the industry. As industries continue to seek more efficient and sustainable material handling solutions, the stone aggregate pneumatic conveying equipment remains a valuable asset, providing reliable performance and long-term benefits.