

Working Principle and Features of Tonne Bag Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced pneumatic conveying systems. Among their product line is the tonne bag pneumatic conveying equipment, which is widely used in various industrial sectors for efficient bulk material handling. This article provides a detailed overview of the working principle and key features of this equipment, highlighting its operational efficiency and versatility.
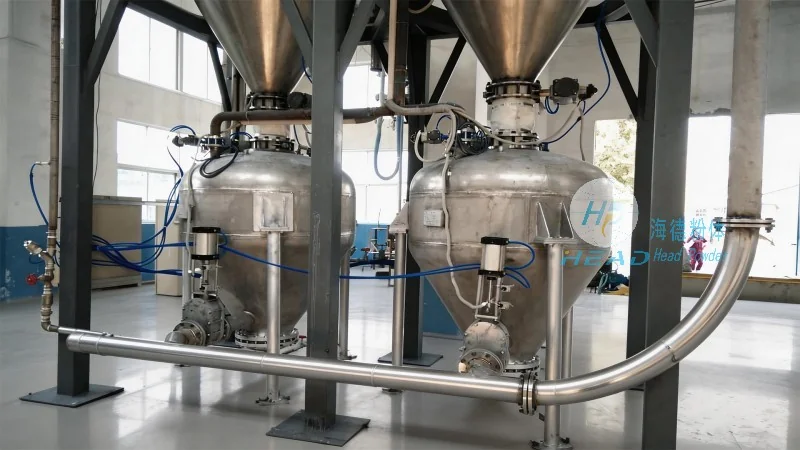
Understanding the Working Principle of Tonne Bag Pneumatic Conveying Equipment
The tonne bag pneumatic conveying equipment operates on the principle of pneumatic transport, where bulk materials are conveyed through a pipeline using compressed air or other gases. The system typically consists of several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The process begins with the material being loaded into the hopper from a tonne bag or other storage containers. The feeder then regulates the material flow into the conveying line, where it is propelled by the air flow generated by a blower or compressor. The air and material mixture travels through the pipeline to the receiver, where the material is separated from the air and collected. The air is then filtered and discharged back into the system or the environment, completing the cycle.
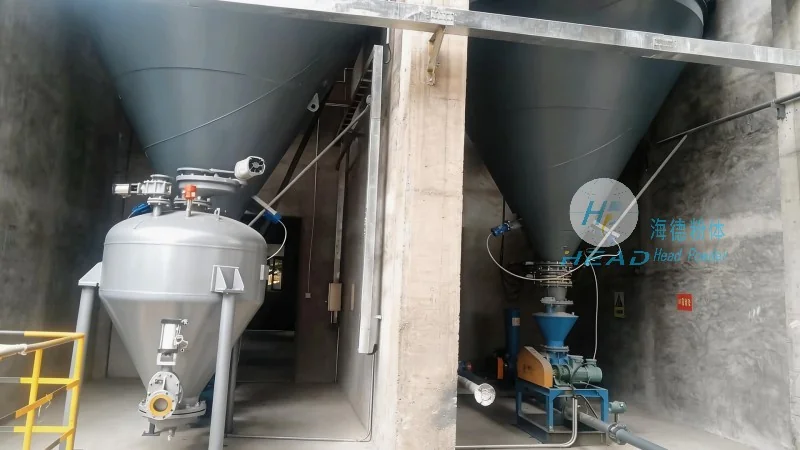
Key Features of Tonne Bag Pneumatic Conveying Equipment
HeadPowder's tonne bag pneumatic conveying equipment is engineered with several notable features that enhance its performance and reliability. One of the primary features is its ability to handle a wide range of bulk materials, including powders, granules, and fine particles, with minimal degradation or segregation. The system is designed to maintain consistent material flow rates, ensuring stable operation even with varying material characteristics. Another significant feature is the integration of advanced control systems that allow for precise regulation of air pressure, flow rate, and material feed, optimizing energy consumption and operational efficiency. The equipment also incorporates robust construction materials, such as stainless steel or corrosion-resistant alloys, to withstand harsh industrial environments and ensure long-term durability. Additionally, the system is equipped with safety features, including pressure relief valves and overcurrent protection, to prevent accidents and ensure safe operation. The modular design of the equipment allows for easy installation, maintenance, and expansion, making it suitable for both new and existing industrial applications.
Applications and Benefits in Industrial Settings
The tonne bag pneumatic conveying equipment from HeadPowder is widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining. In these sectors, the equipment is utilized for the transport of raw materials, intermediate products, and finished goods between different processing stages. The benefits of using this equipment include improved operational efficiency, reduced labor costs, and enhanced product quality due to minimized material handling errors and contamination. The system also offers flexibility in terms of layout and integration with existing production lines, allowing for seamless incorporation into existing workflows. Furthermore, the equipment contributes to better workplace safety by eliminating the need for manual handling of bulk materials, reducing the risk of accidents and exposure to hazardous substances. The consistent and controlled material flow provided by the system also helps in maintaining process stability and reducing downtime, leading to increased overall productivity.
Conclusion
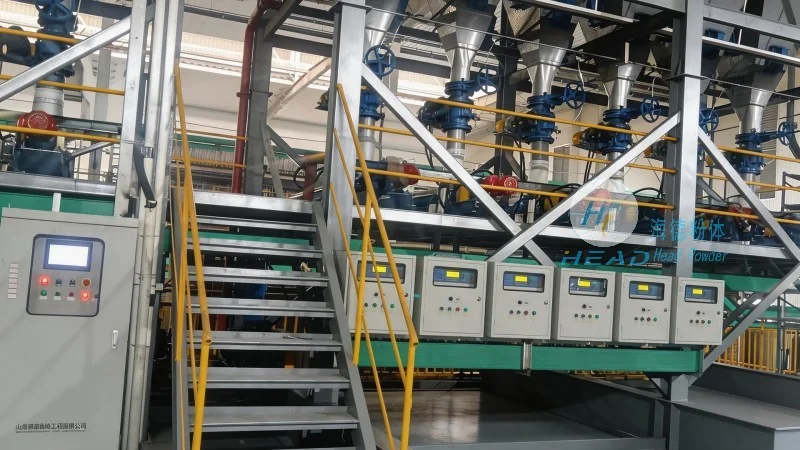
HeadPowder's tonne bag pneumatic conveying equipment represents a reliable and efficient solution for bulk material handling in industrial applications. By understanding its working principle and leveraging its key features, businesses can enhance their operational performance, improve product quality, and ensure safe and sustainable material transport. With its robust construction, advanced control systems, and versatile design, this equipment is well-suited for a wide range of industrial needs, making it a valuable asset for companies seeking to optimize their material handling processes.