With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Sodium bicarbonate, commonly known as baking soda, is a widely used chemical compound in various industrial and commercial applications. When it comes to handling this powder in bulk, efficient and reliable systems are essential to ensure smooth operations and maintain product quality. This article explores the concept of sodium bicarbonate powder handling and delves into the fundamental design principles that underpin effective powder transport solutions, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd. in designing such systems.
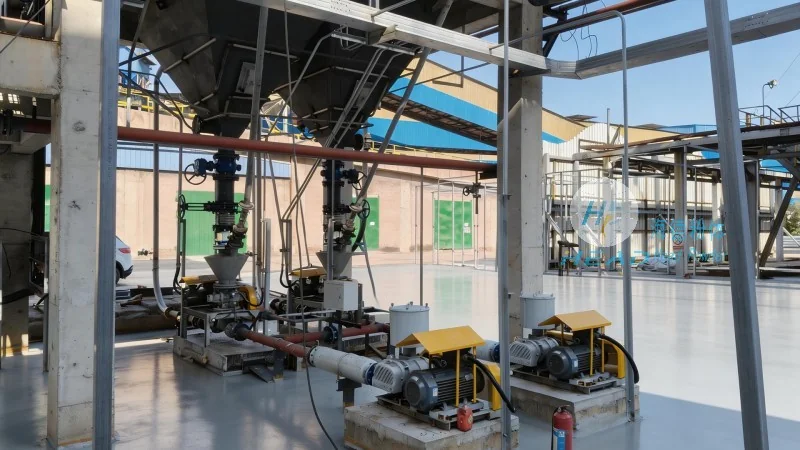
Handling sodium bicarbonate powder involves addressing several key challenges. The material’s properties, such as its fine particle size and hygroscopic nature, can affect how it behaves during transport. Additionally, ensuring consistent flow, preventing caking or agglomeration, and maintaining a clean and safe environment are critical considerations. These challenges necessitate specialized equipment and engineering solutions tailored to the unique characteristics of sodium bicarbonate. The company, Shandong HeadPowder Engineering Co., Ltd., recognizes these challenges and develops systems that mitigate them through careful design and material selection.
Effective sodium bicarbonate powder handling systems are built on several core design principles. First, the system must ensure proper material flow by addressing issues like static electricity and particle segregation. This often involves the use of appropriate feeders, such as rotary valves or screw conveyors, which can maintain a consistent flow rate and prevent blockages. Second, the design must incorporate dust control measures to protect both the material and the environment. This includes features like enclosed systems, dust collection hoods, and filtration units to minimize airborne particles. Third, the system should prioritize safety and compliance with industrial standards, ensuring that all components are designed to handle the material’s potential hazards, such as dust explosions or inhalation risks. Finally, the design should allow for easy maintenance and cleaning to prevent contamination and ensure long-term operational reliability. Shandong HeadPowder Engineering Co., Ltd. emphasizes these principles in their designs, ensuring that each system is tailored to the specific needs of the client.
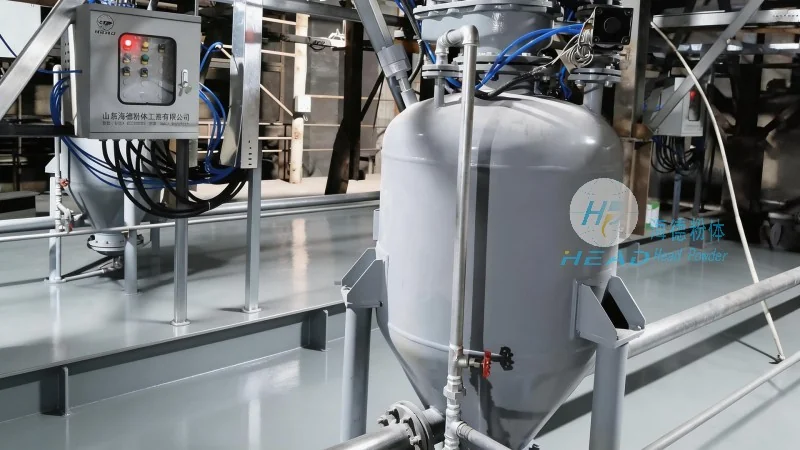
A typical sodium bicarbonate powder handling system consists of several interconnected components. At the core is the storage silo or hopper, which holds the bulk material. From there, a feeder, such as a rotary airlock or a screw feeder, regulates the flow of powder into the transport line. The transport line itself may include pipelines, pneumatic conveying systems, or mechanical conveyors, depending on the distance and layout of the facility. The system also includes control valves, which manage the flow direction and speed, and may incorporate sensors to monitor levels and flow rates. Additionally, the system is equipped with dust collection and filtration equipment to capture any particles that escape during transport, ensuring a clean and safe working environment. Each component is carefully selected and integrated to work in harmony, optimizing the overall performance of the powder handling process. The company ensures that all components are durable and suitable for the hygroscopic and fine-particle nature of sodium bicarbonate.
The physical and chemical properties of sodium bicarbonate play a significant role in the design of powder handling systems. For instance, the material’s hygroscopic nature means it can absorb moisture from the air, leading to caking or clumping. To address this, the system may include drying or dehumidification units to maintain the material’s dryness. Similarly, the fine particle size can cause issues with flow and segregation, requiring specialized equipment like vibratory feeders or air classifiers to ensure uniform distribution. Engineers must consider these properties when selecting materials for components, such as the use of corrosion-resistant materials for parts that come into contact with the powder, and designing the system to minimize friction and wear. By understanding and accounting for these properties, the design can effectively mitigate common problems associated with sodium bicarbonate powder handling. Shandong HeadPowder Engineering Co., Ltd. leverages this understanding to create systems that are both efficient and durable.
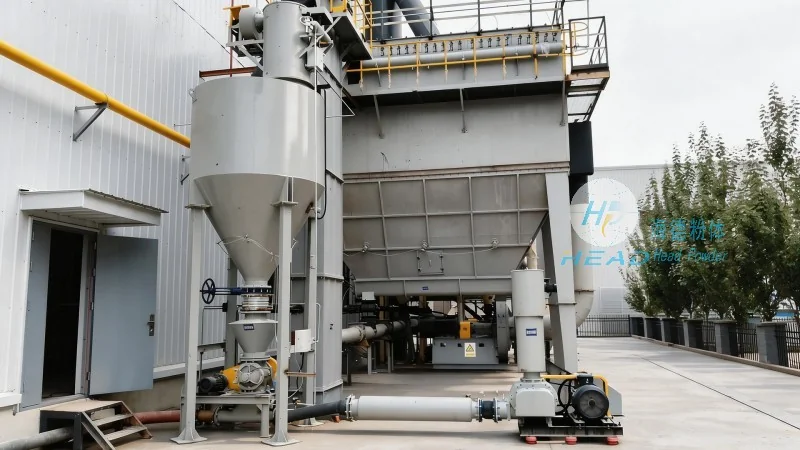
Sodium bicarbonate powder handling systems are utilized across a wide range of industries where the compound is used in bulk. In the food and beverage industry, these systems are essential for processing baking soda into various products, such as baking powders and leavening agents. In the pharmaceutical sector, the systems ensure the safe and consistent handling of sodium bicarbonate for use in medications and supplements. The chemical industry also relies on these systems for manufacturing and processing, where the material is used as a raw ingredient in various chemical reactions. Additionally, in the agricultural and water treatment industries, sodium bicarbonate is used for soil amendment and pH adjustment, requiring reliable powder handling systems to distribute the material effectively. Each application demands a tailored approach to powder handling, but the underlying design principles remain consistent, focusing on efficiency, safety, and product integrity. Shandong HeadPowder Engineering Co., Ltd. serves these industries with customized solutions that meet their specific requirements.
In conclusion, the design of sodium bicarbonate powder handling systems is a critical aspect of industrial operations. By adhering to fundamental principles such as proper flow control, dust management, and safety compliance, companies can ensure the efficient and safe handling of this essential material. The components and considerations discussed in this article highlight the complexity and importance of these systems, which are vital to maintaining productivity and product quality. As industries continue to rely on sodium bicarbonate in bulk, the continued development and refinement of powder handling technologies will remain essential to meet the evolving demands of the market. Shandong HeadPowder Engineering Co., Ltd. remains committed to providing innovative and reliable solutions for sodium bicarbonate powder handling, ensuring that clients can operate with confidence and efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top