With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Efficient material handling is a critical challenge in industrial processes, especially when dealing with fine powders and granular materials like those produced from dry flue gas desulfurization (FGD) systems. The traditional methods of transporting such materials often involve complex and costly equipment, leading to operational inefficiencies and increased maintenance costs. This article explores the innovative approach of pneumatic conveying for FGD ash, highlighting how air flow can be harnessed to achieve high-efficiency, low-cost material transport. We will delve into the technical aspects, benefits, and practical applications of this method, providing a comprehensive overview for industry professionals seeking to optimize their material handling operations.
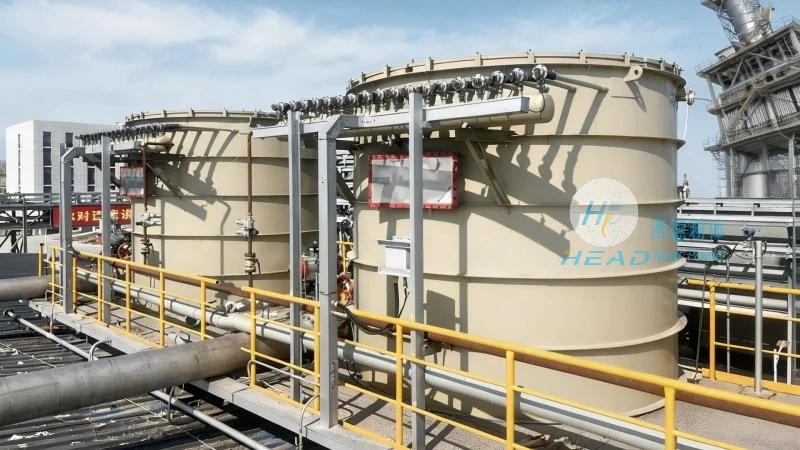
Dry flue gas desulfurization is a widely adopted technique in power plants and industrial facilities to reduce sulfur dioxide emissions. The process involves the use of limestone or other sorbents to capture sulfur compounds from flue gases, resulting in the production of a fine, dry ash byproduct. This ash, often referred to as FGD ash, is typically composed of calcium sulfite/sulfate and other minerals, with particle sizes ranging from sub-micron to several microns. The characteristics of this material—such as its high moisture content (when wet), abrasive nature, and tendency to agglomerate—make it challenging to transport using conventional methods like belt conveyors or screw conveyors. These traditional systems often suffer from blockages, increased wear and tear, and higher energy consumption, making them less suitable for large-scale applications.
Pneumatic conveying, also known as air-based transport, is a method that uses compressed air or other gases to move bulk materials through a pipeline system. Unlike mechanical conveyors, which rely on physical contact and moving parts, pneumatic systems utilize the kinetic energy of the air stream to carry particles. This technology is particularly effective for handling fine powders and granular materials, as it can transport materials over long distances with minimal degradation and low maintenance requirements. The primary advantage of pneumatic conveying lies in its ability to handle materials that are difficult to transport mechanically, such as FGD ash, by leveraging the properties of air flow to achieve efficient and reliable transport.
A typical pneumatic conveying system consists of several key components, each playing a crucial role in the material transport process. The main components include a blower or compressor to generate the air flow, a hopper or feeder to introduce the material into the system, a pipeline network to transport the material, and a receiver or silo to collect the material at the destination. The working principle involves the material being fed into the system, where it is mixed with the air stream. The air flow then carries the particles through the pipeline, maintaining a consistent velocity to prevent settling or blockages. The system can operate in either positive pressure (where the air is forced through the pipeline) or negative pressure (where the air is drawn through the pipeline), depending on the application and material characteristics. For FGD ash, positive pressure systems are often preferred due to their ability to handle abrasive materials and prevent dust emissions.
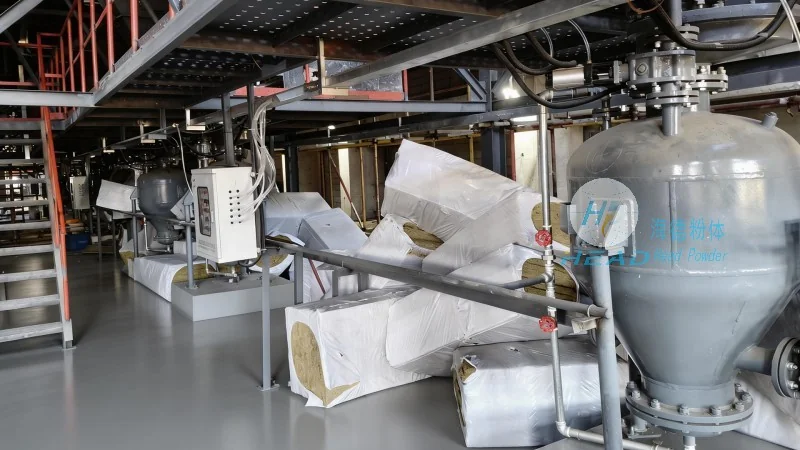
When compared to traditional mechanical conveyors, pneumatic conveying offers several significant advantages for transporting FGD ash. First, it provides a dust-free and enclosed transport environment, which is crucial for maintaining air quality and preventing contamination. The enclosed system also reduces the risk of material loss and environmental pollution, making it more environmentally friendly. Second, pneumatic systems are highly flexible and can be easily integrated into existing industrial facilities, allowing for the transport of materials over long distances without the need for extensive infrastructure modifications. Third, the energy efficiency of pneumatic conveying is superior to mechanical systems, as it minimizes friction and wear, resulting in lower operational costs over time. Additionally, the system can handle varying material flow rates and particle sizes, making it adaptable to different production requirements. These advantages make pneumatic conveying an ideal solution for FGD ash transport, especially in large-scale power plants and industrial facilities.
Pneumatic conveying for FGD ash has been successfully implemented in various industrial applications, demonstrating its effectiveness and reliability. For example, in a large thermal power plant in China, the company Shandong HeadPowder Engineering Co., Ltd. (headpowder) installed a pneumatic conveying system to transport FGD ash from the desulfurization unit to a storage silo. The system was designed to handle a flow rate of 10 tons per hour, with a pipeline length of 500 meters. The implementation resulted in a significant reduction in material handling costs, as the traditional belt conveyor system was replaced with a more efficient and low-maintenance pneumatic system. The plant also reported improved air quality and reduced dust emissions, contributing to a more sustainable operation. Another case study involved a chemical plant that used pneumatic conveying to transport FGD ash to a recycling facility, where the ash was used as a raw material for cement production. The system proved to be highly effective in maintaining consistent material flow and minimizing downtime, leading to increased production efficiency.
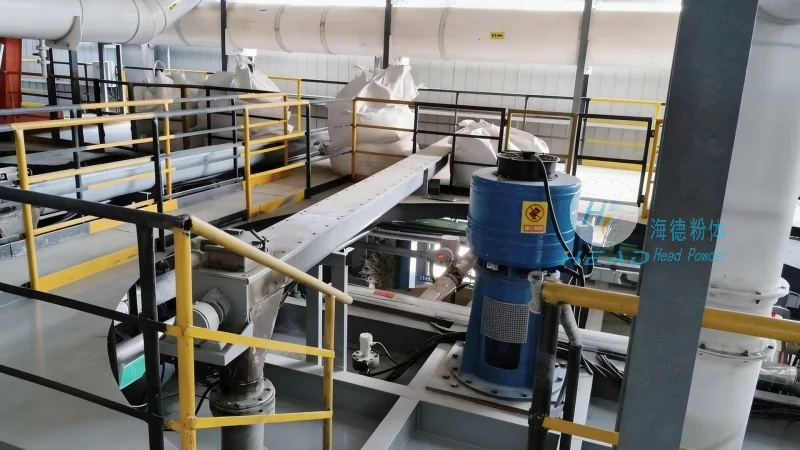
Designing an effective pneumatic conveying system for FGD ash requires careful consideration of several factors to ensure optimal performance and longevity. First, the material characteristics, such as particle size distribution, moisture content, and abrasiveness, must be thoroughly analyzed to determine the appropriate system configuration. For example, fine particles may require higher air velocities to prevent settling, while abrasive materials may necessitate the use of wear-resistant materials for the pipeline and components. Second, the system layout and pipeline design are critical, as the configuration directly impacts the efficiency and reliability of the transport process. Properly sized pipelines, appropriate bends and fittings, and adequate air flow rates are essential to maintain consistent material transport. Third, the selection of the blower or compressor is crucial, as it must provide sufficient air pressure and volume to handle the material flow rate and overcome pipeline resistance. Additionally, regular maintenance and monitoring of the system are necessary to ensure optimal performance and prevent issues such as blockages or air leaks. Best practices include regular cleaning of the pipeline, inspection of components for wear and tear, and monitoring of air flow and pressure to detect any potential problems early. By following these design considerations and best practices, industrial facilities can achieve efficient and reliable pneumatic conveying of FGD ash, maximizing operational efficiency and minimizing costs.
As industrial processes continue to evolve, the demand for more efficient and sustainable material handling solutions is increasing. Pneumatic conveying technology is also advancing, with several innovations aimed at improving performance and reducing costs. One of the key trends is the development of high-capacity and low-energy pneumatic systems, which use advanced blower technologies and optimized pipeline designs to achieve higher material flow rates with lower energy consumption. Another trend is the integration of automation and control systems, which allow for real-time monitoring and adjustment of the system parameters, ensuring optimal performance under varying conditions. Additionally, the use of smart materials and sensors is being explored to enhance the reliability and safety of pneumatic conveying systems. For example, sensors can be used to detect blockages or air leaks, triggering automatic shutdown or maintenance alerts. These innovations are expected to further improve the efficiency and sustainability of pneumatic conveying for FGD ash transport, making it an even more attractive solution for industrial facilities.
In conclusion, pneumatic conveying is a highly effective and efficient method for transporting FGD ash and other fine powders and granular materials. By leveraging the properties of air flow, this technology offers significant advantages over traditional mechanical conveyors, including reduced costs, improved air quality, and increased operational flexibility. The successful implementation of pneumatic conveying systems, as demonstrated by case studies from companies like Shandong HeadPowder Engineering Co., Ltd., highlights the practical benefits of this approach. As industrial facilities continue to seek sustainable and cost-effective solutions for material handling, pneumatic conveying is likely to play an increasingly important role in optimizing FGD ash transport and other bulk material applications. With ongoing innovations and advancements in the technology, the future of pneumatic conveying looks promising, offering even more efficient and reliable solutions for industrial material handling needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top