With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and manufacturing of advanced powder handling solutions. This article provides an overview of the sorghum distillers' grain powder conveying system, detailing its structural components and operational principles to help industry professionals understand its functionality and benefits.
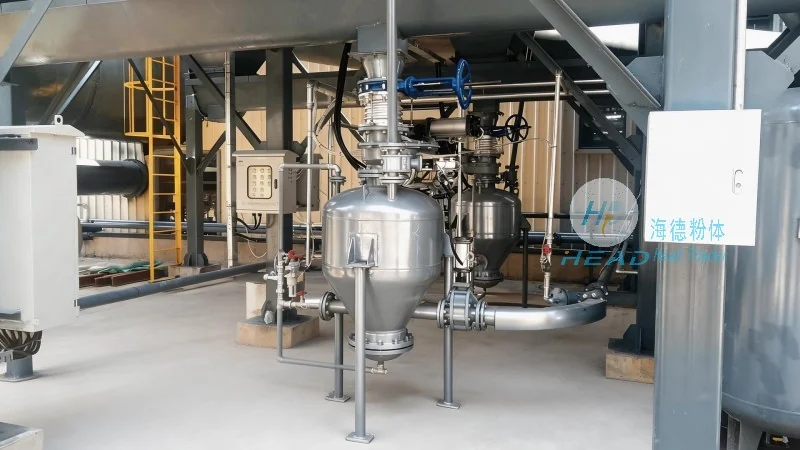
The sorghum distillers' grain powder conveying system is engineered to efficiently transport and manage the byproduct of sorghum-based alcohol production. As a key component in the distillery process, this system ensures the safe and reliable movement of distillers' grain, which is rich in nutrients and often repurposed for animal feed or other industrial applications. The system's design addresses the unique challenges of handling fine, dry powders, such as dust control, material flow optimization, and system durability.
The sorghum distillers' grain powder conveying system comprises several critical components that work in tandem to achieve efficient material transport. These include:
1. Feeding Hopper: The system begins with a feeding hopper, which stores and regulates the flow of sorghum distillers' grain. This component is designed with a sloped bottom to facilitate smooth material discharge and is equipped with a level indicator to monitor the grain inventory. The hopper is typically constructed from high-strength materials, such as stainless steel, to resist corrosion and wear from the abrasive nature of the grain.
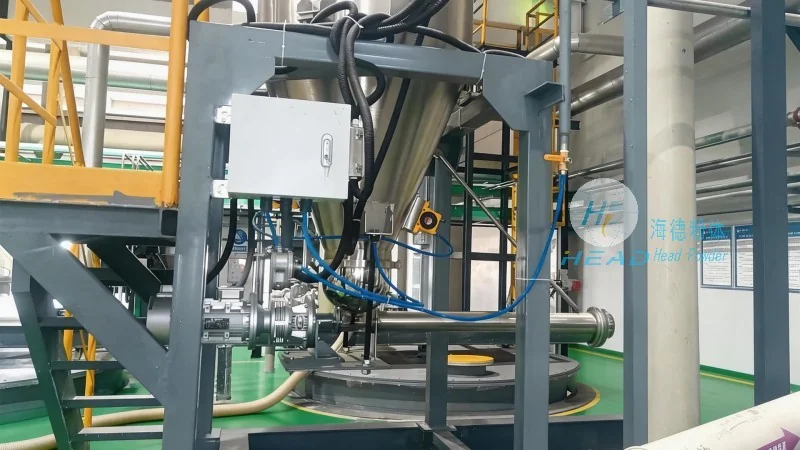
2. Pneumatic Conveying Line: The core of the system is the pneumatic conveying line, which uses air pressure to transport the powder. This technology is ideal for fine powders like distillers' grain, as it minimizes material degradation and reduces the risk of dust accumulation. The line includes a series of pipes, elbows, and straight sections, all designed to maintain consistent air flow and prevent blockages. The system may incorporate a positive displacement blower or a rotary airlock to generate the necessary air pressure for conveying.
3. Control Panel: A centralized control panel manages the operation of the conveying system. It includes sensors for monitoring pressure, flow rate, and material level, as well as control valves and switches to adjust the air pressure and feeding rate. The control panel ensures that the system operates within safe parameters and can be adjusted to accommodate varying production volumes.
4. Dust Collection System: To comply with environmental regulations and maintain a safe working environment, the system is equipped with a dust collection system. This component captures any airborne particles during the conveying process and filters them before releasing clean air back into the environment. The dust collection system typically includes a cyclone separator and a fabric filter to ensure efficient particle removal.
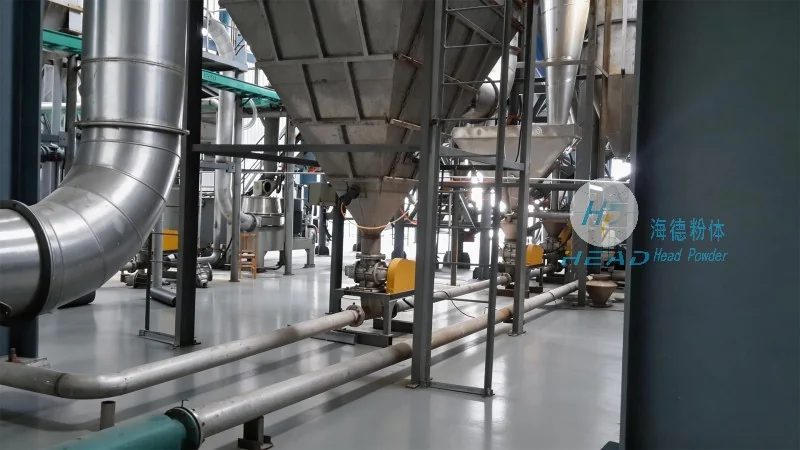
The operation of the sorghum distillers' grain powder conveying system follows a systematic process that ensures efficient material transport. The sequence begins with the loading of sorghum distillers' grain into the feeding hopper. The hopper's design allows for a controlled discharge of the material into the pneumatic conveying line.
As the material enters the line, the positive displacement blower generates high-pressure air, which propels the powder through the pipes. The air flow is directed through a series of bends and straight sections, maintaining a consistent velocity to prevent material settling or blockages. The system's control panel monitors the pressure and flow rate, adjusting the air pressure as needed to maintain optimal transport conditions.
Upon reaching the destination, the material is discharged into a receiving hopper or storage silo. The system may include a rotary airlock at the discharge end to prevent backflow and maintain a consistent flow rate. The air used in the conveying process is then filtered by the dust collection system, ensuring that no dust is released into the environment.
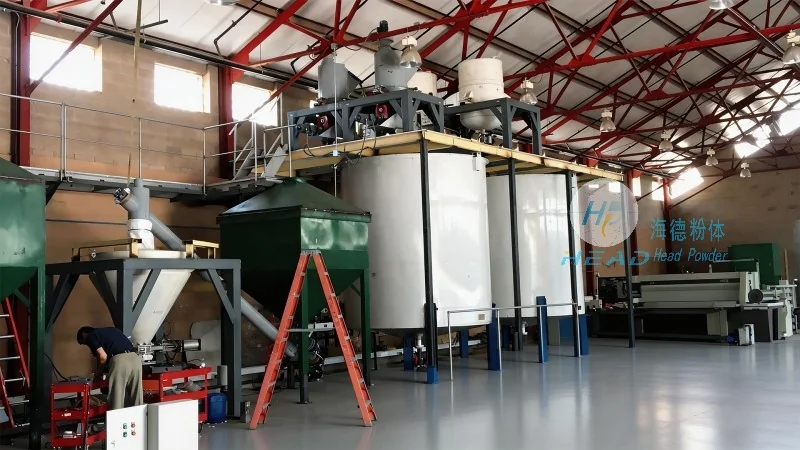
The sorghum distillers' grain powder conveying system offers several advantages for distilleries and other industrial facilities. Its pneumatic design minimizes the risk of material contamination and reduces the need for manual handling, improving workplace safety. The system's ability to handle fine powders efficiently reduces material loss and improves overall production efficiency. Additionally, the dust collection system ensures compliance with environmental regulations, protecting both the environment and the workforce.
Applications of this system include the transport of distillers' grain from the distillation unit to storage facilities, or from storage to feed mills for animal feed production. The system's flexibility allows it to be integrated into existing distillery processes, enhancing overall operational efficiency and reducing downtime.
The sorghum distillers' grain powder conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution for the efficient handling of sorghum distillers' grain. By combining advanced structural components and operational principles, the system ensures reliable material transport while maintaining safety and environmental compliance. As a key player in the engineering industry, HeadPowder continues to innovate in powder handling technologies, providing tailored solutions for the needs of the distillery and related industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top