

Operation Process and Working Principle of Material Mixing and Air-Driven Conveying Systems for Ingr
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced material handling systems. One of their core products is the material mixing and air-driven conveying system, which is widely used in industries such as food, pharmaceuticals, and chemical processing to efficiently blend and transport ingredients. This article provides a detailed overview of the operation process and working principle of these systems, highlighting their efficiency, reliability, and versatility.
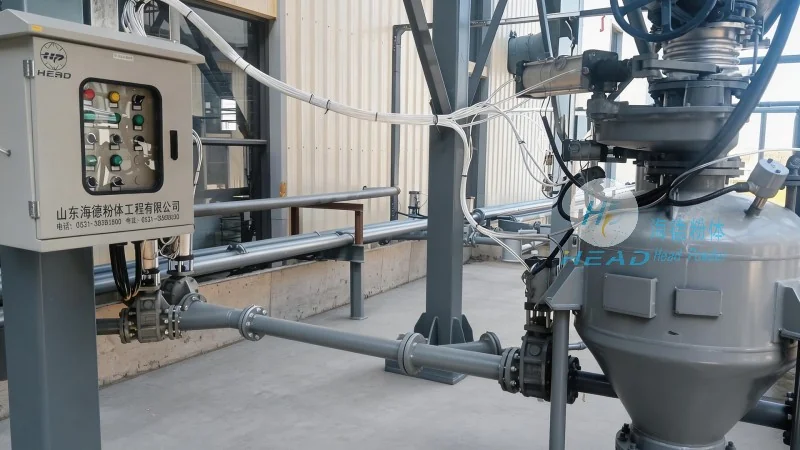
System Overview and Key Components
The material mixing and air-driven conveying system is a sophisticated piece of equipment engineered to handle various types of bulk materials, including powders, granules, and fine particles. The system typically consists of several key components that work in tandem to achieve optimal performance. These components include a hopper for material storage, a mixing chamber where ingredients are combined, and an air-driven conveyor that transports the blended material to the next processing stage. The system is designed to ensure uniform mixing and consistent material flow, which is crucial for maintaining product quality and meeting strict industry standards.
Operation Process: Step-by-Step Execution
The operation of the material mixing and air-driven conveying system follows a systematic process that ensures precise control over the blending and conveying of ingredients. The process begins with the loading of raw materials into the hopper. The system then activates the mixing mechanism, which may involve rotating blades or agitators that thoroughly combine the different ingredients. Once the mixing is complete, the air-driven conveyor is engaged. This component uses compressed air to create a pressure differential that pulls the blended material through the conveyor lines, ensuring a smooth and continuous flow. The system may also include sensors and control panels that monitor the mixing and conveying process, allowing operators to adjust parameters in real-time to maintain optimal performance.
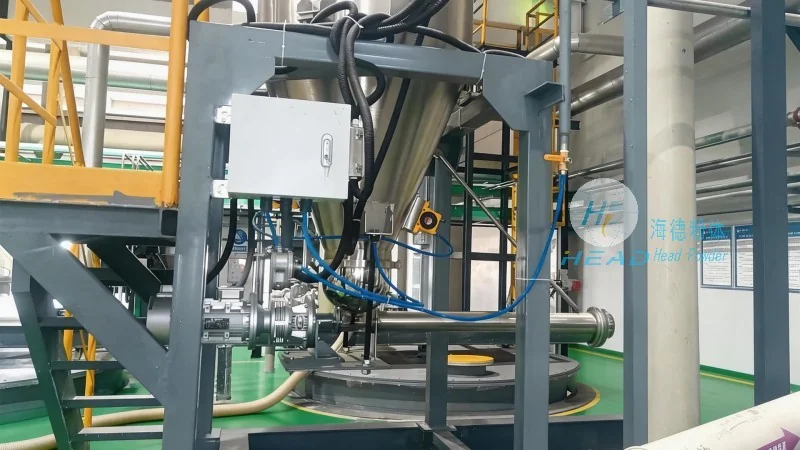
Working Principle: How It Transforms Material Handling
The working principle of the material mixing and air-driven conveying system is based on the principles of fluid dynamics and mechanical mixing. The air-driven conveyor operates by using compressed air to generate a flow of air and material particles, which is known as pneumatic conveying. This method allows for the efficient transport of materials over long distances without the need for mechanical components like belts or chains, reducing maintenance and increasing reliability. The mixing process, on the other hand, relies on mechanical agitation to break down agglomerates and ensure a homogeneous blend. The combination of these two processes—efficient mixing and pneumatic conveying—makes the system highly effective for applications where both uniformity and material transport are critical.
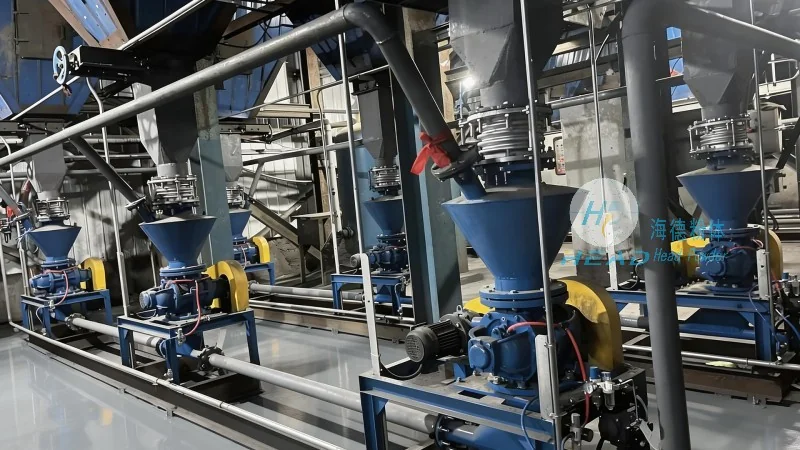
Advantages and Applications in Industrial Settings
The material mixing and air-driven conveying system offers several advantages that make it a preferred choice in various industrial applications. One of the key benefits is its ability to handle a wide range of materials, from fine powders to larger granules, without causing segregation or degradation. The system also provides excellent control over the blending ratio, ensuring that each batch meets the required specifications. Additionally, the air-driven conveyor reduces the risk of contamination, which is essential in industries such as food and pharmaceuticals. These systems are commonly used in the production of food products, where ingredients like flour, sugar, and spices are blended to create consistent flavors and textures. In the pharmaceutical industry, the system is used to mix active ingredients with excipients, ensuring uniform dosage and quality. The chemical industry also benefits from this technology, as it allows for the safe and efficient handling of reactive materials.
Conclusion: Enhancing Productivity and Quality
HeadPowder's material mixing and air-driven conveying systems represent a significant advancement in bulk material handling technology. By combining efficient mixing mechanisms with pneumatic conveying, these systems provide industries with a reliable and versatile solution for ingredient blending and transport. The company's commitment to quality and innovation ensures that their systems meet the highest standards, delivering consistent performance and enhancing overall productivity. For businesses looking to improve their material handling processes, the material mixing and air-driven conveying system from HeadPowder is an excellent choice that combines functionality with durability.