With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Bin pump pneumatic conveying systems represent a sophisticated and efficient method for transporting bulk materials over long distances or within complex industrial settings. These systems are widely utilized across various industries, including mining, food processing, and chemical manufacturing, due to their ability to handle a wide range of materials with minimal maintenance and high operational reliability.
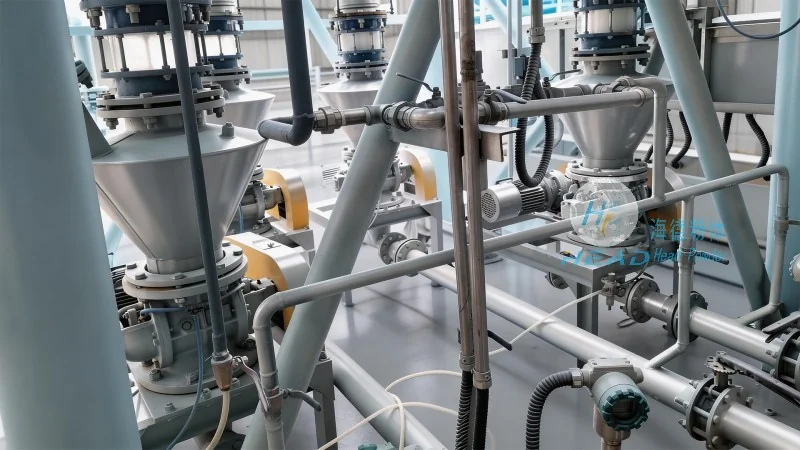
The core of a bin pump system lies in its ability to create a pressure differential that propels material through a pipeline. The system typically consists of a hopper or storage bin, a bin pump unit, and a series of pipes. When material is introduced into the hopper, it is drawn into the pump chamber by a vacuum or pressure created by the pump. The pump then compresses the material, forcing it through the pipeline to the discharge point. This process is often referred to as "pneumatic conveying," as it relies on air or gas to transport the material.
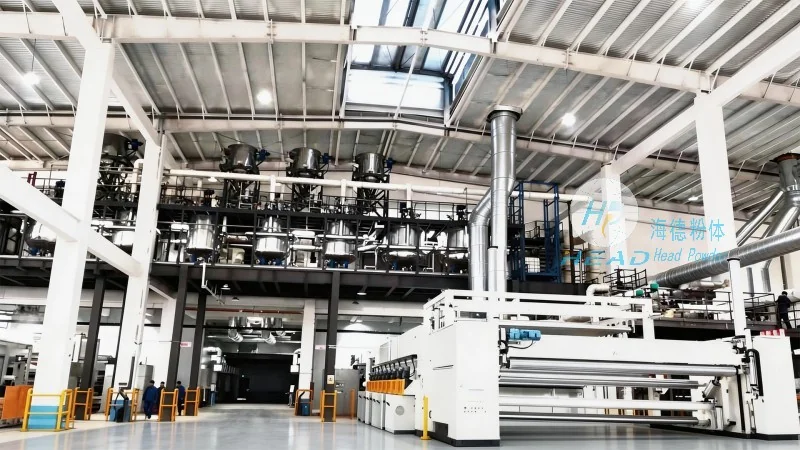
The operation of a bin pump system involves several critical steps and components. First, the material is fed into the storage bin or hopper. The bin pump, which acts as the heart of the system, then draws the material into its chamber. The pump uses either a rotary lobe or a positive displacement mechanism to compress the material, which is then expelled through the discharge line. The system also includes a control panel that monitors pressure, flow rate, and other parameters to ensure optimal performance. Additionally, the pipeline network is designed to handle the specific characteristics of the material being conveyed, such as particle size and moisture content.
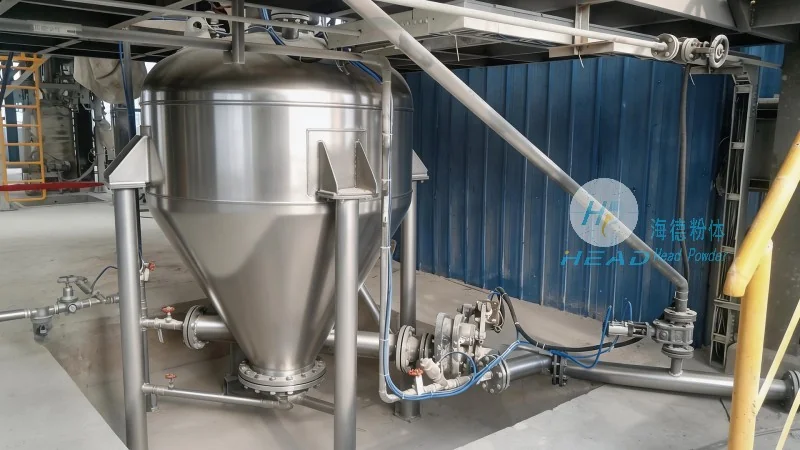
Headpowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in the design, development, and installation of bin pump pneumatic conveying systems. With operations based in Shandong, China, the company has built a strong reputation for delivering high-quality, reliable equipment tailored to the unique needs of its clients. Headpowder's team of engineers and technicians brings extensive experience in material handling and process optimization, ensuring that each system is customized to meet specific operational requirements and industry standards.
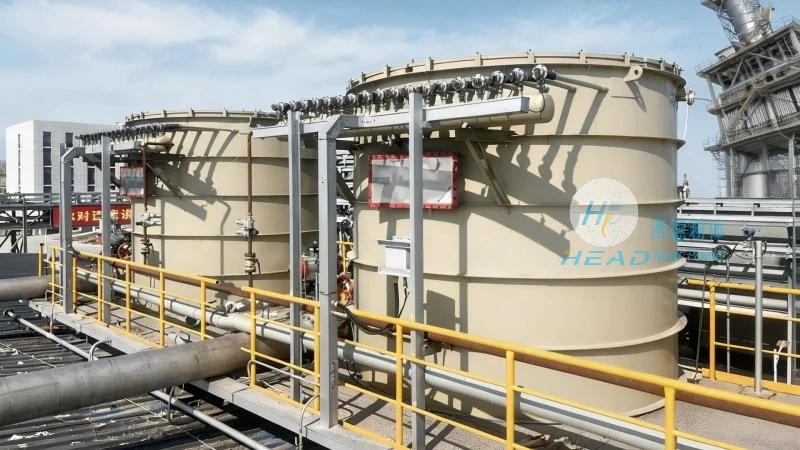
Bin pump systems offer several technical advantages over traditional conveying methods. They provide a dust-free and enclosed environment, which is crucial for materials that are hazardous or require contamination control. The systems are also highly flexible, allowing for changes in material type or flow rate without significant modifications. Furthermore, they can handle materials with varying properties, including abrasive or corrosive substances, making them suitable for a wide range of applications. Common applications include the transport of powders, granules, and bulk solids in industries such as pharmaceuticals, food processing, and chemical manufacturing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top