With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Multi-functional material handling systems represent a sophisticated integration of technology and engineering designed to optimize the movement, storage, and management of various materials in industrial and commercial environments. These systems are engineered to enhance operational efficiency, reduce labor costs, and improve overall productivity by automating the material flow processes. The core principle behind such systems lies in the systematic design of components like conveyors, sorters, and storage units that work in tandem to handle diverse materials with precision and reliability.
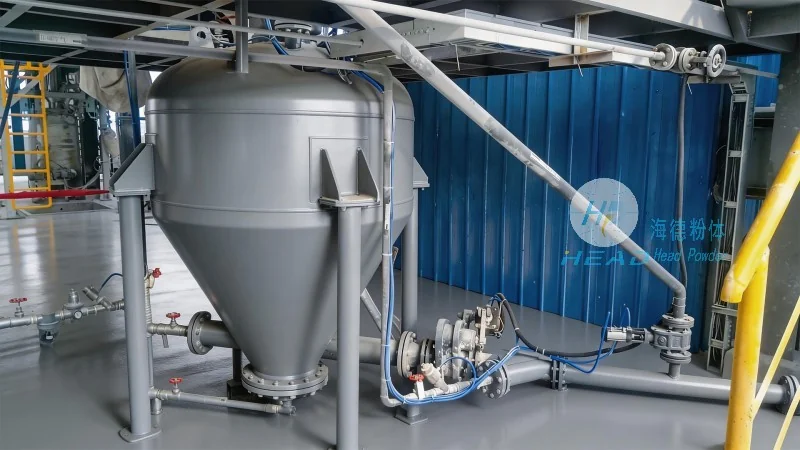
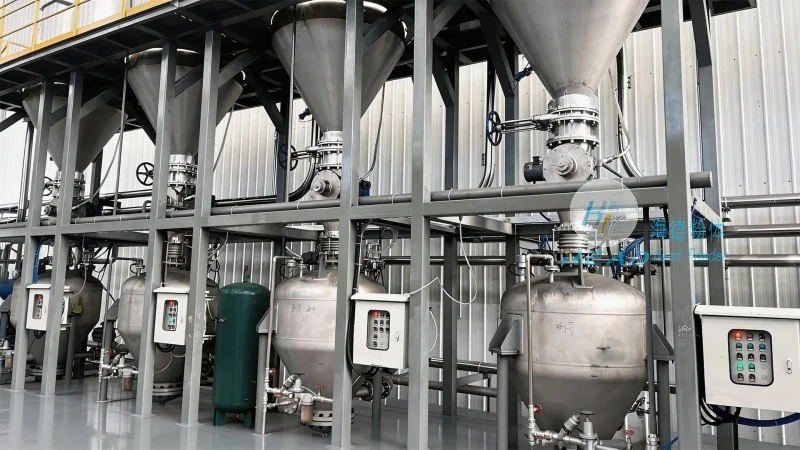
At the heart of a multi-functional material handling system is a modular design approach that allows for flexibility and adaptability to different operational needs. The system typically operates on the principle of continuous or intermittent material flow, depending on the application requirements. Key components include belt conveyors, roller conveyors, and automated storage and retrieval systems (AS/RS), each tailored to specific material characteristics such as weight, size, and shape. The integration of sensors, control systems, and software enables real-time monitoring and adjustment of the material handling process, ensuring optimal performance and minimal downtime. Additionally, the systems are designed with safety features to protect both personnel and equipment, adhering to industry standards and regulations.
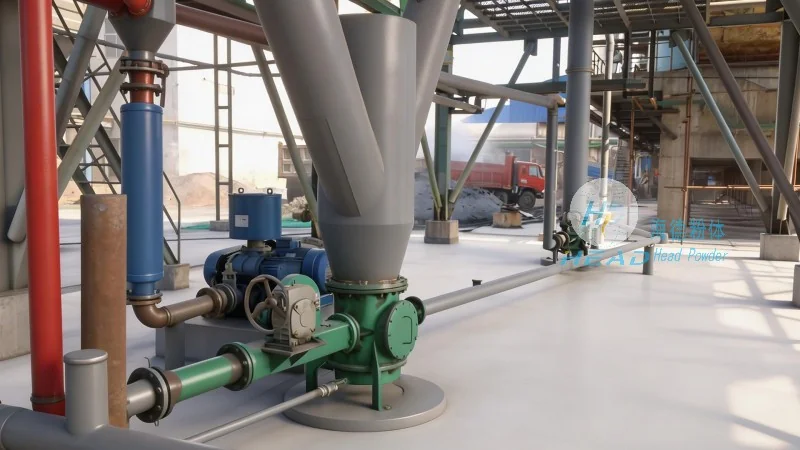
Multi-functional material handling systems are widely employed across various industries, including manufacturing, logistics, warehousing, and distribution centers. In manufacturing settings, these systems facilitate the smooth transfer of raw materials to production lines and the movement of finished products to storage or shipping areas. The ability to handle different material types, from lightweight components to heavy machinery parts, makes them versatile for diverse production processes. In logistics and warehousing, the systems enhance order picking, sorting, and inventory management, improving order fulfillment rates and reducing handling errors. The working scene characteristics also include high throughput capabilities, as these systems are built to handle large volumes of materials efficiently. Furthermore, the adaptability of the systems allows for integration with existing infrastructure, minimizing the need for extensive facility modifications.
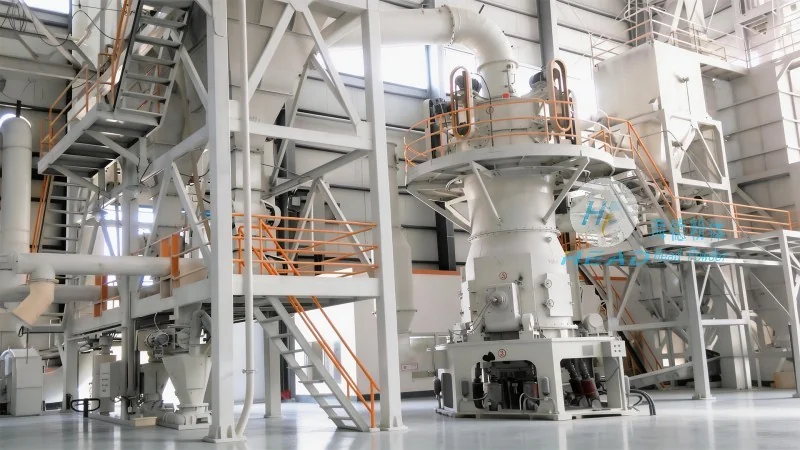
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of advanced material handling solutions. With a strong commitment to innovation and quality, the company specializes in designing, manufacturing, and implementing multi-functional material handling systems tailored to the unique needs of its clients. HeadPowder's expertise lies in understanding the specific challenges faced by industries and developing customized solutions that enhance operational efficiency and reduce costs. The company's facilities are located in Shandong, China, where it leverages local resources and expertise to deliver high-quality products and services. By focusing on customer satisfaction and technological advancement, headpowder has established itself as a trusted partner in the material handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top