With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for various industrial applications. Among their portfolio is the coal ash particle material pneumatic conveying equipment, a sophisticated solution engineered to efficiently handle and transport coal ash particles with precision and reliability.
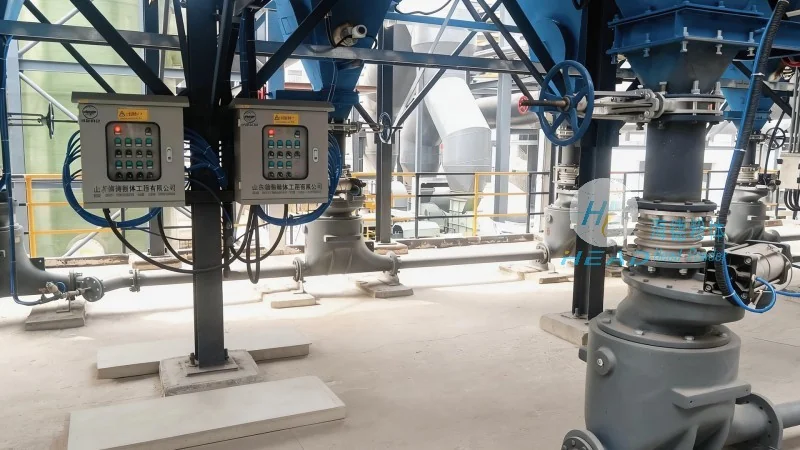
Coal ash, a byproduct of coal combustion in power plants, poses unique challenges in material handling due to its fine particle size, abrasive nature, and potential for dust generation. Traditional conveying methods such as belt conveyors or screw conveyors may struggle with these characteristics, leading to operational inefficiencies and maintenance issues. The coal ash particle material pneumatic conveying equipment from HeadPowder addresses these challenges by leveraging pneumatic technology to provide a seamless, dust-free, and energy-efficient solution for transporting coal ash from source to destination.
The core of the coal ash particle material pneumatic conveying equipment is its pneumatic conveying mechanism, which operates on the principle of air flow to move solid particles. The system typically consists of a hopper for material storage, a blower or compressor to generate the necessary air pressure, a pipeline network for material transport, and a receiver for the discharged material. As coal ash particles are fed into the hopper, the blower creates a high-pressure air stream that draws the particles into the pipeline. The air and particles travel together through the pipeline, with the air providing the necessary momentum to transport the solid material. At the discharge point, the air is separated from the particles, often through a cyclone separator or a filter, allowing the coal ash to be collected in the receiver while the air is either recirculated or vented to the atmosphere.
The coal ash particle material pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is distinguished by several key features that enhance its performance and usability in industrial settings:
1. Efficient Dust Control: Unlike traditional mechanical conveyors, the pneumatic system operates in a closed pipeline, significantly reducing dust emissions and improving workplace safety. This is achieved through the sealed design of the hopper, pipeline, and receiver, which prevents particle leakage and dust dispersion.
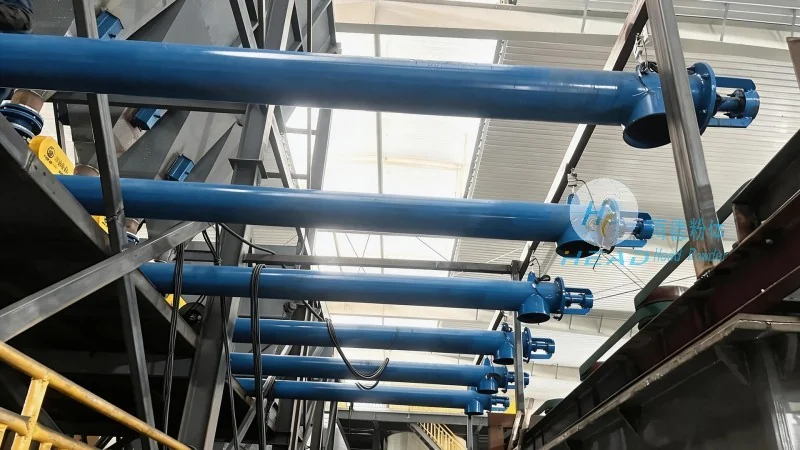
2. Low Maintenance Requirements: The absence of moving parts in the conveying line minimizes wear and tear, resulting in lower maintenance costs and longer equipment lifespan. The system is designed for easy access to components, facilitating routine inspections and repairs.
3. Flexible Layout and Scalability: The modular design of the pneumatic conveying system allows for easy integration into existing industrial layouts and expansion as production needs grow. The pipeline can be configured in various configurations, including vertical, horizontal, or a combination of both, to suit the specific requirements of the facility.
4. Energy Efficiency: Advanced blower technology and optimized air flow management contribute to energy savings, making the system cost-effective over its operational life. The system can be tailored to operate at optimal pressure levels, reducing energy consumption without compromising conveying efficiency.
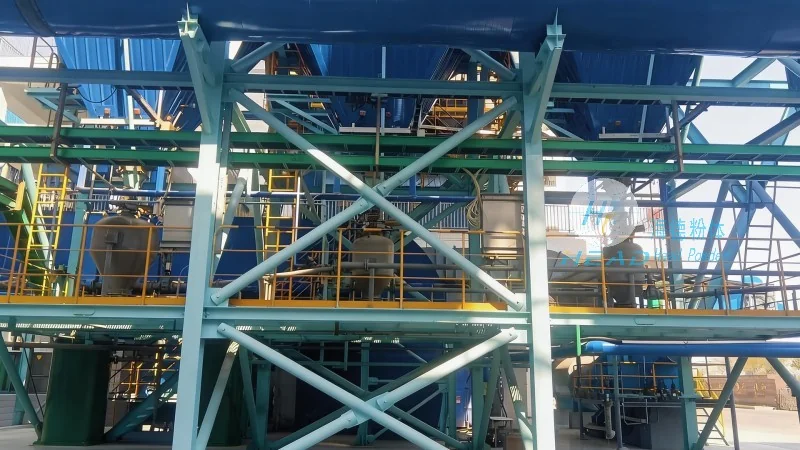
The coal ash particle material pneumatic conveying equipment is engineered to meet the demanding requirements of coal ash handling applications. Key technical specifications include:
- Conveying Capacity: The system can handle capacities ranging from low to high, depending on the specific model and configuration, ensuring compatibility with various production scales.
- Particle Size Range: Designed to efficiently transport coal ash particles with diameters typically ranging from 0.1 mm to several millimeters, accommodating the diverse particle size distributions common in coal ash.
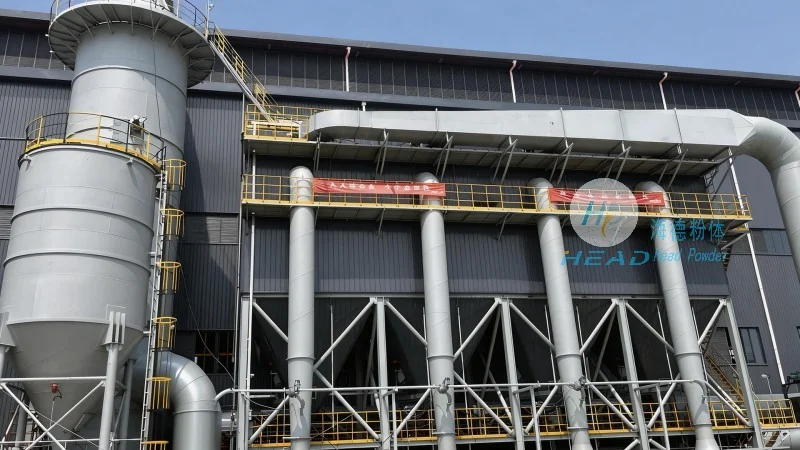
- Operating Pressure: The system operates at pressures ranging from low to moderate, with options available for both positive and negative pressure conveying, providing flexibility in system design.
- Material Compatibility: The equipment is constructed from materials resistant to corrosion and abrasion, such as stainless steel or special alloys, ensuring durability when handling abrasive coal ash particles.
The coal ash particle material pneumatic conveying equipment is widely used in power plants, cement factories, and other industrial facilities where coal ash needs to be transported from storage areas to processing units or disposal sites. Its ability to handle fine, abrasive particles makes it ideal for applications where traditional conveyors may fail. For example, in power plants, the system can efficiently transport coal ash from the boiler to the ash handling system, ensuring smooth operation and minimizing downtime.
Shandong HeadPowder Engineering Co., Ltd. stands as a trusted provider of high-quality pneumatic conveying solutions for coal ash and other industrial materials. The coal ash particle material pneumatic conveying equipment exemplifies the company's commitment to innovation, reliability, and customer satisfaction. By leveraging advanced technology and rigorous engineering, HeadPowder delivers systems that not only meet but exceed industry standards, ensuring efficient, safe, and sustainable material handling for their clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top