

Working Principle and Features of Phosphate Powder Material Pneumatic Conveying Equipment
Phosphate powder material pneumatic conveying equipment is a specialized system designed for the efficient and safe transportation of phosphate powders. This equipment is crucial in industrial applications where handling fine powders requires precision and reliability. The system is engineered to handle the unique properties of phosphate powders, such as their fine particle size and potential for dust generation, ensuring optimal performance and operational safety.
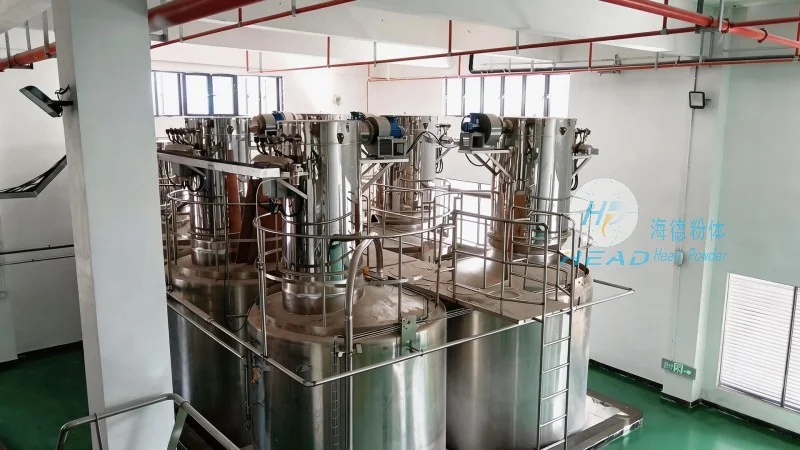
Introduction to Phosphate Powder Pneumatic Conveying Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in developing advanced pneumatic conveying solutions tailored to the demands of phosphate processing industries. The company's expertise lies in creating customized systems that address the specific challenges of transporting phosphate powders, including handling abrasive materials and maintaining consistent flow rates. With a focus on durability and efficiency, HeadPowder's equipment is designed to enhance productivity while minimizing downtime and operational costs.
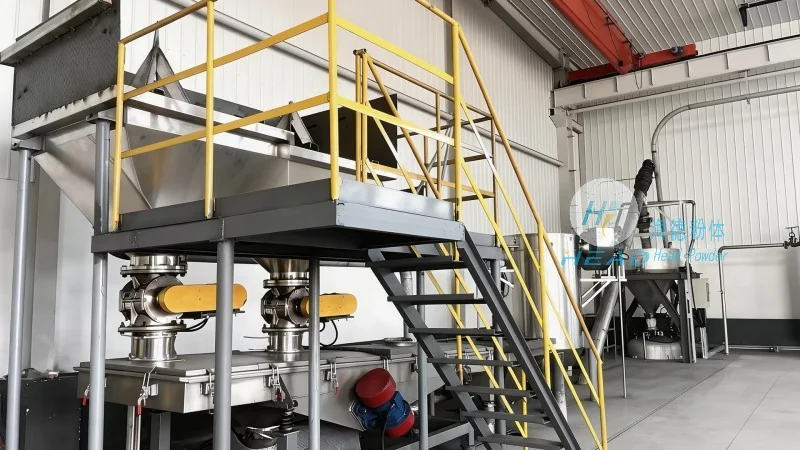
Working Principle of Pneumatic Conveying Equipment
The core mechanism of phosphate powder pneumatic conveying equipment involves the use of air to transport material through a pipeline system. The process typically starts with the material being fed into a hopper or feeder, where it is then introduced into a pipeline. A fan or blower generates the necessary air pressure, which propels the phosphate powder through the system. The conveying can be either positive or negative pressure, depending on the application requirements. The system ensures that the powder is transported in a controlled manner, preventing clogging and maintaining consistent flow. The design incorporates features such as cyclone separators and filters to separate the powder from the air, allowing for clean material recovery and air filtration.
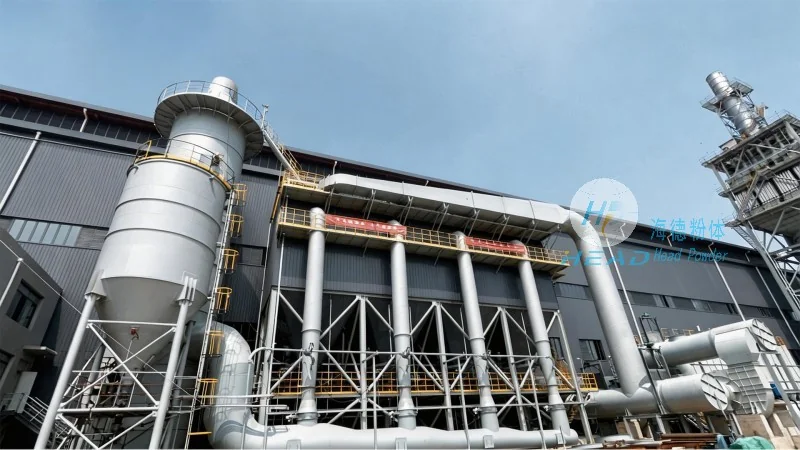
Key Features of Phosphate Powder Pneumatic Conveying Systems
HeadPowder's phosphate powder pneumatic conveying equipment is characterized by several key features that enhance its performance and reliability. One of the primary features is the robust construction, which is built to withstand the abrasive nature of phosphate powders and the high-pressure air flow. The equipment includes advanced control systems that allow for precise regulation of air pressure and material flow, ensuring consistent operation. Additionally, the system incorporates safety features such as pressure relief valves and dust suppression mechanisms to prevent accidents and maintain a safe working environment. The design also emphasizes energy efficiency, with optimized air flow and reduced power consumption, contributing to lower operational costs. The equipment is also designed for easy maintenance, with accessible components that facilitate regular inspections and repairs, minimizing downtime.
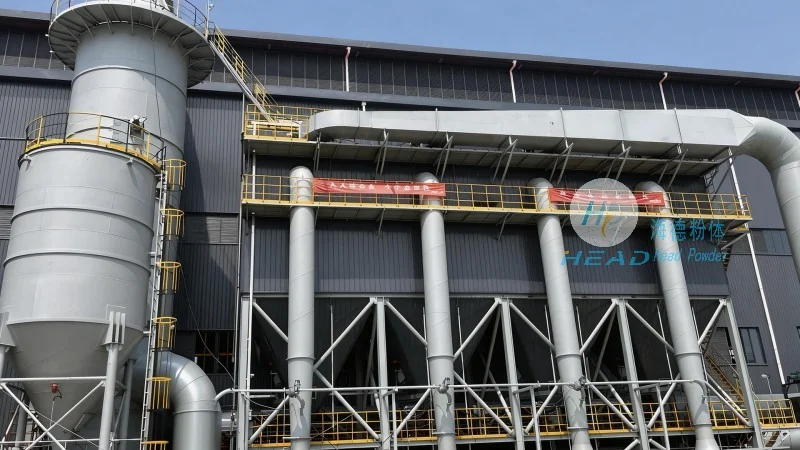
Applications and Benefits in Phosphate Processing
Phosphate powder pneumatic conveying equipment is widely used in various stages of phosphate processing, from raw material handling to product packaging. The system is particularly beneficial in applications where traditional bulk handling methods are inefficient or unsafe. By using pneumatic conveying, industries can achieve faster material transfer, reduced labor costs, and improved product quality. The equipment also helps in maintaining a clean and dust-free environment, which is crucial for compliance with environmental regulations. The benefits extend to increased productivity, as the system can handle high volumes of material with minimal intervention. Additionally, the equipment's flexibility allows for integration into existing processing lines, making it a cost-effective solution for upgrading or expanding phosphate processing facilities.