

[WTTLE]Working Principle and Features of Chicken Essence Material Pneumatic Conveying Equipment
Chicken essence, a vital ingredient in many food products, requires efficient and hygienic handling during processing. The chicken essence pneumatic conveying machine is a specialized piece of equipment designed to transport this delicate material with precision and care. This equipment is crucial for maintaining the quality and integrity of chicken essence, which is often used in soups, sauces, and other culinary applications. The machine operates by using air pressure to move the material through a system of pipes and ducts, ensuring a clean and controlled transfer process.
Working Principle of the Pneumatic Conveying System
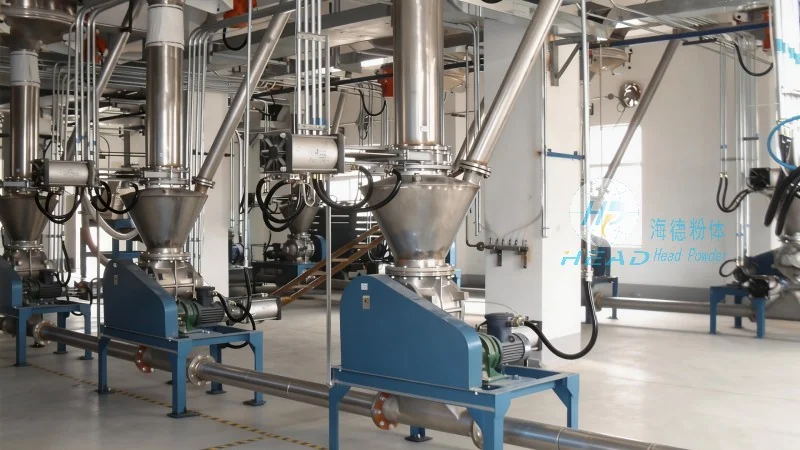
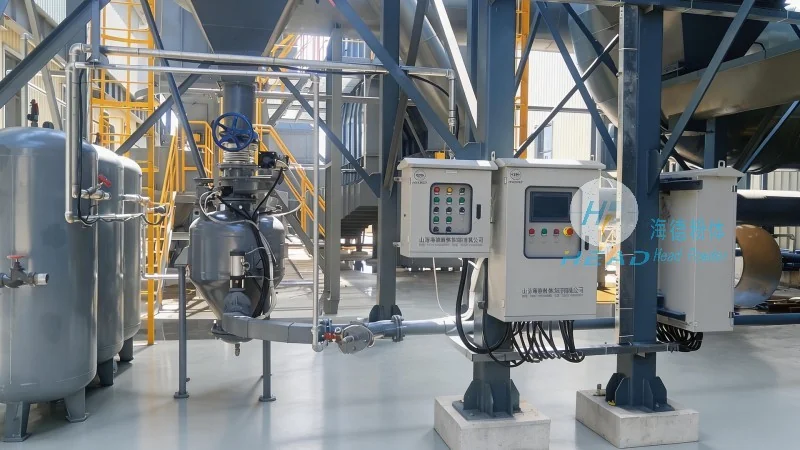
The core of the chicken essence pneumatic conveying machine lies in its pneumatic conveying technology. The system typically consists of a hopper where the chicken essence is loaded, a blower or compressor that generates the necessary air pressure, and a network of pipes that transport the material to the discharge point. As the air is introduced into the system, it creates a flow that carries the chicken essence particles through the pipes. The velocity and pressure of the air are carefully controlled to ensure that the material is moved without damage or degradation. This method is particularly effective for handling fine powders and liquids that are prone to caking or agglomeration, as it prevents direct contact between the material and the conveying equipment, reducing the risk of contamination and product loss.
Key Features and Advantages
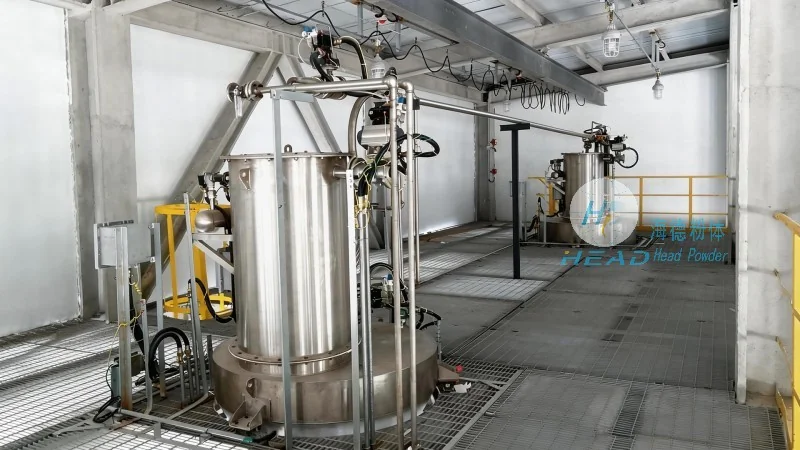
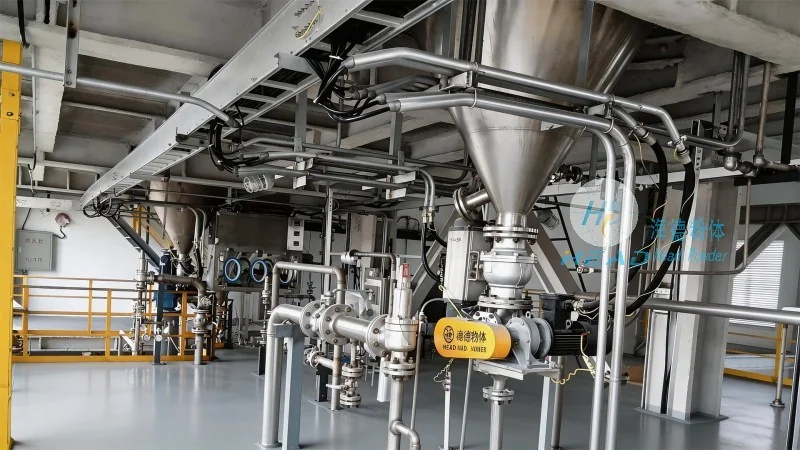
Several notable features distinguish the chicken essence pneumatic conveying machine from other conveying methods. Firstly, it offers a fully enclosed system, which is essential for maintaining the hygiene standards required in food processing. The sealed design prevents dust and contaminants from entering the environment, ensuring that the chicken essence remains pure and safe for consumption. Secondly, the machine is highly flexible in terms of layout and installation. It can be configured to fit various production line setups, allowing for easy integration into existing facilities. The system also provides excellent control over the conveying rate, enabling precise dosing of chicken essence into different products. Additionally, the pneumatic conveying process is energy-efficient compared to traditional methods like belt conveyors or bucket elevators, as it minimizes mechanical wear and reduces power consumption. Another advantage is the ability to handle both dry and liquid forms of chicken essence, making it versatile for different production needs. The machine's design also facilitates easy cleaning and maintenance, which is critical for maintaining compliance with food safety regulations.
Company Information and Background
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized conveying equipment for the food industry. With a focus on innovation and quality, the company has developed advanced solutions for handling delicate materials like chicken essence. HeadPowder's expertise in pneumatic conveying technology ensures that their equipment meets the highest standards of efficiency, hygiene, and durability. The company's facilities are located in Shandong, China, where they leverage local manufacturing capabilities to produce reliable and cost-effective solutions for global clients. By combining years of industry experience with cutting-edge engineering, HeadPowder provides tailored pneumatic conveying systems that address the specific needs of food processing operations, helping businesses maintain productivity while adhering to stringent safety and quality requirements.