With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Coal ash granular material conveying lines are essential systems in industrial applications, particularly in the handling and transportation of coal ash. These lines are designed to efficiently move coal ash from one location to another, ensuring smooth operations in power plants and related facilities. Understanding the working principle and key features of such lines is crucial for optimizing material handling processes and enhancing overall operational efficiency.
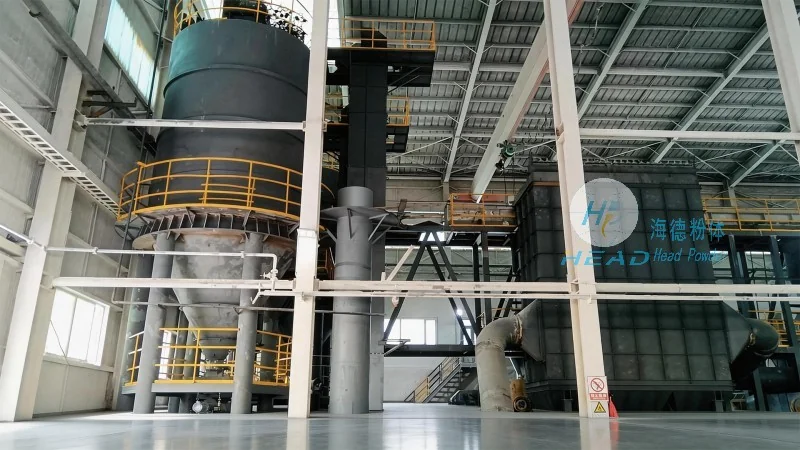
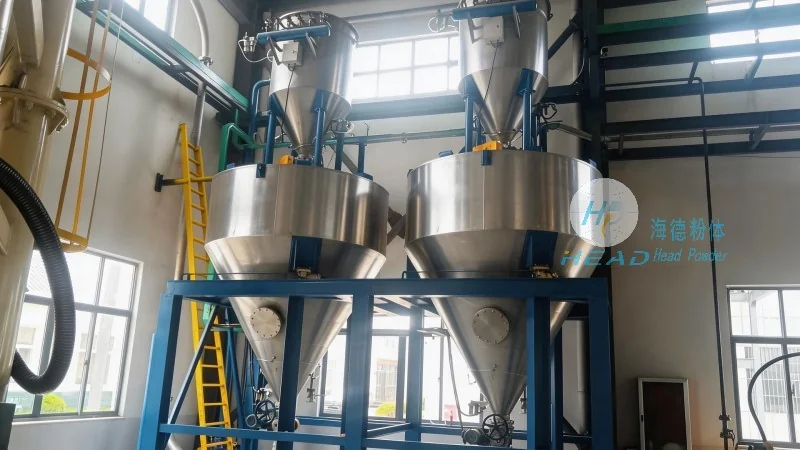
The core working principle of coal ash granular material conveying lines revolves around the use of mechanical equipment to transport coal ash particles. Typically, these systems employ screw conveyors, belt conveyors, or pneumatic conveyors, depending on the specific requirements of the application. The process begins with the collection of coal ash from storage silos or ash hoppers. The material is then fed into the conveyor system, where it is transported through a series of components, including feeders, conveyors, and discharge mechanisms. The mechanical action of the conveyor (such as the rotation of screws or the movement of belts) propels the coal ash forward, ensuring consistent and reliable material flow. Additionally, the system may incorporate control mechanisms to regulate the speed and volume of material transport, allowing for precise management of the conveying process. This ensures that the coal ash is delivered to its intended destination without any blockages or inefficiencies.
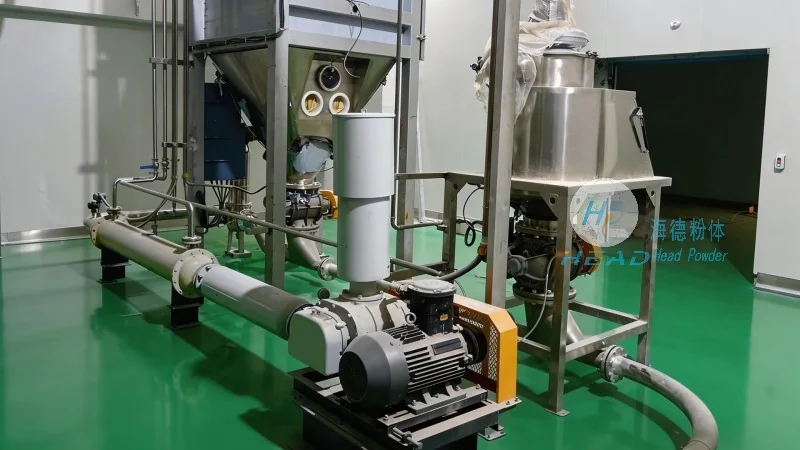
Coal ash granular material conveying lines are characterized by several key features that enhance their performance and reliability. One of the primary features is their robust construction, which is designed to withstand the abrasive nature of coal ash particles. The materials used in the construction of the conveyors, such as high-strength steel and corrosion-resistant coatings, ensure long-term durability and minimal maintenance requirements. Another important feature is the system's adaptability, allowing it to handle varying particle sizes and moisture content of coal ash. This flexibility is achieved through adjustable feed mechanisms and variable speed controls, which can be tailored to the specific characteristics of the material being conveyed. Furthermore, the conveying lines are equipped with safety features, including overload protection and emergency stop functions, to prevent accidents and ensure operator safety. The integration of advanced monitoring systems, such as level sensors and temperature indicators, provides real-time data on the system's performance, enabling proactive maintenance and troubleshooting. These features collectively contribute to the efficient and safe operation of coal ash granular material conveying lines.
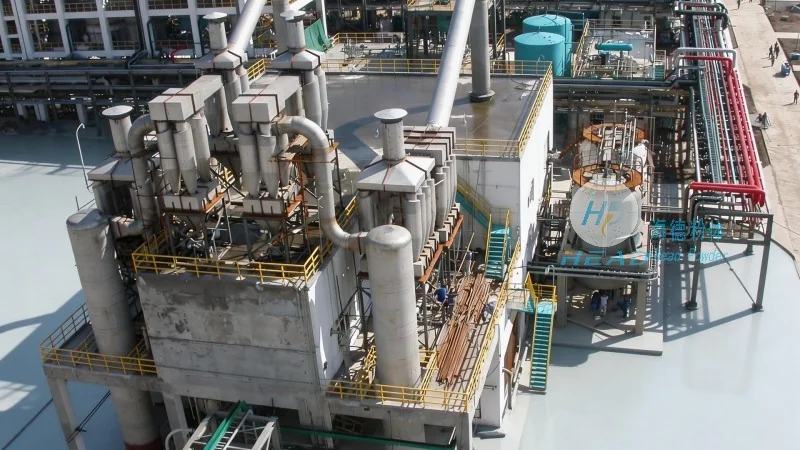
Shandong HeadPowder Engineering Co., Ltd., based in China, is a leading manufacturer and supplier of industrial material handling equipment. With a strong commitment to quality and innovation, HeadPowder specializes in designing and manufacturing coal ash granular material conveying lines that meet the highest industry standards. The company's expertise in mechanical engineering and material science enables the development of customized solutions tailored to the unique needs of power plants and industrial facilities. HeadPowder's products are known for their durability, efficiency, and reliability, ensuring long-term performance and minimal downtime. The company's team of experienced engineers and technicians provides comprehensive support, from initial consultation and design to installation and after-sales service. By choosing HeadPowder, clients can benefit from advanced technology, superior craftsmanship, and dedicated customer service, ensuring the successful implementation of their material handling projects.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top