

What is a Fine Powder Conveying System Equipment? What Are Its Design Principles?
For industries dealing with fine powders, efficient and reliable material handling is crucial. The fine powder conveying system equipment plays a vital role in ensuring smooth operations, from raw material transport to processing and storage. Understanding its design principles is essential for optimizing performance and maintaining product quality. This article explores the key aspects of fine powder conveying systems, focusing on their functionality and engineering design.
Introduction to Fine Powder Conveying System Equipment
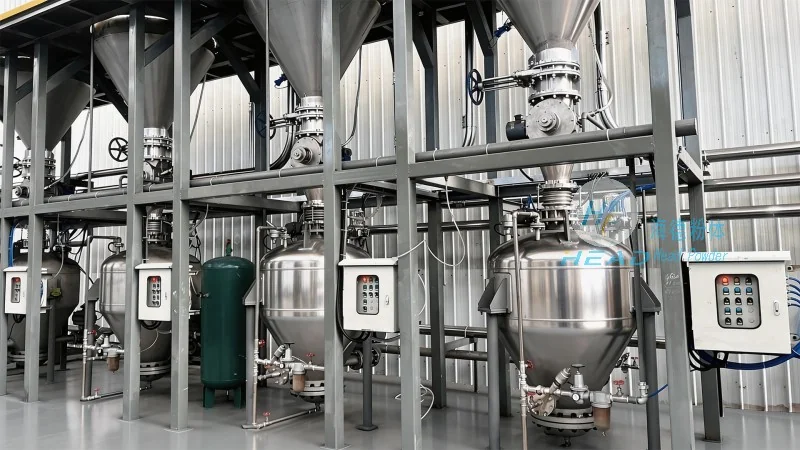
Fine powder conveying systems are specialized devices engineered to transport fine powders, such as cement, flour, or chemical powders, over long distances with minimal loss and maximum efficiency. These systems are widely used in various industries, including construction, food processing, and pharmaceuticals, where the handling of fine powders requires precision and control. The equipment typically consists of components like hoppers, feeders, conveying mechanisms, and control systems, all working in harmony to achieve seamless material movement.
Design Principles of the Fine Powder Conveying System
The design of a fine powder conveying system is based on several critical principles to ensure optimal performance. First, the system must address the challenges of powder flow, such as bridging, caking, and segregation, which can lead to uneven material transport. Engineers employ various techniques, including aeration, vibration, and proper hopper design, to mitigate these issues. Second, the conveying mechanism must be selected based on the powder characteristics, including particle size, density, and moisture content. Common types include pneumatic conveying (air-assisted) and mechanical conveying (e.g., screw conveyors or belt conveyors). The choice of mechanism impacts the system's efficiency, energy consumption, and suitability for different applications.
Key Components and Their Functions
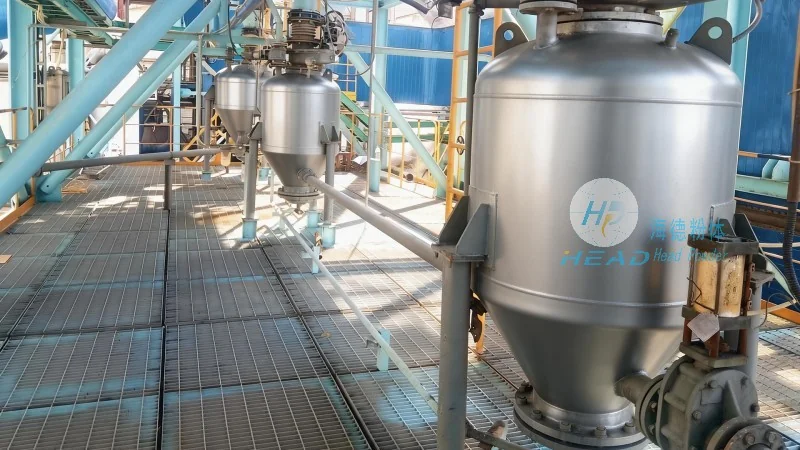
Several key components make up a fine powder conveying system, each playing a specific role in the overall operation. The hopper is the initial storage unit where raw materials are loaded. Its design, including the angle of the walls and the presence of a discharge gate, is crucial for preventing material bridging and ensuring smooth flow. The feeder, often a rotary valve or a star feeder, regulates the flow rate of the powder into the conveying line, maintaining consistent material delivery. The conveying mechanism, whether pneumatic or mechanical, transports the powder from the feeder to the destination. Pneumatic systems use compressed air to create a flow, while mechanical systems rely on mechanical force, such as screws or belts. Finally, the control system monitors and adjusts the operation of the entire system, ensuring it operates within safe and efficient parameters.
Advantages of Fine Powder Conveying Systems
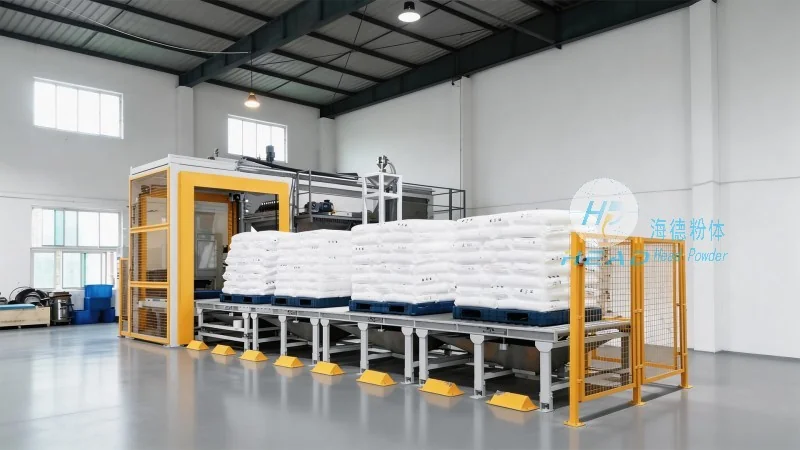
Implementing a fine powder conveying system offers numerous advantages for industrial operations. One of the primary benefits is the reduction in material loss and contamination, as the system minimizes exposure to the environment. This is particularly important for products that require high purity, such as pharmaceuticals or food ingredients. Additionally, these systems enhance operational efficiency by automating the material handling process, reducing labor costs and human error. The ability to transport powders over long distances without the need for intermediate storage also streamlines production workflows. Furthermore, fine powder conveying systems are designed to be flexible, allowing for adjustments in flow rate and direction to accommodate varying production demands.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in fine powder conveying system equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner for industries requiring reliable material handling solutions. HeadPowder's products are designed to meet the specific needs of various applications, ensuring optimal performance and durability. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. HeadPowder's commitment to customer satisfaction and product excellence has earned it a reputation for delivering high-quality solutions tailored to the unique requirements of each client.