With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When it comes to the efficient and reliable transportation of brown sugar, selecting the right conveying method is crucial for maintaining product quality and operational efficiency. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, offers a range of advanced solutions tailored to meet diverse industrial needs. This article explores the common methods used for brown sugar conveying, highlighting their applications, advantages, and considerations for optimal performance.
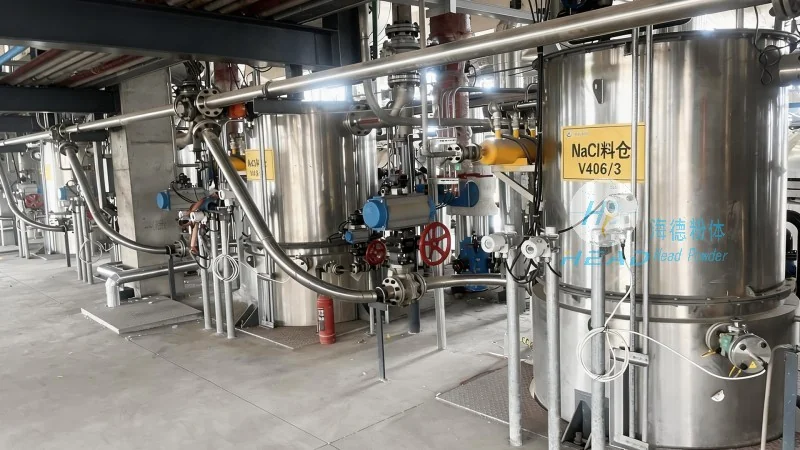
Screw conveyors, also known as auger conveyors, are among the most widely used equipment for transporting brown sugar. These systems consist of a rotating helical screw inside a U-shaped or cylindrical housing. As the screw rotates, it moves the sugar material forward through the housing. For brown sugar, which can be granular or in a semi-liquid state, screw conveyors provide gentle handling, minimizing product degradation and dust generation. The design allows for vertical or inclined transport, making it suitable for both short and long-distance applications. Shandong HeadPowder Engineering Co., Ltd. specializes in customizing screw conveyor systems to accommodate varying capacities and material characteristics, ensuring seamless integration into existing production lines.
Belt conveyors represent another popular choice for brown sugar conveying, particularly in large-scale operations. These systems utilize a continuous belt looped over rollers to transport the material. The belt can be made from materials such as rubber or PVC, which are resistant to sugar and moisture. Belt conveyors are ideal for horizontal or slightly inclined transport over longer distances, offering high throughput and low maintenance requirements. They are commonly used in sugar processing plants to move brown sugar from storage silos to processing units or packaging areas. The smooth operation of belt conveyors ensures minimal product breakage and consistent flow rates, contributing to overall operational efficiency.
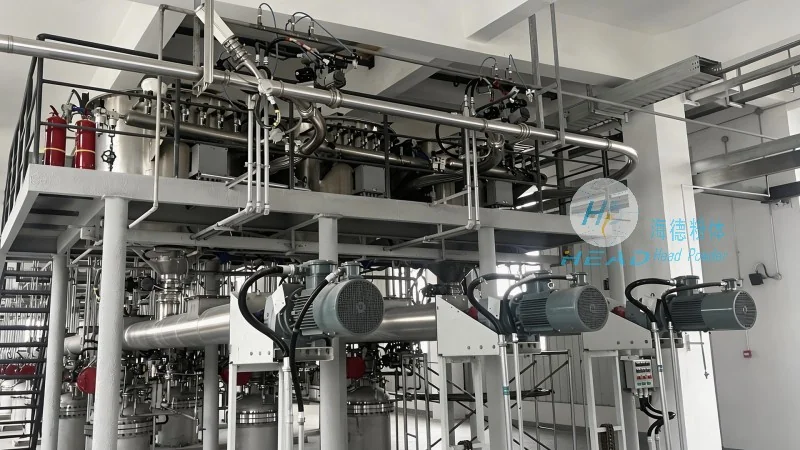
Pneumatic conveying systems employ air or gas to transport brown sugar in a closed pipeline. This method is particularly effective for handling fine or powdery sugar, as it prevents dust contamination and allows for flexible routing. There are two main types of pneumatic conveyors: dilute-phase and dense-phase. Dilute-phase systems use low air velocity to move the material, while dense-phase systems use higher air pressure to push the sugar in a slurry-like state. Pneumatic conveying offers advantages such as dust-free operation, the ability to transport materials over long distances without intermediate storage, and compatibility with existing infrastructure. Shandong HeadPowder Engineering Co., Ltd. designs pneumatic conveying solutions that optimize air usage and material transport, ensuring energy efficiency and reduced operational costs.
For vertical transport of brown sugar, bucket elevators are an excellent choice. These systems consist of a vertical or inclined frame with a continuous chain or belt carrying buckets. As the buckets move upward, they scoop up the sugar and discharge it at the top. Bucket elevators are capable of handling large volumes of material and can transport brown sugar from ground-level storage to elevated processing areas or silos. They are particularly useful in facilities where vertical space is limited or where multiple levels of processing are required. The enclosed design of bucket elevators minimizes dust and spillage, maintaining a clean and safe working environment. Shandong HeadPowder Engineering Co., Ltd. provides bucket elevator systems that are robust and durable, designed to withstand the abrasive nature of brown sugar and ensure long-term reliability.
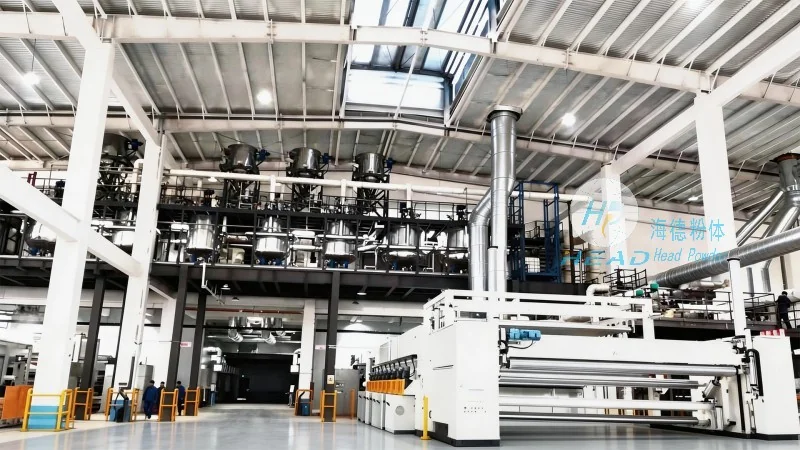
Vibrating conveyors use vibrations to move brown sugar along a trough. The system consists of a trough supported by vibration motors, which cause the material to move forward through the trough. This method is ideal for handling delicate or sticky brown sugar, as it provides gentle and continuous movement without causing product degradation. Vibrating conveyors are commonly used in applications where the material needs to be transported at a controlled speed or where the conveyor must operate in a compact space. They are particularly effective for horizontal or slightly inclined transport and can be customized with different trough angles and vibration frequencies to suit specific material characteristics. Shandong HeadPowder Engineering Co., Ltd. offers vibrating conveyor solutions that ensure minimal product breakage and consistent flow, enhancing overall process efficiency.
Hydraulic conveying systems use water or other fluids to transport brown sugar, especially in applications where the material is in a slurry form. The system involves pumping the sugar slurry through a pipeline, with the fluid providing the necessary pressure to move the material. Hydraulic conveying is suitable for long-distance transport and can handle large volumes of material with high efficiency. It is commonly used in sugar processing plants where the brown sugar is mixed with water for processing or transportation. The advantage of hydraulic conveying is its ability to transport material through complex layouts and over uneven terrain, making it a versatile option for challenging environments. Shandong HeadPowder Engineering Co., Ltd. designs hydraulic conveying systems that optimize fluid usage and material transport, ensuring reliable operation and minimal maintenance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top