With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the various types, key features, and practical applications of PFA (Polytetrafluoroethylene) pneumatic conveying systems is crucial for industries seeking efficient material handling solutions. These systems are engineered to handle a wide range of materials, including those with high moisture content, abrasive properties, or sensitivity to contamination. The expertise of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field, provides clients with tailored solutions that meet specific operational requirements.
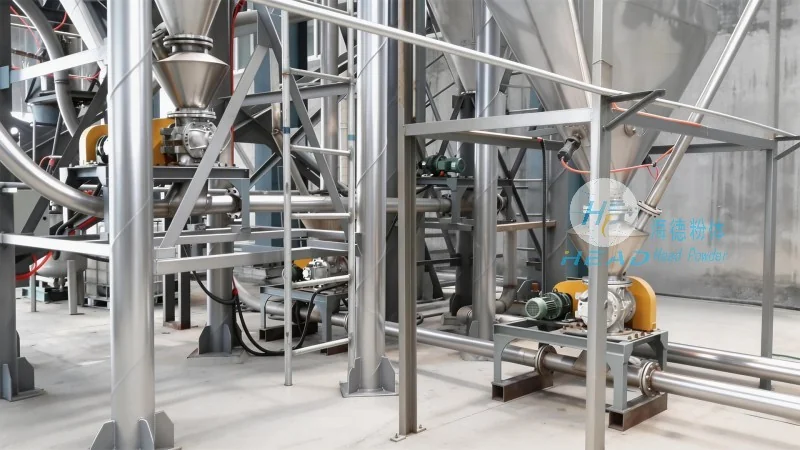
PFA pneumatic conveying systems are available in several configurations, each designed to address different material handling challenges. The primary types include dilute phase and dense phase systems, which differ in their operational principles and suitability for various materials. Dilute phase systems utilize low-pressure air to transport materials in a suspended state, making them ideal for light to medium-density powders and granules. In contrast, dense phase systems employ higher pressure and lower air velocity to move materials in a more compacted form, reducing the risk of product degradation and ensuring a more controlled discharge. HeadPowder specializes in customizing these systems to match the unique characteristics of each material, ensuring optimal performance and efficiency.
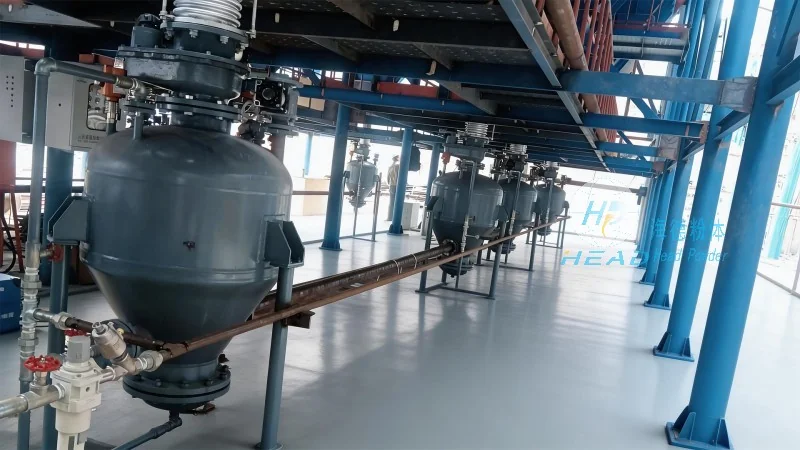
The PFA material used in these systems offers several advantages that enhance their performance and durability. PFA is known for its excellent chemical resistance, making it suitable for handling aggressive or corrosive materials without degradation. Additionally, PFA provides superior resistance to high temperatures, allowing the systems to operate in environments where other materials would fail. The smooth inner surface of PFA components minimizes friction and product buildup, reducing maintenance requirements and extending the system's lifespan. These features, combined with the ability to handle a wide range of materials, make PFA pneumatic conveying systems a reliable choice for industrial applications.
PFA pneumatic conveying systems find applications across multiple industries, including chemical processing, pharmaceuticals, food and beverage, and mining. In the chemical industry, they are used to transport powders and granules that require strict contamination control, such as pharmaceutical intermediates or specialty chemicals. The food and beverage sector benefits from PFA systems due to their hygienic design and resistance to cleaning agents, ensuring compliance with regulatory standards. Mining operations utilize these systems to transport raw materials efficiently, reducing the need for manual handling and improving overall productivity. HeadPowder's expertise in designing and manufacturing PFA pneumatic conveying systems ensures that clients receive solutions tailored to their specific industry needs, providing reliable and efficient material handling solutions.
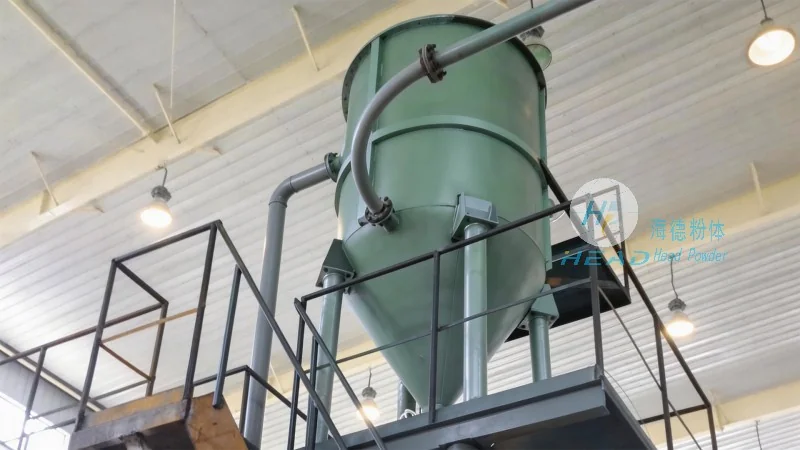
Shandong HeadPowder Engineering Co., Ltd. offers comprehensive services to ensure that clients receive the most suitable PFA pneumatic conveying system for their operations. The company provides detailed consultations to assess material properties, process requirements, and operational constraints, enabling the design of customized systems that maximize efficiency and minimize downtime. HeadPowder's team of engineers and technicians work closely with clients to develop solutions that address specific challenges, such as material segregation or product degradation. The company also provides installation and commissioning services, ensuring that the systems are properly set up and tested for optimal performance. With a focus on quality and customer satisfaction, HeadPowder delivers reliable PFA pneumatic conveying systems that meet the highest industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top