With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.

In the realm of industrial material handling, the efficient and safe transportation of fine powders remains a critical challenge for manufacturers worldwide. One of the most demanding applications involves the handling of carbon black, a fine black powder used extensively in the rubber and plastic industries. Shandong Headpowder Engineering Co., Ltd. has successfully addressed these challenges with a specialized solution implemented in the United Kingdom. This project, known as the Birmingham Carbon Black Negative Pressure Pneumatic Conveying Case, highlights the company's expertise in delivering high-performance air conveying systems tailored for complex European environments. The project not only improved operational efficiency but also set a new standard for dust control and safety in the facility.
The implementation of this system in Birmingham serves as a prime example of modern industrial engineering. By utilizing state-of-the-art pneumatic conveying technology, the facility was able to transition from manual handling methods to a fully automated, centralized system. This case study demonstrates how advanced air transport solutions can be integrated into existing infrastructure to solve persistent logistical problems. The focus was on creating a robust pipeline network that could withstand the abrasive nature of carbon black while maintaining a sealed environment to prevent environmental contamination.
Carbon black is unique in its physical properties, presenting specific difficulties that standard conveyor systems often cannot handle. As a fine, high-particle-density material, it tends to float in the air and is highly susceptible to static electricity. In the context of the Birmingham facility, the primary concerns were occupational health, fire safety, and the containment of dust. Traditional mechanical conveyors, such as screw feeders or bucket elevators, often struggle with these issues, leading to leakage and potential hazards.
The need for a specialized pneumatic conveying case solution became evident when the facility sought to upgrade its processing capabilities. The goal was to transfer carbon black from multiple storage points to a central processing unit without allowing the powder to disperse into the workshop air. This is where the concept of negative pressure air transport becomes indispensable. By creating a vacuum within the transport lines, the system effectively pulls the material through the pipes, ensuring that the powder never escapes into the open environment. This approach is particularly vital in European industrial settings, where environmental regulations regarding particulate matter are exceptionally strict.
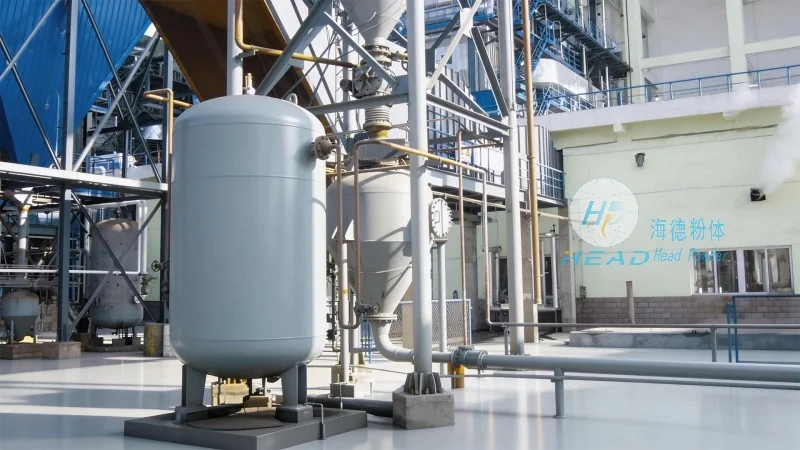
The core of the Birmingham project is the application of negative pressure centralized pneumatic conveying. Unlike positive pressure systems that push material through pipes, negative pressure systems operate by sucking material in. This fundamental difference offers several advantages, particularly in dust containment. In the Birmingham plant, the system was designed to create a consistent vacuum within the pipeline network, drawing carbon black from various collection hoppers and directing it to a central collection silo or processing area.
This technology is often referred to as a European pneumatic conveying solution due to its alignment with the high standards of European industrial automation. The system utilizes a central vacuum generator, often a Roots blower or a liquid ring vacuum pump, to maintain the necessary suction. The pipes are connected to different points in the factory floor, creating a spider-web-like network that ensures all carbon black is captured. This centralized approach simplifies the control system, as operators only need to manage one central unit rather than multiple individual feeders. The result is a streamlined process that significantly reduces the footprint of the material handling equipment on the factory floor.
A successful pneumatic conveying system relies on a suite of precision-engineered components. In the Birmingham carbon black project, every valve, elbow, and filter was selected to optimize performance. The system typically includes a series of rotary valves or slide gates at the pickup points to control the feed rate into the vacuum lines. These components are designed to handle the abrasive nature of carbon black without excessive wear, ensuring a long service life for the equipment.
One of the standout features of this Birmingham pneumatic conveying installation is the advanced filtration system. As carbon black is transported, the air must be cleaned before being released back into the atmosphere. The system employs high-efficiency bag filters or cartridge filters that capture even the finest particles of carbon black. This not only protects the vacuum pump from clogging but also ensures that the factory remains compliant with environmental standards. The automated cleaning cycle of these filters further enhances the system's efficiency, requiring minimal human intervention.
The operational logic of the system is designed for maximum reliability. Sensors monitor the pressure and flow within the pipes, automatically adjusting the vacuum levels to ensure a consistent transport rate. If a blockage occurs, the system is equipped with safety mechanisms to prevent damage. This level of automation is a hallmark of Shandong Headpowder Engineering Co., Ltd.'s engineering philosophy, ensuring that the client in Birmingham experiences minimal downtime and consistent production output.
The deployment of this negative pressure system delivered immediate and long-term benefits to the Birmingham facility. The most significant advantage was the drastic improvement in workplace safety. By eliminating open handling and dust clouds, the risk of respiratory issues among employees was significantly reduced. Furthermore, the elimination of dust accumulation on electrical equipment and machinery lowered the risk of fire, a critical safety concern when handling combustible powders like carbon black.
Operational efficiency was also a major win. The automated nature of the system meant that material transfer was continuous and uninterrupted. The centralization of the conveying process reduced the need for forklifts and manual labor, freeing up floor space and allowing staff to focus on value-added tasks. The system's ability to handle high volumes of carbon black with low energy consumption also contributed to the facility's operational cost savings. This case stands as a testament to the effectiveness of modern pneumatic conveying cases in optimizing industrial workflows.
The success of the Birmingham project is attributed to the technical expertise and dedicated service of Shandong Headpowder Engineering Co., Ltd.. Based in Shandong, China, Headpowder has established itself as a leading provider of powder handling solutions globally. The company specializes in the design, manufacturing, and installation of pneumatic conveying systems, dust collectors, and material handling equipment. Their team of engineers possesses deep knowledge of various industries, including chemical, pharmaceutical, and food processing, allowing them to customize solutions to meet specific client requirements.
Headpowder takes pride in its ability to deliver comprehensive solutions that address the entire material handling lifecycle. From the initial site survey and system design to the final commissioning and after-sales support, the company ensures a seamless experience for its clients. Their reputation for quality and reliability has made them a preferred partner for industrial projects in Europe and beyond. The Birmingham carbon black project is a shining example of their capability to handle complex challenges and deliver superior results.
In conclusion, the United Kingdom Birmingham carbon black negative pressure centralized pneumatic conveying case represents a milestone in industrial material handling. It showcases how advanced engineering can solve critical challenges related to dust, safety, and efficiency. For facilities looking to upgrade their handling systems or implement new ones, this project serves as a model of excellence. Shandong Headpowder Engineering Co., Ltd. continues to lead the industry with innovative solutions and a commitment to customer satisfaction.
If you are interested in learning more about this case or require a similar pneumatic conveying solution for your facility, please do not hesitate to contact our team. You can reach our project manager, Manager Zhang, for detailed consultations. You can contact us via WeChat at 15662777102. We are ready to assist you in designing the most efficient and safe pneumatic conveying system for your specific needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top