With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Gravity dust removal material conveying lines are critical components in industrial processes, particularly in sectors dealing with bulk materials and airborne particulates. These systems combine material handling with dust control, ensuring efficient operation while maintaining environmental compliance. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced gravity dust removal material conveying lines tailored to diverse industrial needs.

At Shandong HeadPowder Engineering Co., Ltd., we understand the importance of reliable material conveying and dust control in modern industrial operations. Our gravity dust removal material conveying lines are engineered to address the challenges of transporting bulk materials while effectively capturing and removing airborne dust particles. This article explores the underlying principles, operational characteristics, and practical applications of these systems, highlighting how they contribute to enhanced productivity and environmental safety.
The core principle of gravity dust removal material conveying lines revolves around the use of gravity and aerodynamic separation to transport materials and filter out dust. The system typically consists of a hopper or inlet where raw material is fed, followed by a series of inclined or horizontal chutes that allow material to move under the influence of gravity. Simultaneously, air is drawn through the system, and dust particles are separated from the material stream due to differences in density and size. The clean material continues along the conveying path, while the collected dust is directed to a collection bin or filtration system. This dual-function design ensures efficient material transport and effective dust removal, minimizing the risk of dust contamination in the workplace and surrounding environment.
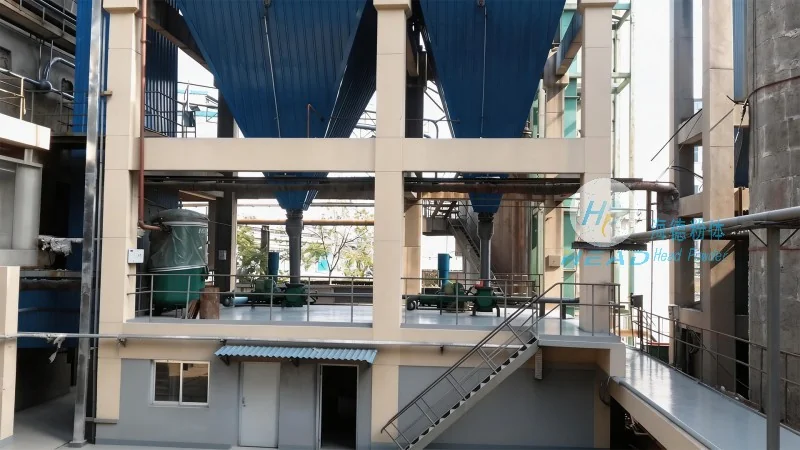
Gravity dust removal material conveying lines are designed to operate in various industrial settings, each with distinct characteristics that influence their performance and application. These systems are particularly well-suited for environments where material handling and dust control are paramount, such as power plants, cement factories, and chemical processing facilities. The working scene characteristics include: 1. **High Material Throughput**: The ability to handle large volumes of bulk materials without compromising dust removal efficiency. 2. **Low Energy Consumption**: Gravity-driven operation reduces the need for external power sources, making the system cost-effective and environmentally friendly. 3. **Space Efficiency**: Compact design allows installation in confined areas, adapting to the spatial constraints of industrial sites. 4. **Dust Control Compliance**: Built-in filtration and collection mechanisms help meet regulatory standards for air quality, ensuring safe and legal operation. 5. **Durability and Maintenance**: Robust construction with easy-to-clean components minimizes downtime and maintenance costs, enhancing long-term operational reliability.
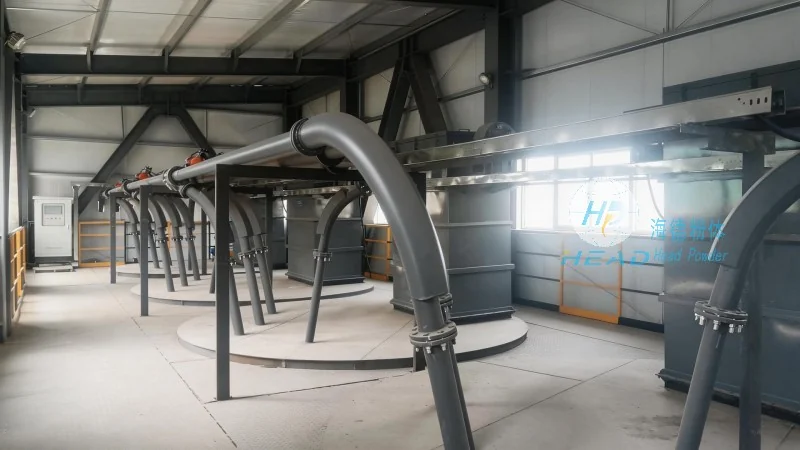
Our gravity dust removal material conveying lines incorporate several technical features that enhance their performance and adaptability. Key features include: - **Gravity-Driven Conveying**: Utilizes the natural force of gravity to move materials, reducing mechanical wear and energy consumption. - **Aerodynamic Dust Separation**: Advanced air flow management and particle separation technology ensures high dust capture rates, even for fine particulates. - **Modular Design**: Flexible and customizable components allow for adaptation to specific material types and process requirements. - **Integrated Dust Collection**: Built-in filtration systems, such as cyclones or bag filters, effectively capture and store dust, preventing re-entry into the workspace. - **Material Compatibility**: Constructed from corrosion-resistant and wear-resistant materials, suitable for handling a wide range of bulk materials, including powders, granules, and bulk solids. These features collectively contribute to the efficiency, reliability, and longevity of the conveying lines.
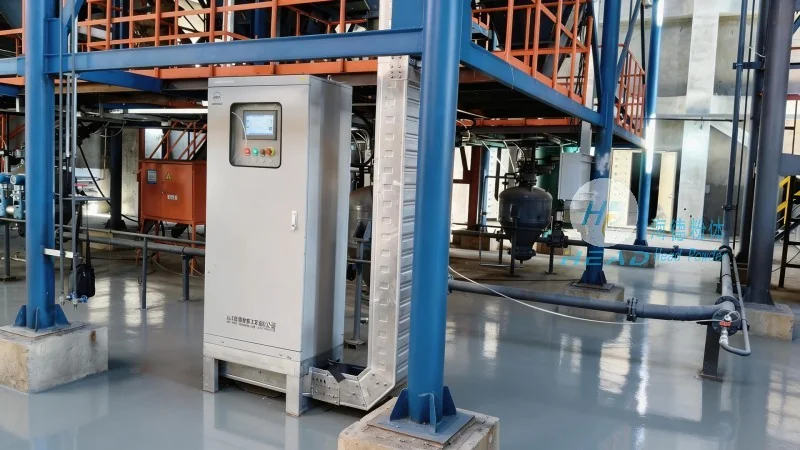
Gravity dust removal material conveying lines are widely used in various industrial applications, demonstrating their versatility and effectiveness. For instance, in thermal power plants, these systems transport coal or ash while capturing fine dust particles, preventing air pollution and ensuring safe material handling. In cement manufacturing, they convey raw materials and finished products while controlling dust emissions, contributing to cleaner production processes. Additionally, in chemical and pharmaceutical industries, the systems handle powders and granules with minimal dust generation, maintaining product quality and workplace safety. These applications highlight the adaptability of gravity dust removal material conveying lines to different industrial needs and operational conditions.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of industrial material handling and dust control solutions. Headquartered in Shandong, China, the company specializes in designing, manufacturing, and installing advanced gravity dust removal material conveying lines and related equipment. With a commitment to quality, innovation, and customer satisfaction, HeadPowder provides tailored solutions that meet the unique requirements of each industrial client. The company’s products are known for their reliability, efficiency, and compliance with international standards, making them a trusted choice in the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top