With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Camellia seed material conveying lines represent a critical component in the efficient processing of oilseeds, particularly within the context of camellia oil extraction. These systems are engineered to manage the unique physical attributes of camellia seeds, ensuring a seamless and continuous flow from raw material reception through to subsequent processing stages. The technology underpinning these lines integrates mechanical engineering principles with material handling expertise to optimize throughput while minimizing operational disruptions.
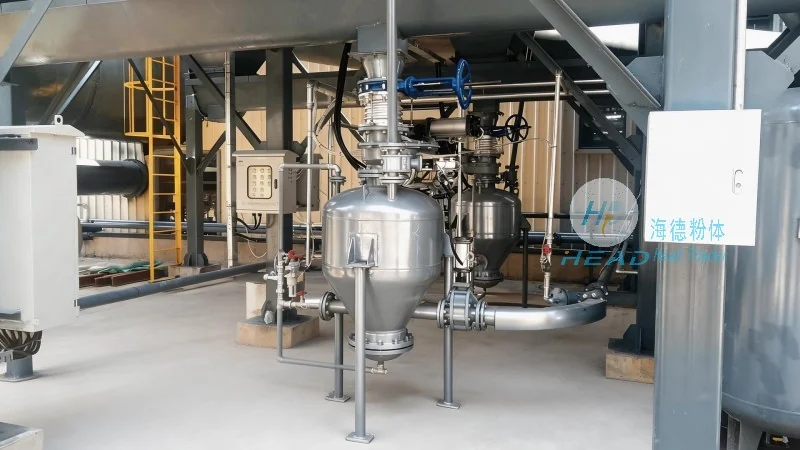
The fundamental operational principle of camellia seed material conveying lines centers on the utilization of specialized equipment to transport seeds through various processing phases. Key system components include feeders, conveyors, and sorting mechanisms that operate in concert to maintain consistent material flow. The design accommodates the varying sizes and densities of camellia seeds, ensuring each seed is transported without damage or loss. This is achieved through adjustable speed controls, variable tension systems, and robust construction materials that resist wear and tear from continuous operation.
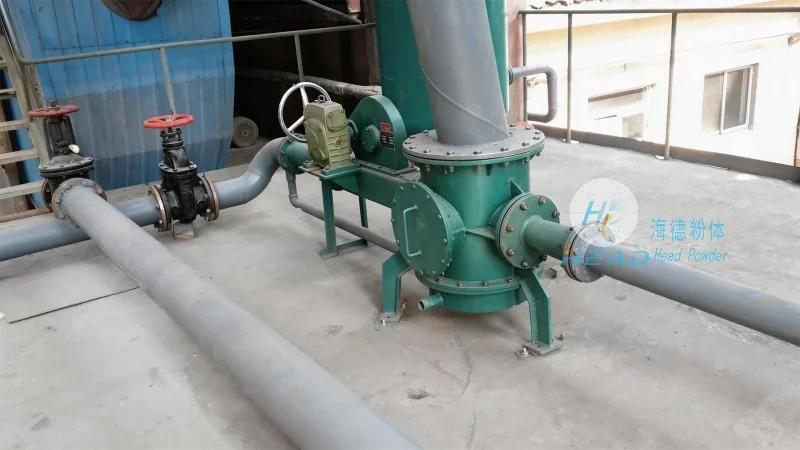
The operational characteristics of camellia seed material conveying lines are tailored to the specific demands of industrial oil extraction facilities. These systems are typically deployed in settings where large volumes of raw material require rapid and efficient processing. The design emphasizes durability and reliability, as downtime can significantly impact production output. Additionally, the conveying lines are engineered for seamless integration with other processing equipment, such as oil presses and filtration units, creating a cohesive production line. This integration allows for a streamlined workflow, reducing the need for manual handling and associated labor costs.
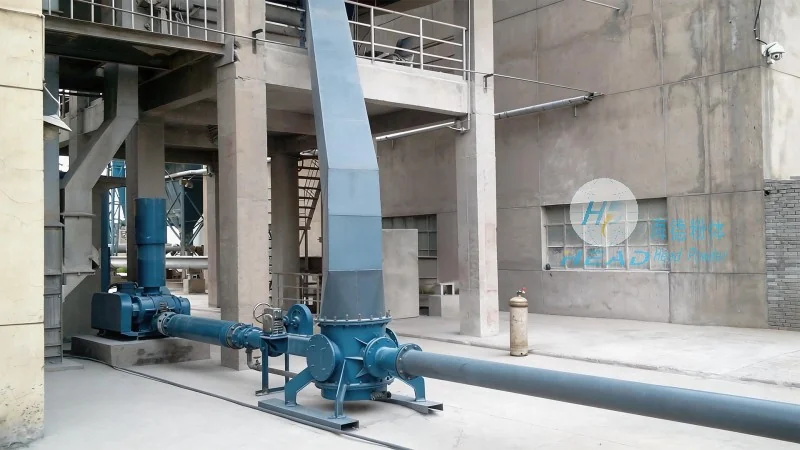
Camellia seed material conveying lines are available in diverse configurations to suit different production scales and operational requirements. For small to medium-sized processing facilities, compact conveyor systems with adjustable speed settings are common, capable of handling up to 5 tons of material per hour for batch processing. In larger industrial plants, high-capacity conveyors with automated feeding mechanisms are employed, processing up to 20 tons per hour. The systems are constructed from stainless steel and other corrosion-resistant materials, ensuring longevity and compliance with food safety standards. Applications extend beyond oil extraction to include seed cleaning, grading, and packaging, making these lines versatile solutions for the entire camellia seed processing chain.
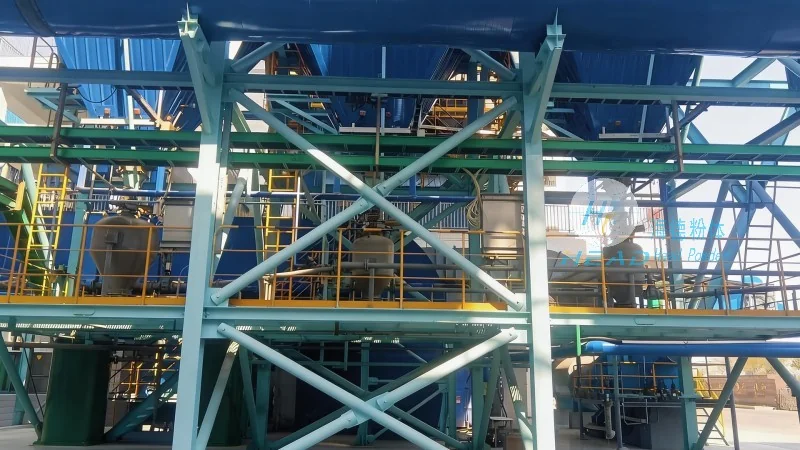
HeadPowder, a leading manufacturer of material handling solutions, specializes in designing and manufacturing camellia seed material conveying lines. With headquarters in Shandong, China, the company leverages over two decades of experience in the engineering and processing industries. Shandong HeadPowder Engineering Co., Ltd. focuses on delivering customized solutions that meet the unique needs of clients, from small-scale farms to large industrial operations. The company’s team of engineers and technicians collaborates closely with clients to understand operational challenges and develop tailored conveying systems. HeadPowder’s commitment to quality and innovation has earned the company a reputation for reliability and efficiency in the market. By combining advanced technology with local manufacturing expertise, the company ensures its products are both cost-effective and high-performing, providing long-term value to customers.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top