

Principle and Working Scene Characteristics of Automatic Tonne Bag Feeding Powder Material Conveyor
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer specializing in powder material handling equipment. The company is headquartered in Shandong, China, and has been dedicated to providing efficient and reliable solutions for powder conveying and feeding applications. Among its product lineup, the automatic tonne bag feeding powder material conveyor stands out as a key solution for industries requiring large-scale, automated powder handling.
The Principle of the Automatic Tonne Bag Feeding Powder Material Conveyor
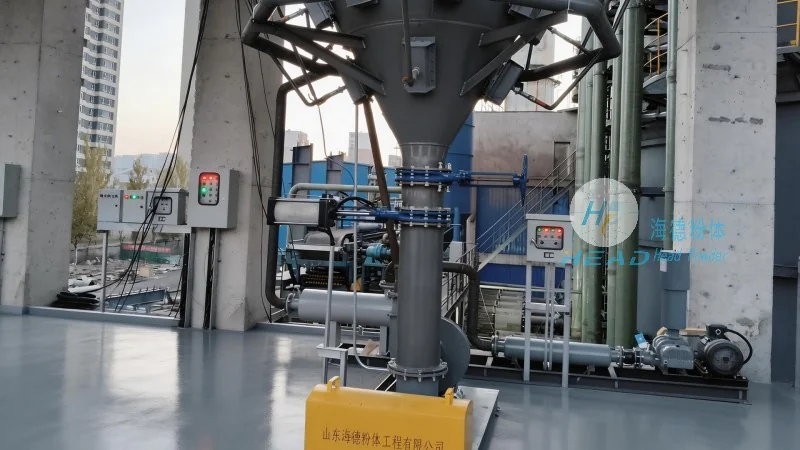
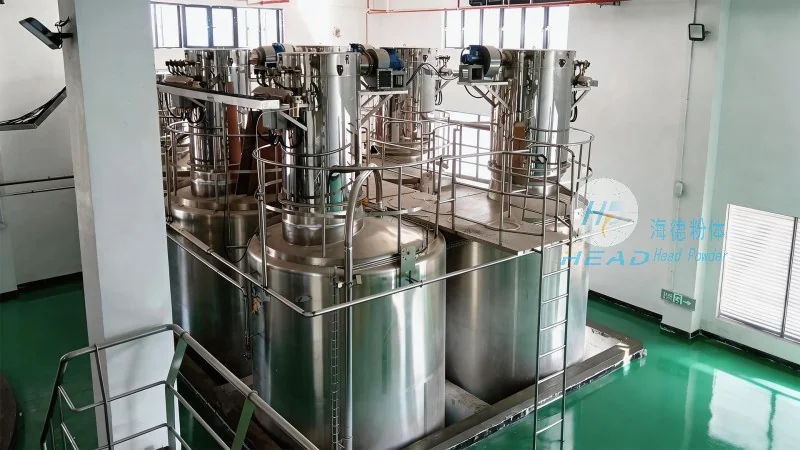
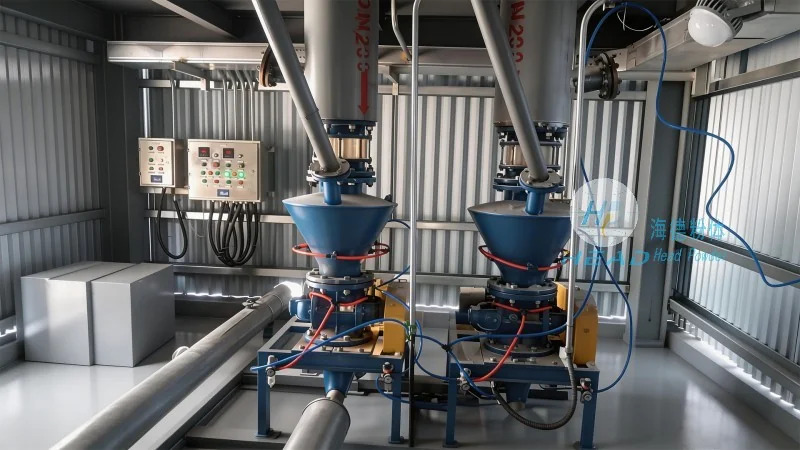
The automatic tonne bag feeding powder material conveyor operates on a principle that integrates advanced automation and mechanical engineering to facilitate the seamless transfer of bulk powders from tonne bags into processing lines. The system's core components include a robust hopper designed to accommodate the weight and dimensions of tonne bags, a precision discharge mechanism that regulates the flow of powder, and an automated bag handling unit that manages the opening, filling, and sealing of the bag. The process begins when a tonne bag is placed into the hopper; the system uses sensors to detect the bag's presence and triggers the feeding sequence. The bag is then opened via an automated cutting or tearing mechanism, allowing the powder to flow into the hopper. The discharge mechanism, often a rotary airlock valve or a star feeder, controls the flow rate by adjusting the speed of rotation, ensuring that the powder is delivered at a consistent rate to downstream equipment. This automated approach eliminates the need for manual intervention, reducing the risk of material spillage, contamination, and operator exposure to dust. The system also includes a dust collection system to capture any airborne particles, maintaining a clean and safe working environment.
Working Scene Characteristics of the Conveyor
The automatic tonne bag feeding powder material conveyor is particularly suited for industrial applications where large volumes of powder need to be handled efficiently and safely. Common working scenes include pharmaceutical manufacturing, food processing, chemical production, and mining operations. In pharmaceutical factories, for example, the conveyor ensures that raw materials are transferred under sterile conditions, minimizing the risk of cross-contamination. In food processing plants, the system maintains hygiene standards by preventing dust and particles from entering the environment. In chemical plants, the conveyor handles various powders, such as catalysts or reagents, with precision to avoid over or under-dosing. The versatility of the conveyor makes it adaptable to different industries and applications, providing a reliable solution for bulk powder handling.
Key Advantages in Working Scenarios
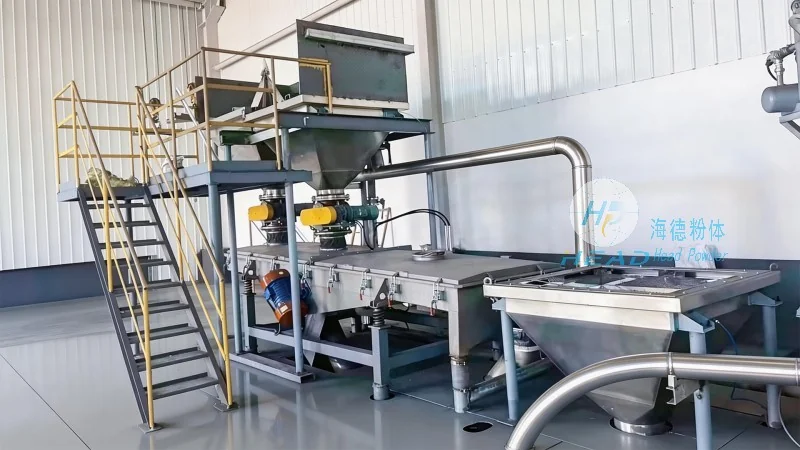
In various working scenarios, the automatic tonne bag feeding powder material conveyor offers several advantages that enhance operational performance. Firstly, the automated process reduces labor costs and minimizes human error, leading to more consistent and reliable material transfer. Secondly, the system is designed to handle different types of powders, including fine, coarse, and sticky materials, ensuring adaptability across diverse applications. Thirdly, the conveyor is equipped with safety features, such as dust collection systems and emergency stop buttons, to protect operators and maintain a safe working environment. These features are particularly important in industries where safety and compliance are critical. Additionally, the conveyor can be integrated with other processing equipment, such as mixers or reactors, to create a seamless production line, further improving overall efficiency.