With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Magnesium sulfate heptahydrate, a chemical compound with the formula MgSO₄·7H₂O, is widely utilized in industries such as pharmaceuticals, food processing, and agriculture. The efficient transportation of this material from storage to processing units is essential for maintaining production continuity and product quality. Pneumatic conveying systems have become a preferred method for handling such powders due to their ability to transport materials in a closed, dust-free environment. This article delves into the fundamental principles of a magnesium sulfate heptahydrate pneumatic conveying system and highlights the key working scene characteristics that define its operational effectiveness.
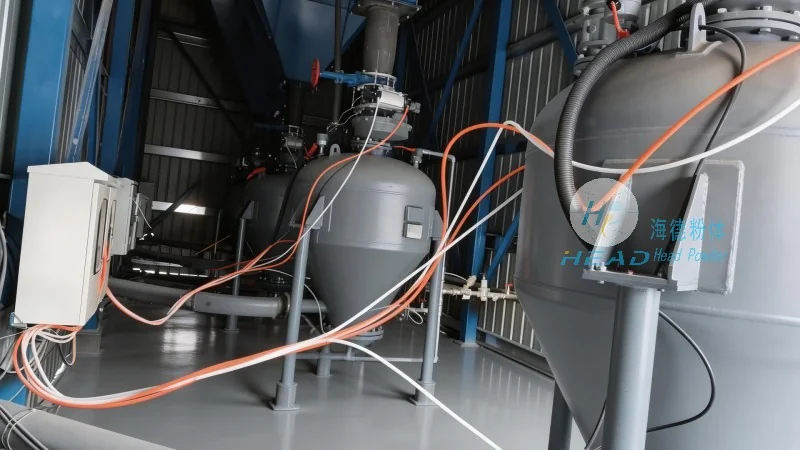
The operation of a pneumatic conveying system relies on the fundamental principle of using air or gas to transport solid materials through a pipeline. In the context of magnesium sulfate heptahydrate, the process begins with the material being introduced into a hopper or feeder. The material is then drawn into a pipeline where it is entrained by a high-velocity air stream generated by a blower or compressor. The air creates a pressure differential that propels the material forward, allowing it to be transported over considerable distances. The system may employ different conveying modes, including dilute phase and dense phase, depending on the material's properties and the required transport distance. Dilute phase conveying uses lower air velocities and higher material concentrations, while dense phase conveying utilizes higher air pressures and lower material concentrations to achieve more controlled and gentle transport. This flexibility allows the system to handle varying material characteristics and operational needs. The system also incorporates components like cyclones, filters, and dust collectors to separate the material from the air stream, ensuring that the material is delivered to its destination without contamination or loss.
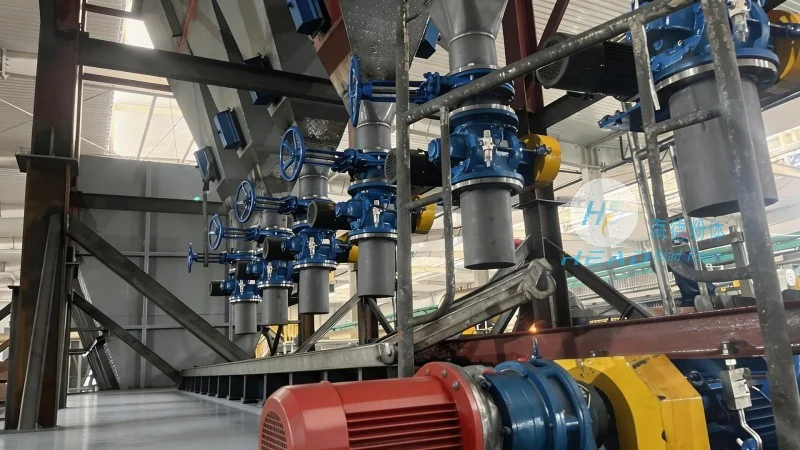
The working scene characteristics of a magnesium sulfate heptahydrate pneumatic conveying system are tailored to specific industrial environments where the material is processed. These systems are commonly found in pharmaceutical manufacturing facilities, where the material is used as an excipient or active ingredient. The key characteristics include the ability to handle fine powders without causing excessive wear on the system components, as magnesium sulfate heptahydrate is relatively abrasive but manageable with appropriate equipment. The system's design also considers the material's hygroscopic nature, ensuring that the conveying process does not lead to moisture absorption or caking, which could affect material flow and system performance. Additionally, the system is often integrated with automated control systems to monitor flow rates, pressure, and material levels, enhancing operational stability and reducing downtime. The working scene may involve multiple stages of material handling, such as from bulk storage to intermediate processing units, and the system's flexibility allows it to adapt to varying production demands. The use of a pneumatic conveying system in these scenarios provides a clean, dust-free environment, which is critical for maintaining product purity and compliance with industry regulations. The system's efficiency in handling the material also contributes to cost savings by minimizing material loss and reducing the need for manual handling, which can be hazardous in some applications.
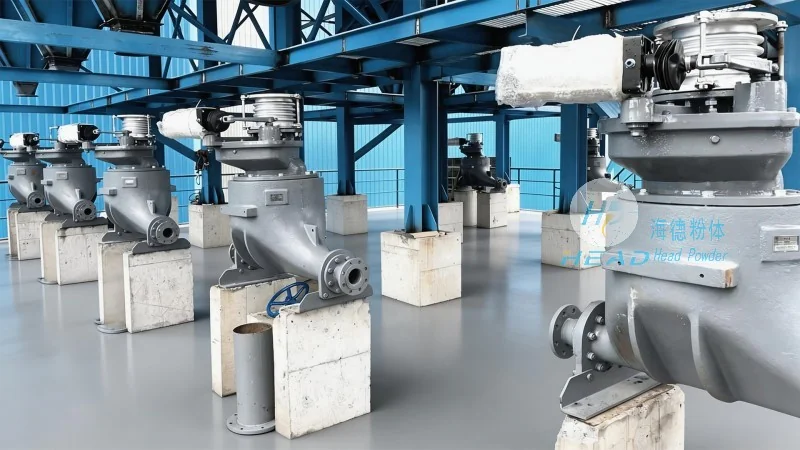
Shandong HeadPowder Engineering Co., Ltd., a leading engineering company specializing in material handling solutions, provides comprehensive support for the design, installation, and maintenance of magnesium sulfate heptahydrate pneumatic conveying systems. The company's expertise in industrial engineering ensures that the systems are optimized for efficiency, reliability, and safety. HeadPowder's team of engineers and technicians work closely with clients to understand their specific material handling needs and develop tailored solutions that meet industry standards. The company's facilities are located in Shandong, China, where it leverages local resources and expertise to deliver high-performance systems. HeadPowder offers a range of services, including system design, equipment supply, installation, and ongoing technical support. By partnering with HeadPowder, industries can enhance their material handling processes, reduce operational costs, and improve overall production efficiency. The company's commitment to quality and customer satisfaction ensures that clients receive systems that are not only effective but also durable and easy to maintain. With a focus on innovation and customer-centric solutions, HeadPowder continues to be a trusted provider of pneumatic conveying systems for magnesium sulfate heptahydrate and other industrial materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top