With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for pharmaceutical applications. These systems are engineered to meet stringent industry standards, ensuring safe and efficient material handling within pharmaceutical manufacturing environments.
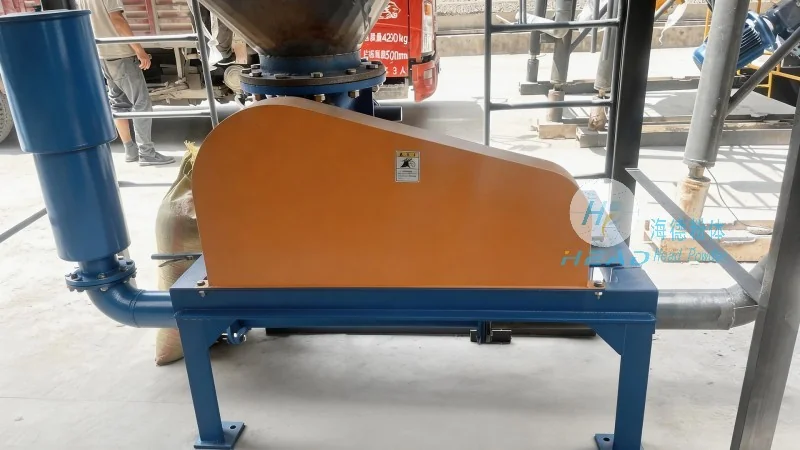
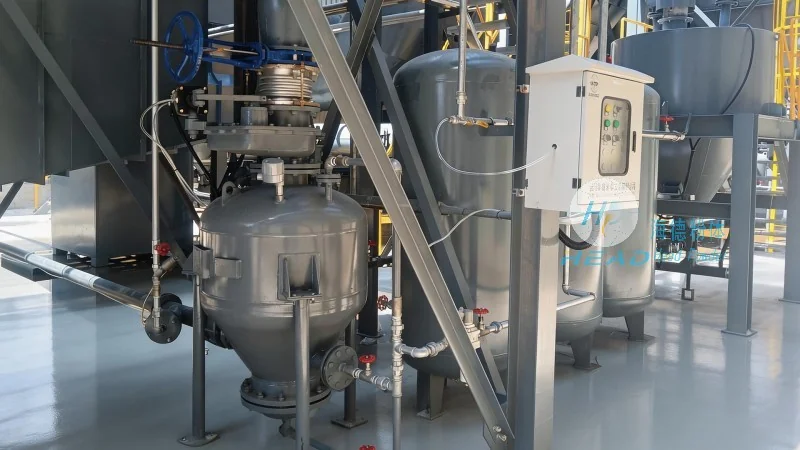
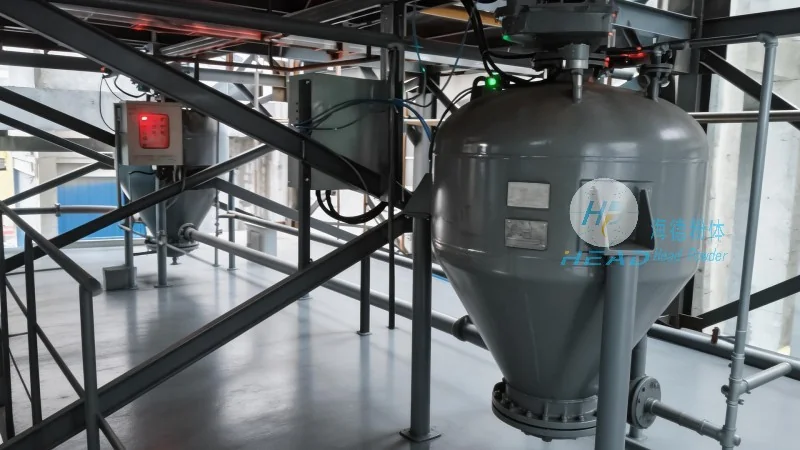
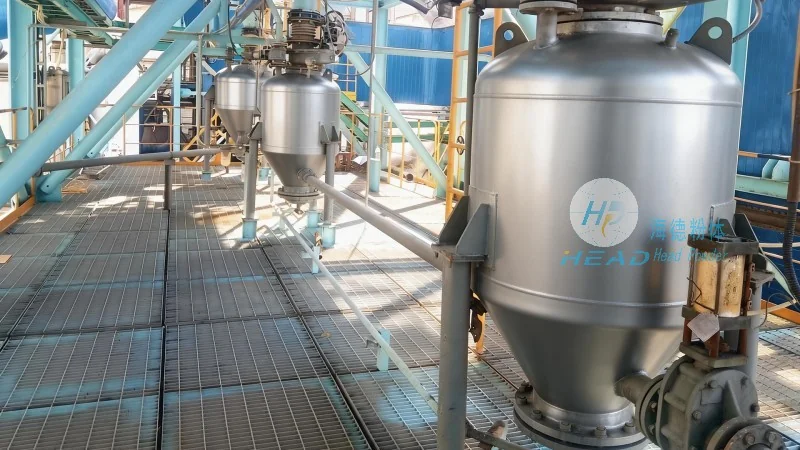
The core mechanism of a pharmaceutical material pneumatic conveying system involves the use of air or gas to transport bulk materials through a closed pipeline network. The system typically operates under either positive pressure (pressure conveying) or negative pressure (vacuum conveying), depending on the specific requirements of the material being handled and the system layout. In positive pressure systems, a blower or compressor generates compressed air that propels the material forward through the pipeline. The material is often introduced into the system via a feeder, such as a rotary valve or a star feeder, which controls the flow rate and ensures consistent material feeding. As the material travels through the pipeline, it is mixed with the air stream, forming a dense or dilute phase flow, depending on the system design. The conveying line may include components like bends, expansion joints, and filters to maintain system integrity and prevent material deposition or blockages. At the destination point, a separator or cyclone separates the material from the air stream, allowing the material to be discharged into a collection vessel or processing equipment. The air, now filtered to remove any residual particles, is either recirculated back into the system or vented to the atmosphere, depending on the system configuration.
Pharmaceutical material pneumatic conveying systems from HeadPowder are characterized by several critical features that enhance their performance and suitability for pharmaceutical applications. Firstly, they are designed with a focus on hygiene and compliance with GMP (Good Manufacturing Practice) standards. The components, including the feeder, pipeline, and separator, are constructed from materials such as stainless steel, which are easy to clean and sanitize, minimizing the risk of contamination. The system's design also incorporates features like smooth internal surfaces and minimal dead zones to prevent material accumulation and ensure thorough cleaning. Secondly, these systems offer high efficiency and flexibility in material handling. They can transport a wide range of pharmaceutical materials, including powders, granules, and bulk solids, with minimal product degradation. The adjustable flow rates and pressure settings allow for precise control over the conveying process, adapting to varying production demands. Thirdly, the systems are engineered for reliability and low maintenance. Advanced components, such as high-efficiency blowers and robust feeders, reduce the likelihood of system downtime. The use of durable materials and thoughtful design minimizes wear and tear, extending the system's operational life. Additionally, the systems are designed for easy integration into existing pharmaceutical production lines, with modular components that can be customized to fit specific facility layouts and material handling requirements. This flexibility ensures that the systems can be adapted to meet the evolving needs of pharmaceutical manufacturers without significant modifications to the overall production infrastructure.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top