With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications requiring the efficient and reliable transport of dry bulk materials, pneumatic conveying systems offer a robust solution. This article explores the working principle and key features of such systems, highlighting their importance in modern material handling processes.
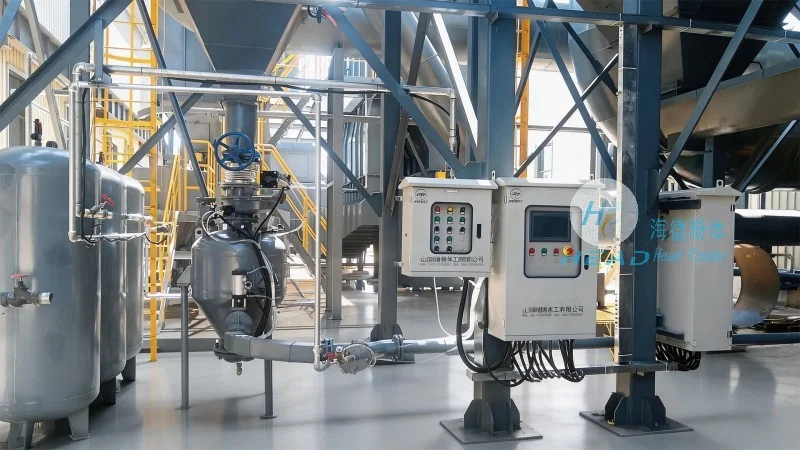
Pneumatic conveying systems operate by utilizing compressed air or other gases to transport dry bulk materials through a pipeline. The core mechanism involves creating a pressure differential between the inlet and outlet of the system. In an aspiration (or vacuum) system, a vacuum is created at the material source, drawing the dry powder into the pipeline. Conversely, pressure (or blow) systems use compressed air to push the material forward. The choice between these systems depends on factors like material characteristics, distance, and system layout. The process typically involves a hopper or feeder that feeds the dry material into the pipeline, where it is mixed with the conveying air. The mixture travels through the pipeline to the destination, where it is separated from the air—often via a cyclone separator or filter—and the material is discharged. The air is then either recycled or vented, depending on the system design. This method allows for continuous, closed-loop operation, minimizing material exposure to the environment and reducing the risk of contamination.
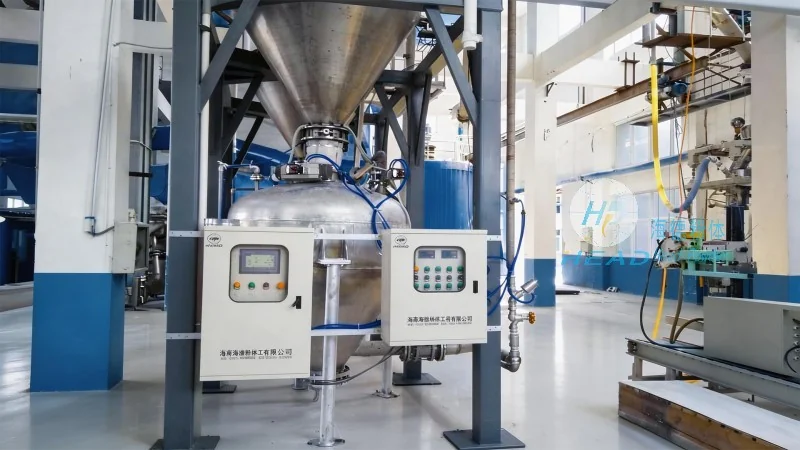
Dry bulk material pneumatic conveying systems are characterized by several advantages that make them suitable for diverse industrial applications. One of the primary features is high efficiency in material transport, as they can move large volumes of dry powder over significant distances with minimal energy consumption compared to traditional methods like belt conveyors or bucket elevators. The systems are also flexible and adaptable, capable of handling a wide range of dry materials—from fine powders to coarse granules—by adjusting the air pressure, flow rate, and pipeline design. This adaptability makes them ideal for industries such as pharmaceuticals, food processing, chemicals, and mining. Another critical feature is environmental friendliness, as the closed system design prevents dust emissions and contamination, aligning with regulatory standards and promoting a safer working environment. Additionally, these systems offer hygienic and clean operation, which is essential in industries where product purity is paramount, such as food and pharmaceutical manufacturing. The ability to integrate with existing production lines and scale up or down based on demand further enhances their practicality. Furthermore, the systems provide low maintenance requirements compared to mechanical conveyors, as they have fewer moving parts and are less prone to wear and tear from abrasive materials. This reduces downtime and operational costs over the system's lifespan.
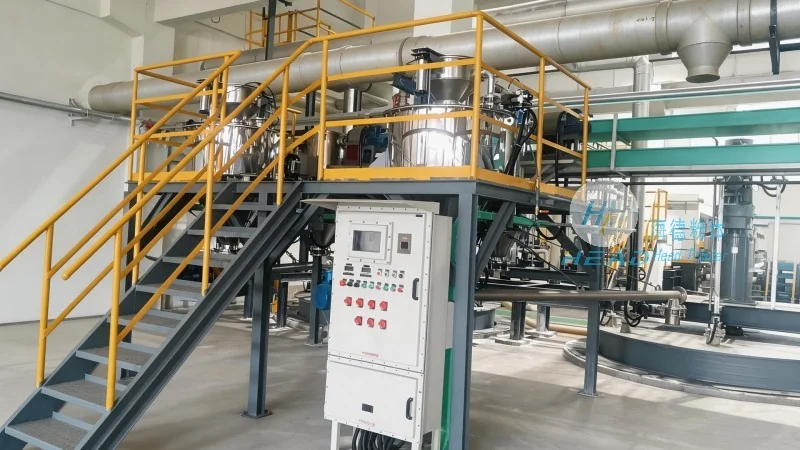
The versatility of dry bulk material pneumatic conveying systems makes them indispensable in various sectors. In the pharmaceutical industry, they are used to transport active pharmaceutical ingredients (APIs) and excipients with strict purity requirements, ensuring that the materials remain free from contamination during transport. The food processing sector relies on these systems for handling powders like flour, sugar, and spices, maintaining hygiene standards and preventing cross-contamination. The chemical industry utilizes pneumatic conveyors to move bulk chemicals, including powders and granules, in manufacturing processes, enhancing safety by containing dust and fumes. In the mining and minerals sector, these systems are employed to transport raw materials like coal, ore, and sand, improving efficiency in processing plants. Even in the agricultural sector, pneumatic conveyors are used to move grain and other agricultural products from storage to processing facilities. The consistent performance and reliability of these systems across these industries underscore their importance in modern material handling.
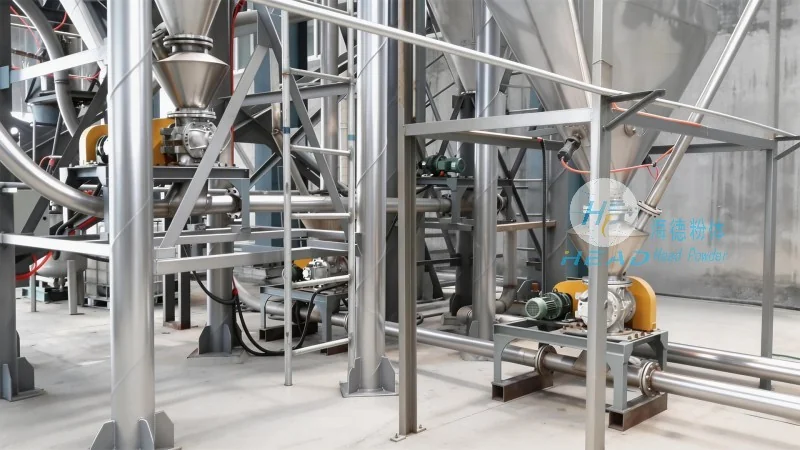
Overall, dry bulk material pneumatic conveying systems represent a sophisticated solution for the efficient and safe transport of dry powders. Their working principle, based on air pressure and vacuum, enables continuous, closed-loop operation, while their key features—such as efficiency, adaptability, and environmental friendliness—make them a preferred choice for many industries. As demand for reliable material handling solutions grows, the importance of these systems in maintaining productivity and compliance with industry standards remains high. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of clients. With a focus on innovation and quality, the company ensures that its systems meet the highest operational and safety standards, supporting clients in achieving their material handling goals effectively. Based in Shandong, China, HeadPowder Engineering Co., Ltd. leverages decades of experience to deliver solutions that enhance operational efficiency and reduce costs for businesses across various sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top