With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Pyrolysis carbon powder conveying systems are essential equipment in industrial processes that handle fine powders derived from pyrolysis processes. These systems are designed to efficiently transport carbonaceous powders, ensuring stable and reliable material handling. The following sections will explore the working principle and key features of such conveyors, providing insights into their operational mechanisms and benefits. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of high-quality pyrolysis carbon powder conveying equipment, catering to the diverse needs of industrial clients.
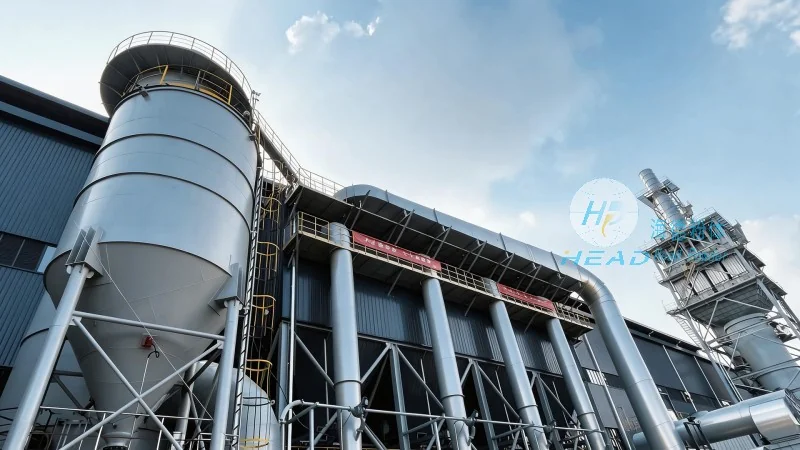
At the core of pyrolysis carbon powder conveyors is a mechanism that combines air flow and mechanical components to move fine powders. The process typically begins with the feeding of carbon powder into the conveyor system. A fan or blower generates a controlled airflow, which is directed through a pipeline or duct. The carbon powder is then entrained by the air stream and transported to the desired destination. This method, known as pneumatic conveying, is particularly effective for handling fine, dusty materials like pyrolysis carbon powder. The system ensures that the powder is moved without clogging or degradation, maintaining the quality of the material throughout the conveying process. The design of the conveyor, including the type of fan, pipeline diameter, and air velocity, is critical in determining the efficiency and capacity of the system. For instance, high-velocity air can handle larger quantities of powder but may increase energy consumption, while low-velocity systems are more energy-efficient but require larger ducts to maintain flow.
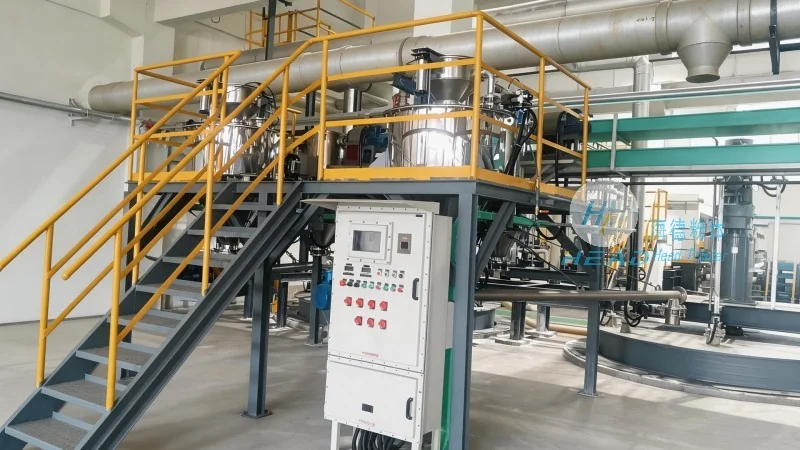
Pyrolysis carbon powder conveyors are equipped with several features that enhance their performance and usability. One of the primary features is the ability to handle fine, abrasive powders without causing wear or damage to the equipment. The materials used in the construction of the conveyor, such as stainless steel or special alloys, are chosen to resist corrosion and abrasion from the carbon powder. Another important feature is the system's ability to maintain a clean and dust-free environment. Many conveyors incorporate filtration and dust collection systems to prevent the release of fine particles into the air, ensuring compliance with environmental regulations and workplace safety standards. Additionally, these conveyors often include adjustable controls for air pressure and flow rate, allowing operators to optimize the conveying process based on the specific characteristics of the carbon powder being handled. This flexibility is crucial in industrial settings where the properties of the powder may vary. The design also includes safety features, such as pressure relief valves and emergency shut-off mechanisms, to prevent accidents and ensure safe operation. Furthermore, the conveyors are typically compact and easy to integrate into existing production lines, minimizing the need for extensive modifications to the facility.
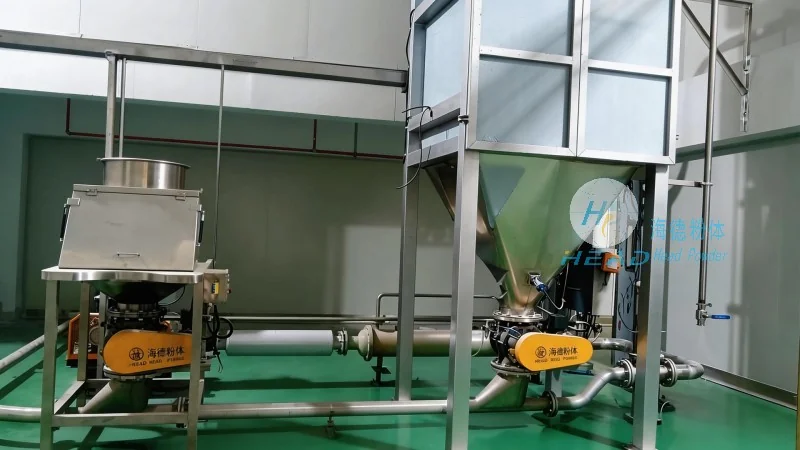
The use of pyrolysis carbon powder conveyors offers several benefits in industrial applications. These systems improve the efficiency of material handling by reducing the time and labor required to transport carbon powder. By automating the conveying process, they also enhance safety by minimizing human exposure to fine powders. The consistent and reliable transport of the powder ensures that downstream processes, such as processing or packaging, operate smoothly without interruptions. The conveyors are widely used in industries that produce pyrolysis carbon, including waste management, biomass processing, and chemical manufacturing. For example, in waste-to-energy facilities, pyrolysis carbon powder conveyors are used to transport the carbon residue from pyrolysis reactors to storage or further processing units. In biomass processing plants, they help move the carbon powder from pyrolysis units to combustion or gasification systems. The versatility of these conveyors makes them suitable for various applications, from small-scale laboratory operations to large-scale industrial production.
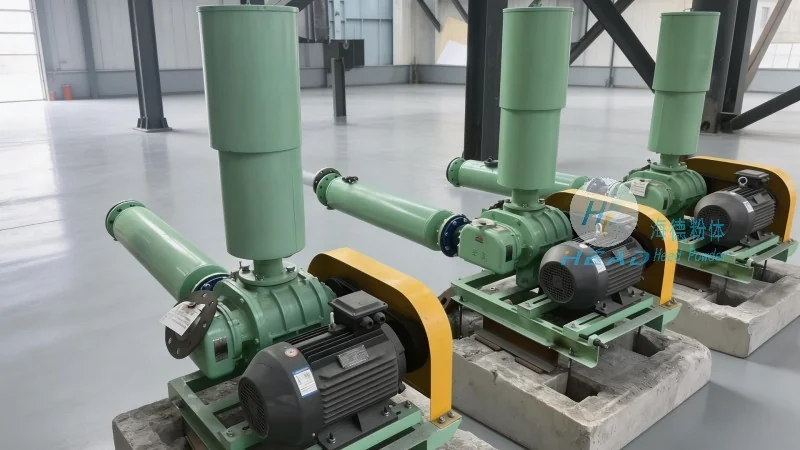
Pyrolysis carbon powder conveyors are sophisticated equipment that play a vital role in the efficient handling of fine carbon powders. Understanding their working principle and key features is essential for selecting the right system for specific industrial needs. The combination of pneumatic conveying technology with robust construction and advanced controls ensures that these conveyors provide reliable, safe, and efficient material transport. As industries continue to rely on pyrolysis processes for carbon production, the demand for high-quality conveying systems will remain strong. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd., based in China, is crucial in providing tailored solutions that meet the unique requirements of different applications, ensuring optimal performance and longevity of the equipment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top