

Working Principle and Features of Intelligent Weighing Pneumatic Conveying System Equipment
Intelligent weighing pneumatic conveying systems represent a sophisticated technology in material handling, combining precise weight measurement with efficient pneumatic transport. This article explores the core working principles and key features of such systems, highlighting their practical applications and technical advantages.
Introduction to Intelligent Weighing Pneumatic Conveying Systems
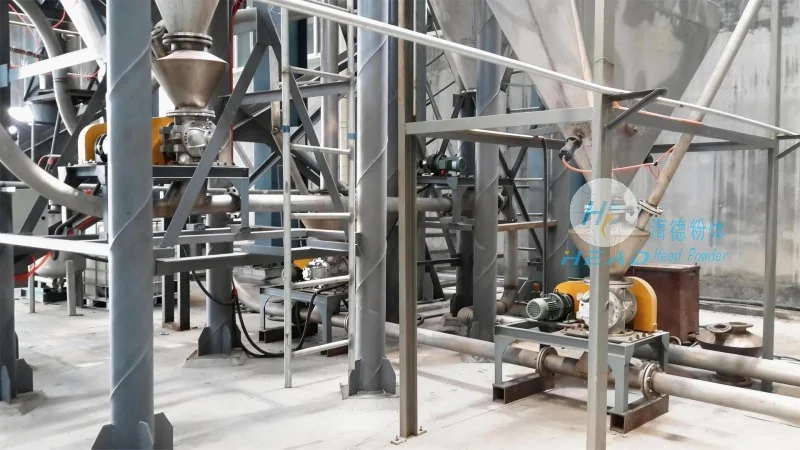
Developed and manufactured by Shandong HeadPowder Engineering Co., Ltd., an intelligent weighing pneumatic conveying system integrates advanced technology to optimize material handling processes. The system is designed to transport bulk materials through an enclosed pipeline using compressed air or other gas streams, while simultaneously providing accurate weight measurement at various points in the process. This dual functionality makes it ideal for industries requiring both material transport and real-time inventory tracking.
Key Components and Their Roles
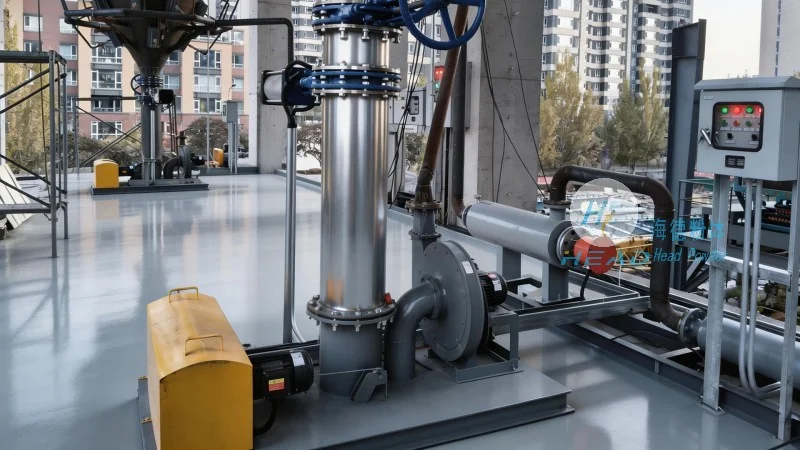
The intelligent weighing pneumatic conveying system typically consists of several critical components, each playing a vital role in the overall operation. These include the material feed hopper, which holds the bulk material; the conveying pipeline, which transports the material; the weighing hopper or scale, which measures the material mass; and the control unit, which manages the entire process. Additionally, the system may incorporate air compressors, filters, and valves to regulate airflow and ensure smooth operation.
Working Principle of the System
The operation of an intelligent weighing pneumatic conveying system follows a systematic sequence. Initially, bulk material is fed into the material hopper. When the system is activated, compressed air is introduced into the conveying pipeline, creating a flow that draws the material from the hopper into the pipeline. As the material travels through the pipeline, it passes through the weighing hopper, where sensors accurately measure the mass of the material being conveyed. The control unit processes this data and adjusts the airflow or feeding rate as needed to maintain consistent material flow and weight accuracy. This closed-loop control ensures stable and reliable operation, minimizing material loss and optimizing process efficiency.
Core Features and Technical Advantages
Intelligent weighing pneumatic conveying systems are distinguished by several key features that enhance their performance and usability. One of the primary advantages is the ability to provide real-time weight measurement, enabling precise inventory management and process control. This feature is particularly valuable in industries such as pharmaceuticals, food processing, and chemical manufacturing, where product purity and consistency are paramount. Another notable feature is the system's ability to handle a wide range of materials, from fine powders to granules, with minimal degradation or segregation. The enclosed pipeline design also helps maintain material integrity and prevents contamination, which is critical for products with strict quality standards.
Application Scenarios and Industry Impact
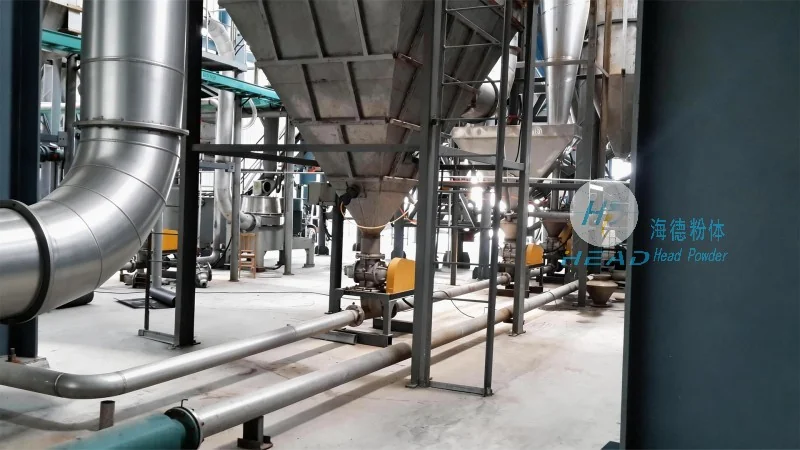
The versatility of intelligent weighing pneumatic conveying systems makes them suitable for a variety of industrial applications. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring accurate dosing and batch consistency. In the food processing sector, they are employed to handle ingredients like flour, sugar, and spices, maintaining hygiene and preventing cross-contamination. Similarly, in the chemical industry, they facilitate the transport of powders and granules while providing accurate weight data for quality control. The ability to integrate with other automation systems further enhances their utility, allowing for seamless integration into existing production lines.
Conclusion
Intelligent weighing pneumatic conveying systems represent a significant advancement in material handling technology, offering a combination of precision, efficiency, and reliability. By integrating advanced weighing technology with pneumatic conveying mechanisms, these systems address the challenges of material transport and inventory management in modern industrial settings. As industries continue to demand higher standards of quality and efficiency, the adoption of such systems is likely to increase, driving further innovation in material handling solutions.