With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding coke material handling equipment is crucial for industries that rely on efficient and reliable transport of coke, a key product in steel production. This equipment is designed to move coke from production sites to processing facilities or storage areas with precision and minimal loss. The design principles behind these systems are rooted in engineering efficiency, safety, and adaptability to the unique characteristics of coke, such as its density, size, and tendency to generate dust.
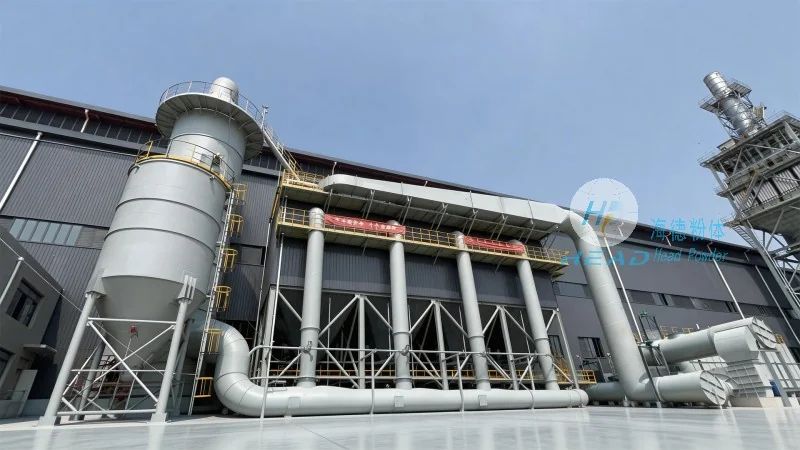
Coke material handling equipment is a specialized category of machinery used in the coke production and steel manufacturing sectors. Its primary function is to transport coke, which is a porous, hard, and carbon-rich material, from the coke oven to various processing stages or storage locations. These systems are integral to maintaining the flow of operations in coke plants, ensuring that coke is moved safely and efficiently without compromising quality or causing environmental issues like dust pollution.
HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the design, manufacturing, and installation of coke material handling equipment. With a strong presence in Shandong, China, the company has built a reputation for delivering high-quality solutions tailored to the specific needs of coke production facilities. HeadPowder's expertise lies in understanding the unique challenges of coke handling, such as its abrasive nature and the need for dust control, and developing equipment that addresses these challenges effectively.
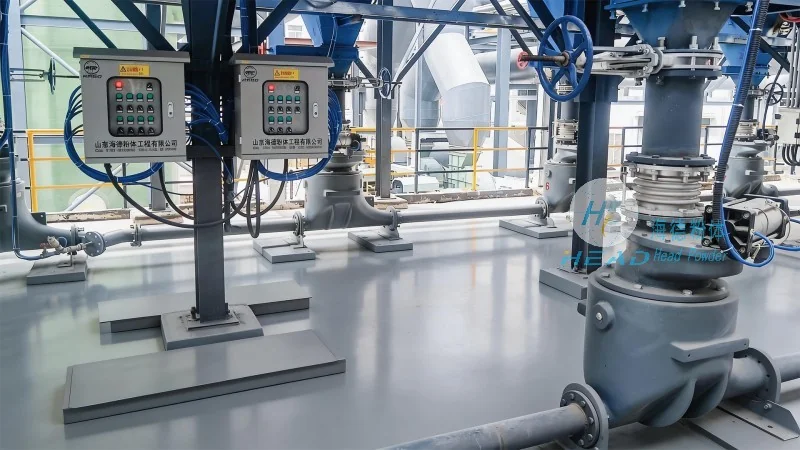
The design of coke material handling equipment is guided by several key principles aimed at optimizing performance and ensuring safety. First, structural integrity is paramount, as coke is a heavy and abrasive material that can cause wear on machinery. Equipment is typically constructed from durable materials like steel, with components designed to withstand the constant impact and friction associated with coke transport. Second, the system is engineered for efficiency, minimizing energy consumption and maximizing throughput. This involves optimizing the speed and capacity of conveyor systems, ensuring that coke is moved in a continuous and unbroken flow. Third, safety and environmental considerations are integrated into the design. Features such as dust suppression systems, enclosed conveyor belts, and proper ventilation are included to protect workers and comply with environmental regulations. Additionally, the design takes into account the need for easy maintenance and accessibility, allowing for quick repairs and adjustments without disrupting production.
Modern coke material handling equipment consists of several key components, each playing a critical role in the overall operation. The primary components include feeders, conveyors, elevators, and storage silos. Feeders are used to control the flow of coke from the source, ensuring a consistent and controlled feed to the conveyor system. Conveyors, often in the form of belt conveyors or chain conveyors, are responsible for transporting coke horizontally or at an incline. Elevators, such as bucket elevators or screw conveyors, are used to lift coke vertically, moving it from lower to higher levels within the facility. Storage silos are used to store large quantities of coke, providing a buffer for production and ensuring a steady supply of material.
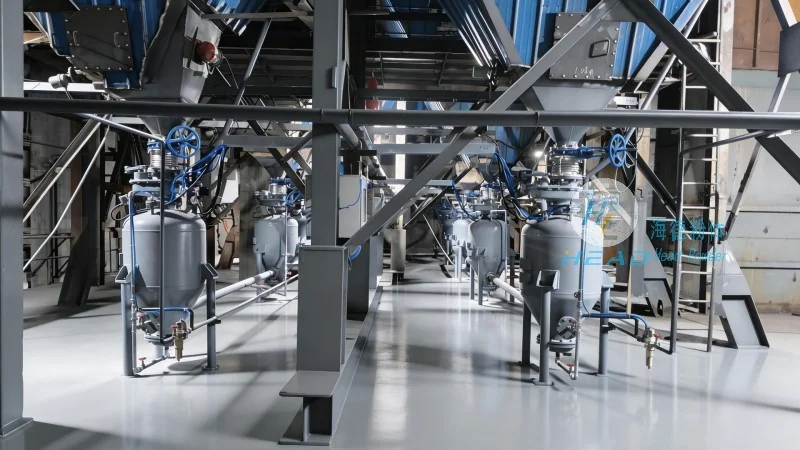
Implementing advanced coke material handling equipment offers numerous advantages for coke production facilities. One of the most significant benefits is improved efficiency, as these systems can handle large volumes of coke with minimal downtime. This leads to increased production capacity and reduced operational costs. Another advantage is enhanced safety, as the equipment is designed with features that minimize the risk of accidents, such as enclosed conveyor systems and dust control measures. Additionally, advanced systems often include automation and monitoring capabilities, allowing for real-time tracking of the coke flow and early detection of potential issues. This proactive approach helps prevent equipment failures and ensures the smooth operation of the entire production process.
In conclusion, coke material handling equipment is a vital component of modern coke production facilities, and its design principles are centered on efficiency, safety, and durability. Companies like HeadPowder Engineering Co., Ltd. play a crucial role in providing these specialized systems, leveraging their expertise to meet the unique demands of the coke industry. By understanding the design principles and key components of these systems, coke plants can optimize their operations, improve safety, and reduce costs, ultimately contributing to the overall success of their business.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top