With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
In the rapidly evolving industrial landscape of East Africa, the demand for efficient and reliable material handling systems has reached unprecedented levels. A prime example of this technological advancement is the recent chemical and mineral powder pneumatic conveying project successfully executed in Nairobi, Kenya. This project represents a significant milestone in the region's infrastructure development, showcasing the capability to handle difficult bulk materials with precision and safety. The initiative was spearheaded by a leading engineering firm dedicated to providing top-tier pneumatic conveying solutions to the international market. By implementing state-of-the-art technology, the project has set a new benchmark for material transfer in the African continent, ensuring that industrial operations can continue seamlessly without the risks associated with traditional handling methods.
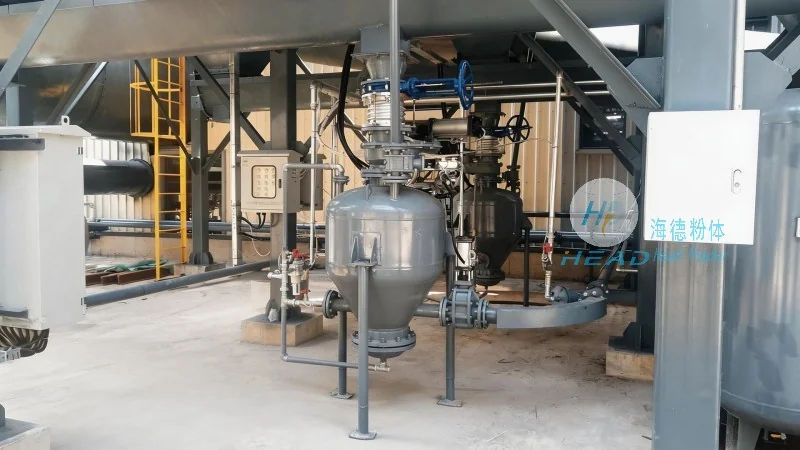
Chemical and mineral powders present unique challenges in industrial settings. These materials are often fine, dusty, and chemically reactive, requiring specialized handling equipment to prevent contamination, environmental hazards, and operational inefficiencies. In the context of the Nairobi project, the primary objective was to transport these powders over significant distances within a complex facility. The traditional methods of manual handling or belt conveyors were deemed insufficient due to the high risk of dust leakage and the potential for material degradation during transport. The solution required a system that could maintain the integrity of the chemical and mineral powders while ensuring the safety of the workforce and the surrounding environment.
To address these challenges, the project utilized a robust pneumatic conveying system designed to transport dry bulk materials using pressurized air or vacuum. This technology is widely recognized as one of the most effective methods for moving powders and granules. The system operates by creating a pressure differential that moves the material through a closed pipeline from the source to the destination. This closed-loop system is crucial for preventing dust emissions, which is a major concern when handling fine chemical powders. Furthermore, the pneumatic conveying system significantly reduces the need for manual intervention, thereby lowering labor costs and minimizing the risk of occupational health issues related to dust inhalation.
This Nairobi installation stands out as a definitive pneumatic conveying case in the African market. It demonstrates how advanced engineering can be adapted to local conditions while maintaining global standards of quality and efficiency. The project involved the installation of specialized vacuum or pressure vessels, depending on the specific requirements of the chemical and mineral powders being processed. The engineering team focused on optimizing the system parameters, such as air velocity and pressure, to ensure that the material flowed smoothly without clogging or causing pipeline erosion. The successful deployment of this system in Nairobi highlights the growing trend of adopting sophisticated material handling solutions across the African continent.
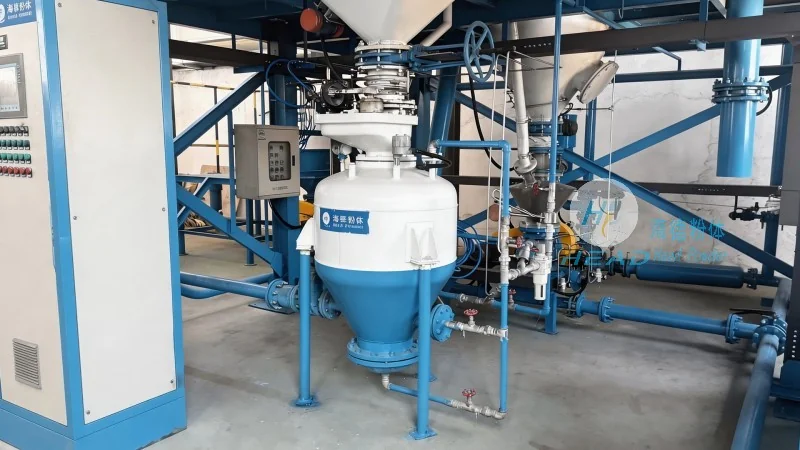
The African market presents unique logistical and environmental challenges, including high temperatures, varying humidity levels, and infrastructure constraints. The Nairobi project specifically required a solution that could withstand these conditions and provide reliable performance year-round. The pneumatic conveying system installed in this project was engineered with durability and ease of maintenance in mind. This adaptability is a key factor in the success of African pneumatic conveying projects. By providing a system that can operate efficiently in diverse climates and industrial settings, the engineering firm has solidified its reputation as a trusted partner for industrial automation in the region.
Focus on the Nairobi pneumatic conveying aspect, this project was tailored to meet the specific throughput requirements of the client's chemical processing plant. The system was designed to handle large volumes of mineral powder, ensuring that the production line never experienced downtime due to material shortages. The engineering team conducted extensive simulations and on-site assessments to determine the optimal pipeline layout and equipment specifications. The result was a highly efficient system that not only met but exceeded the client's expectations regarding throughput and reliability. This project serves as a testament to the technical expertise available in the field of bulk material handling.
The successful execution of the Nairobi project is a result of the comprehensive engineering capabilities of Shandong Headpowder Engineering Co., Ltd.. Based in Shandong, China, the company has established itself as a premier manufacturer and engineering service provider in the field of pneumatic conveying. With years of experience in the industry, the company has developed a deep understanding of the mechanics of powder handling and the specific needs of various industrial sectors. Their team of engineers and technicians are dedicated to delivering customized solutions that address the unique challenges of each project, whether it is located in Asia, Africa, or beyond.
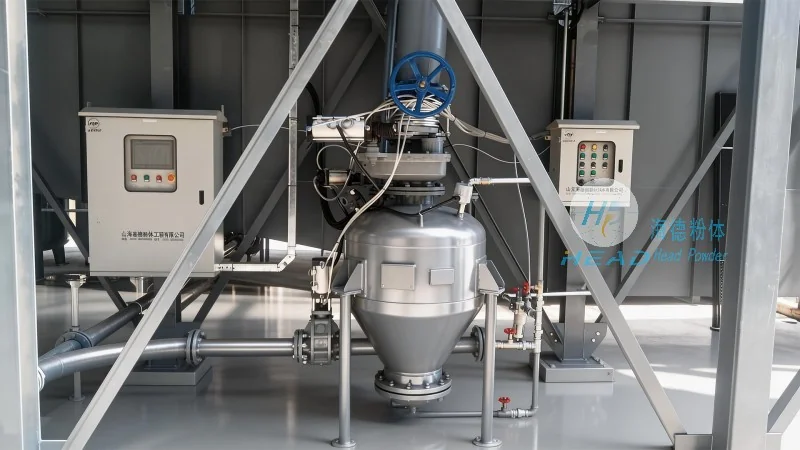
As a company based in Shandong, Shandong Headpowder Engineering Co., Ltd. leverages its strategic location and access to advanced manufacturing technologies to produce high-quality pneumatic conveying equipment. The company’s expertise extends beyond manufacturing; they offer complete turnkey solutions, including design, installation, and commissioning. The Nairobi project is a clear example of their global reach, where their engineering prowess was applied to a complex industrial challenge in East Africa. By combining global engineering standards with local market knowledge, the company ensures that every project is a success.
The completion of the chemical and mineral powder pneumatic conveying project in Nairobi marks a significant achievement for all stakeholders involved. It provides a safe, efficient, and environmentally friendly method for handling bulk materials, contributing to the overall productivity of the industrial facility. This case reinforces the value of investing in modern pneumatic conveying technology for chemical and mineral processing. The system not only improves operational efficiency but also enhances workplace safety and environmental compliance.
For those interested in learning more about this successful implementation or exploring similar solutions for their own facilities, direct communication with the project engineers is recommended. The project team is available to discuss technical specifications and project requirements. Interested parties are encouraged to contact Mr. Zhang, the project manager, for detailed consultations. You can reach the team via WeChat at 15662777102 to discuss how pneumatic conveying technology can be integrated into your specific industrial processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top