With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Bin pump pneumatic conveying equipment is a specialized system used in industrial settings to transport bulk materials through a pipeline network using air pressure. This technology is widely adopted across various industries due to its efficiency, flexibility, and ability to handle a wide range of materials, from powders to granules. The equipment operates by using a bin pump, which acts as a pressure vessel to store and discharge material under controlled conditions. The design principles behind this equipment are centered on creating a reliable and efficient method for material transfer, ensuring minimal product degradation and operational safety.
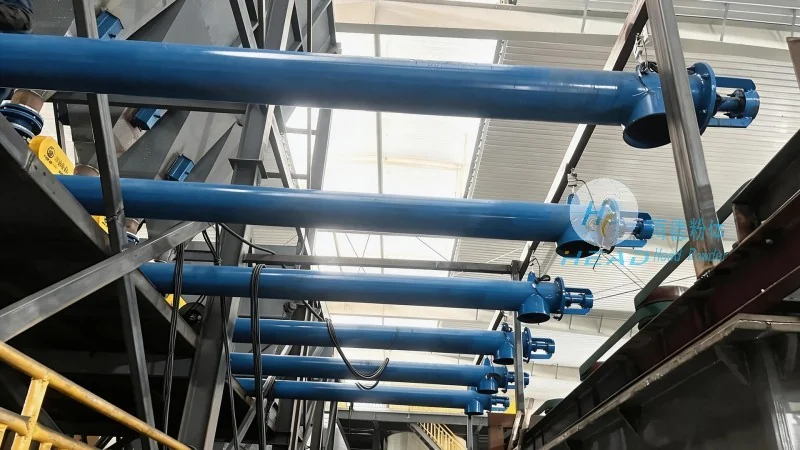
The bin pump, often referred to as a pressure bin or surge bin, is the central component of the system. It is designed to hold bulk materials and provide a consistent flow to the conveying line. The pump typically consists of a hopper, a discharge valve, and a pressure control mechanism. The hopper is where the material is stored, and the discharge valve regulates the flow of material into the pipeline. The pressure control system maintains the necessary air pressure to ensure smooth material transport. Other key components include the conveying line, which can be made of metal or plastic, and the air compressor or blower that generates the air pressure needed for operation. These components work together to create a closed-loop system that can handle both positive and negative pressure conveying, depending on the application requirements.
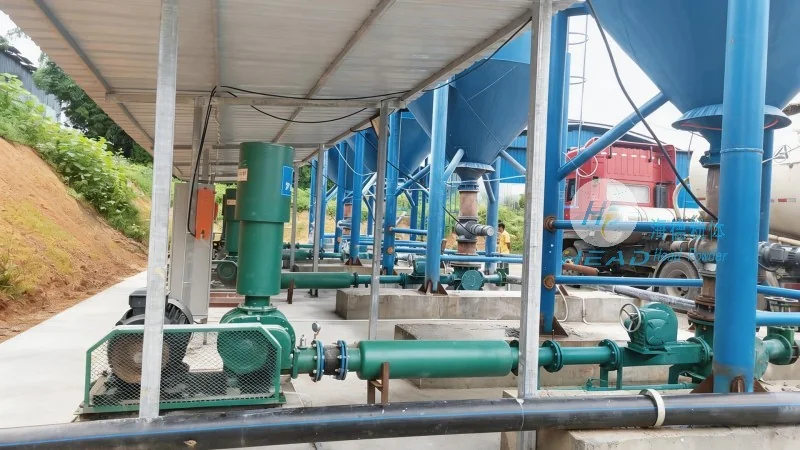
The design of bin pump pneumatic conveying equipment focuses on several critical principles to ensure optimal performance. First, the system must maintain consistent material flow, which is crucial for preventing blockages and ensuring continuous operation. This is achieved through the use of a pressure bin that can store a sufficient amount of material to sustain the conveying process. Second, the equipment must be designed to handle a variety of materials, including those that are abrasive, corrosive, or prone to bridging or caking. The bin pump's construction, often made from stainless steel or other durable materials, helps mitigate issues related to material degradation and equipment wear. Third, the system must prioritize safety and operational reliability. This includes features such as pressure relief valves, material flow indicators, and automatic shut-off mechanisms to prevent accidents and equipment damage. Additionally, the design considers energy efficiency, with the air compressor or blower sized appropriately to minimize power consumption while maintaining sufficient pressure for material transport.
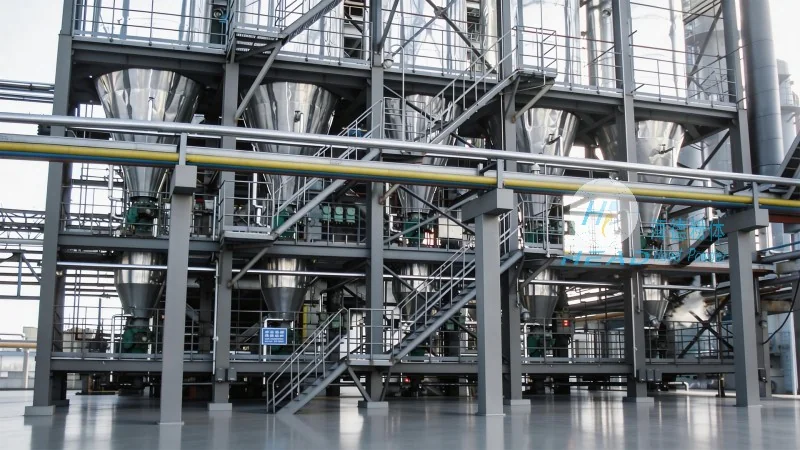
Bin pump pneumatic conveying equipment is utilized in numerous industrial applications, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, for example, the equipment is used to transport powders and granules while maintaining strict hygiene standards. The enclosed system prevents contamination and ensures product purity. In food processing, the equipment is ideal for handling ingredients like flour, sugar, and spices, as it maintains product quality and prevents cross-contamination. The benefits of using this technology extend beyond material handling efficiency. The system reduces labor costs by automating the material transfer process and minimizes product loss due to spillage or degradation. Furthermore, the flexibility of the system allows for easy integration into existing production lines, adapting to changes in production volume or material types without significant modifications. The design also allows for remote monitoring and control, enhancing operational management and reducing downtime.
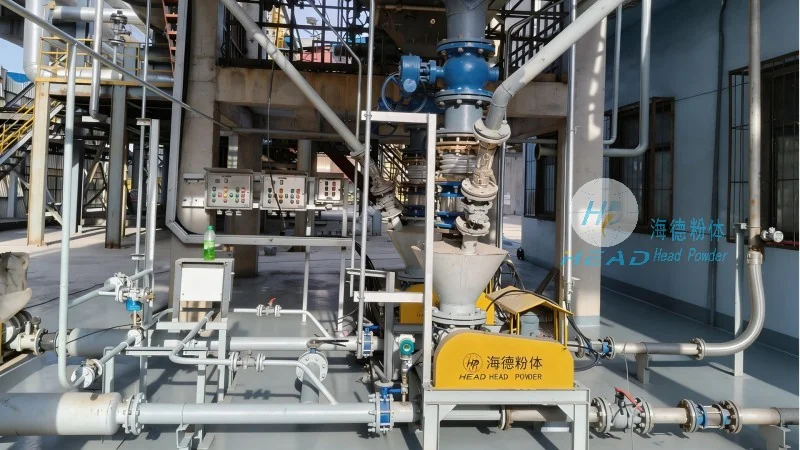
Bin pump pneumatic conveying equipment plays a vital role in modern industrial operations by providing an efficient, reliable, and safe method for bulk material transport. The design principles, centered on consistent flow, material compatibility, and operational safety, ensure that the equipment meets the demands of various industries. As manufacturing processes continue to evolve, the importance of such equipment in optimizing material handling and improving overall productivity cannot be overstated. The technology's adaptability and efficiency make it a preferred choice for companies seeking to enhance their production capabilities while maintaining high standards of quality and safety. With proper design and maintenance, bin pump pneumatic conveying systems can provide long-term value and reliability in industrial settings.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top