With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. One of their key areas of expertise is the application of pneumatic conveying systems for the efficient transport of bulk brown sugar. This technology offers a reliable and cost-effective method for moving large volumes of sugar cane molasses or brown sugar from storage to processing facilities, or between different stages of production.
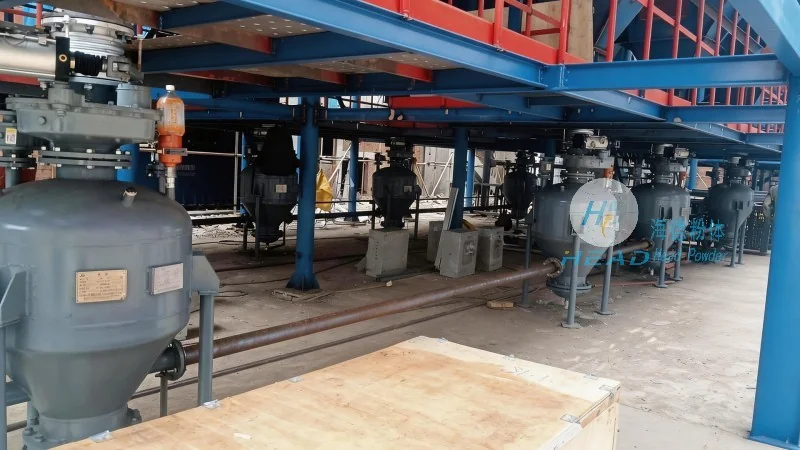
Pneumatic conveying uses compressed air or gas to transport dry bulk materials like brown sugar through a network of pipes. The system typically consists of a hopper, a conveyor line, and a receiver. As the brown sugar is fed into the hopper, it is drawn into the conveyor line by the airflow, moving it to the desired destination. This method eliminates the need for mechanical components such as belts or buckets, reducing maintenance requirements and minimizing the risk of material contamination.
Implementing pneumatic conveying for bulk brown sugar offers several advantages. First, it provides a dust-free and hygienic environment, which is crucial for maintaining the quality of brown sugar, especially in food processing applications. The enclosed system prevents the sugar from coming into contact with external contaminants, ensuring compliance with food safety standards. Second, the technology allows for high-speed and continuous material transport, improving overall production efficiency. Unlike traditional methods that may involve manual handling or conveyor belts, pneumatic systems can handle large volumes with minimal labor, reducing operational costs. Third, the flexibility of pneumatic conveying enables easy integration with existing production lines. The system can be customized to fit specific facility layouts, accommodating changes in production volume or process requirements without major modifications.
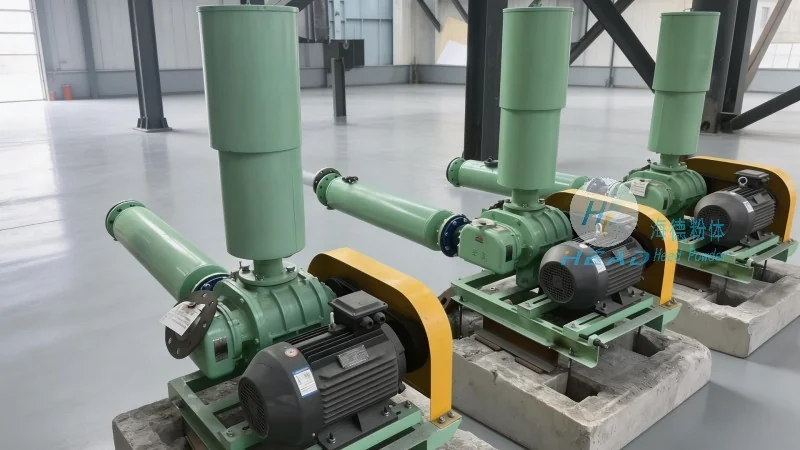
Shandong HeadPowder Engineering Co., Ltd. leverages decades of experience in engineering and material handling to design tailored pneumatic conveying solutions for brown sugar transport. The company's team of experts works closely with clients to assess their specific needs, from initial material analysis to final system installation and commissioning. By understanding the unique characteristics of brown sugar—such as its moisture content, particle size, and flow properties—the engineers can optimize the conveying system for maximum efficiency and minimal energy consumption. HeadPowder utilizes advanced simulation tools to model the pneumatic conveying process, ensuring that the system is designed to handle the exact volume and type of brown sugar required. This approach minimizes downtime and maximizes the return on investment for the client.
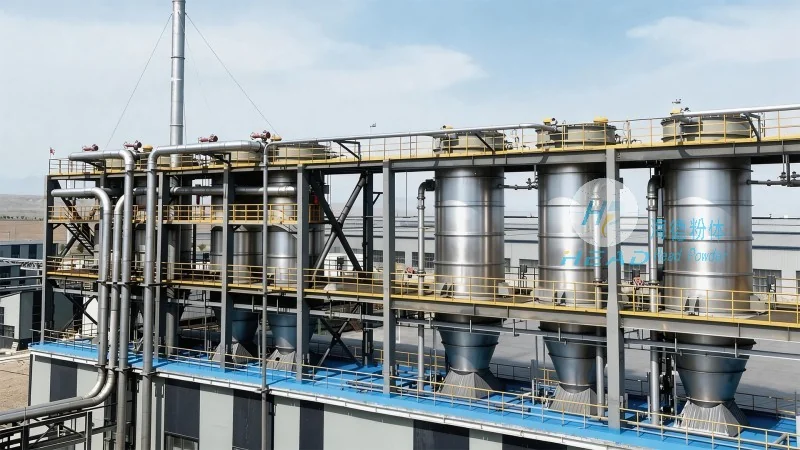
HeadPowder's pneumatic conveying systems for bulk brown sugar are equipped with several key features that enhance performance and reliability. The systems include high-quality, corrosion-resistant materials to withstand the acidic and sugary environment of brown sugar processing. This prevents material degradation and ensures the longevity of the equipment. The company also incorporates advanced control systems that allow for real-time monitoring of the conveying process. Operators can track parameters such as airflow, pressure, and material flow rate, enabling quick adjustments to maintain optimal performance. Additionally, the systems are designed with safety features, including emergency shut-off valves and pressure relief mechanisms, to protect both the equipment and personnel from potential hazards. The integration of these features ensures that the pneumatic conveying system operates safely and efficiently, reducing the risk of accidents and downtime.
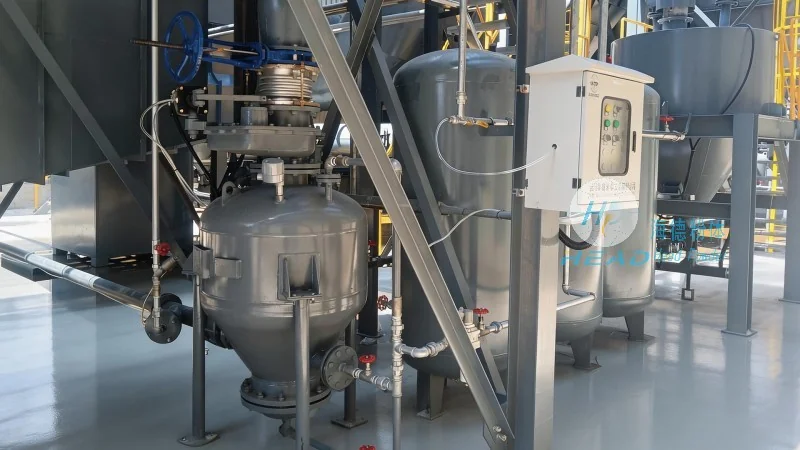
HeadPowder has successfully implemented pneumatic conveying systems for numerous brown sugar processing facilities across China. One client, a large sugar mill, reported a 30% reduction in labor costs after switching to a pneumatic conveying system. The system's ability to handle large volumes of brown sugar continuously eliminated the need for manual loading and unloading, freeing up staff for other tasks. Another client, a food processing company, praised the system's hygienic design, which helped maintain the quality of their brown sugar products and meet stringent food safety regulations. These case studies highlight the effectiveness of HeadPowder's pneumatic conveying solutions in improving operational efficiency and product quality.
As the demand for efficient and reliable bulk material handling continues to grow, pneumatic conveying remains a preferred solution for brown sugar transport. HeadPowder, with its expertise and commitment to innovation, is well-positioned to provide cutting-edge pneumatic conveying systems that meet the evolving needs of the industry. By leveraging advanced engineering and tailored solutions, the company ensures that its clients achieve optimal performance, cost savings, and compliance with industry standards. For businesses looking to enhance their brown sugar processing operations, pneumatic conveying, as implemented by HeadPowder, offers a robust and sustainable solution.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top