

Design of a Negative Pressure Pneumatic Conveying System for Calcium Carbonate Powder
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for the handling of calcium carbonate powder. The negative pressure pneumatic conveying system is a sophisticated solution engineered to efficiently transport fine powders like calcium carbonate, ensuring minimal product degradation and optimal operational efficiency. This system is particularly suitable for industrial applications where precise material handling is critical, such as in the production of coatings, plastics, and other chemical products.
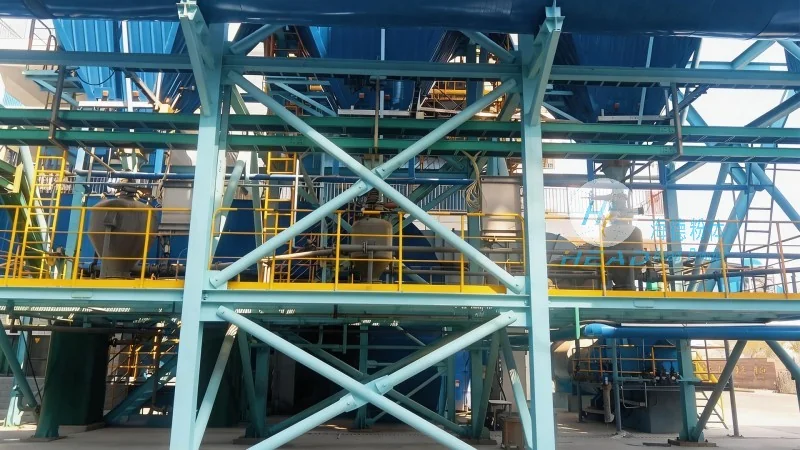
Key Features and Technical Specifications
The negative pressure pneumatic conveying system for calcium carbonate powder incorporates several key features that enhance its performance and reliability. The system operates under negative pressure, which draws the powder from the source and transports it through a sealed pipeline to the destination. This design minimizes dust emissions and prevents product contamination, making it ideal for applications requiring high purity standards. The system is equipped with adjustable air flow control mechanisms, allowing operators to fine-tune the conveying rate based on the specific characteristics of the calcium carbonate powder, such as particle size and moisture content. Additionally, the system includes advanced filtration and separation components to ensure that the conveyed material remains free from impurities, maintaining the quality of the final product.
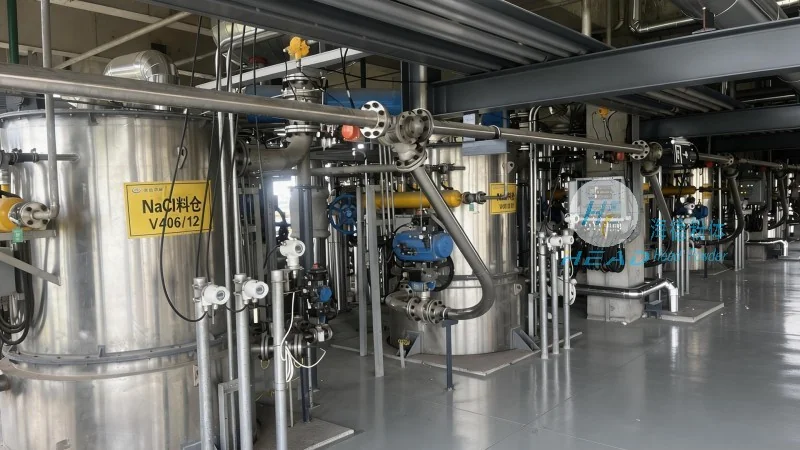
Advantages of the System
Implementing a negative pressure pneumatic conveying system for calcium carbonate powder offers numerous advantages for industrial operations. Firstly, it significantly reduces operational costs by minimizing material loss and energy consumption compared to traditional conveying methods like belt conveyors or screw conveyors. The sealed system prevents dust dispersion, enhancing workplace safety and compliance with environmental regulations. Secondly, the system enhances product quality by preventing exposure to air and moisture, which can cause agglomeration or degradation of the powder. This is crucial for applications where the purity of calcium carbonate is a key factor, such as in the production of high-performance coatings or pharmaceuticals. Furthermore, the system's modular design allows for easy integration into existing production lines, reducing downtime during installation and maintenance.
Application Scenarios
The negative pressure pneumatic conveying system is widely applicable in various industrial sectors that rely on calcium carbonate powder. In the coatings industry, for example, the system efficiently transports fine calcium carbonate particles to mixing and processing units, ensuring consistent quality in the final coating products. In the plastics industry, the system aids in the uniform distribution of calcium carbonate as a filler material, improving the mechanical properties of the end products. Additionally, the system is suitable for use in the chemical and pharmaceutical industries, where precise handling of fine powders is essential to maintain product integrity and regulatory compliance. The system's adaptability to different particle sizes and flow rates makes it a versatile solution for diverse industrial needs.
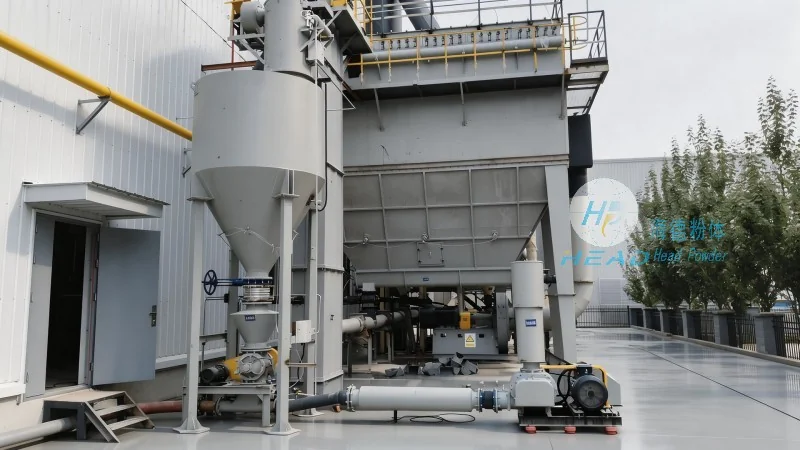
Customization and After-Sales Support
HeadPowder understands that each industrial application has unique requirements, and therefore, offers customized solutions for the negative pressure pneumatic conveying system. The company's engineering team works closely with clients to design systems that meet specific operational parameters, such as conveying distance, material throughput, and environmental constraints. Post-installation, HeadPowder provides comprehensive after-sales support, including regular maintenance services, spare parts supply, and technical assistance to ensure the system operates at peak efficiency. The company's commitment to quality and customer satisfaction is reflected in its adherence to international standards and continuous improvement of its products.