With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Quartz stone, a widely used material in construction, manufacturing, and decorative applications, requires efficient and reliable transportation methods to ensure smooth workflow and minimal operational disruptions. Among the various material handling solutions available, pneumatic conveying stands out as a sophisticated technology that addresses the unique challenges associated with quartz stone transport. This article explores the critical role of pneumatic conveying in the efficient and effective movement of quartz stone, highlighting its advantages, operational principles, and practical applications in industrial settings.

Quartz stone, composed primarily of silicon dioxide (SiO₂), is known for its hardness, durability, and aesthetic appeal. It is commonly used in countertops, flooring, and various industrial components. The physical properties of quartz stone, such as its abrasive nature and relatively high density, pose challenges for traditional bulk material handling methods like belt conveyors or bucket elevators. These conventional systems may suffer from wear and tear, increased maintenance costs, and reduced efficiency when handling quartz stone. Therefore, specialized transport solutions are essential to maintain productivity and protect equipment integrity.
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using a stream of air. This technology offers several advantages over traditional mechanical conveying systems, particularly for abrasive and high-density materials like quartz stone. The primary benefits include reduced equipment wear, lower maintenance requirements, and the ability to handle materials in a closed system, minimizing dust emissions and environmental impact. Pneumatic conveying systems can be designed to operate in both positive and negative pressure modes, providing flexibility in material movement and integration with existing industrial processes.
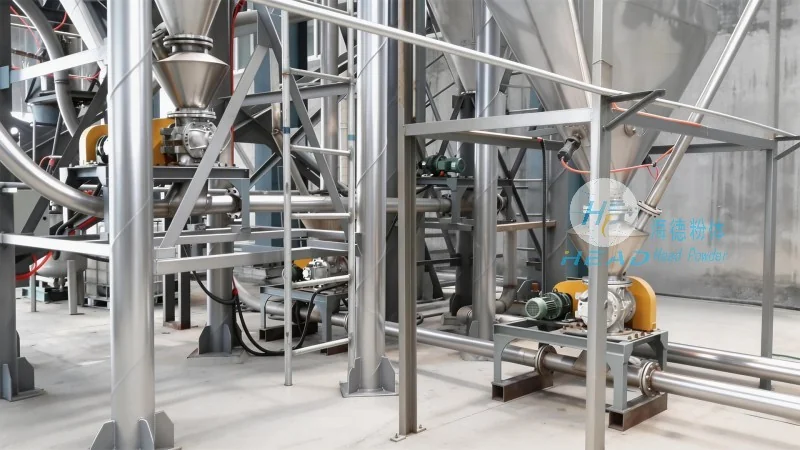
One of the most significant advantages of pneumatic conveying in quartz stone transport is its ability to handle abrasive materials without excessive wear on the system components. Quartz stone's hardness means that traditional metal or rubber components may degrade quickly under continuous use. Pneumatic systems, especially those utilizing high-quality materials like stainless steel or specialized coatings, can withstand the abrasive nature of quartz stone, extending the lifespan of the equipment and reducing downtime. Additionally, the closed-loop design of pneumatic conveying systems helps contain dust and particulate matter, improving workplace safety and compliance with environmental regulations. This is particularly important in industries where air quality and worker health are paramount.
Efficiency is a critical factor in industrial operations, and pneumatic conveying systems are designed to optimize the movement of quartz stone with minimal energy consumption. By using air as the primary transport medium, these systems can achieve high material throughput rates while maintaining low operational costs. The ability to transport materials over long distances without the need for multiple transfer points or intermediate storage reduces overall handling time and labor costs. Furthermore, the compact design of pneumatic conveying systems allows for space-saving installations, which is beneficial in facilities with limited floor space. This efficiency translates into improved productivity and reduced operational expenses for businesses handling quartz stone.
The versatility of pneumatic conveying makes it suitable for a wide range of applications involving quartz stone. For instance, in a quartz stone processing plant, pneumatic systems can be used to transport raw quartz ore from storage silos to grinding mills, then to mixing and molding equipment. In a manufacturing facility producing quartz-based products, such as countertops or tiles, pneumatic conveying can efficiently move finished products from production lines to packaging and shipping areas. The integration of pneumatic conveying with other industrial processes, like automated sorting or quality control, enhances overall system efficiency and ensures consistent material handling across the entire production cycle.
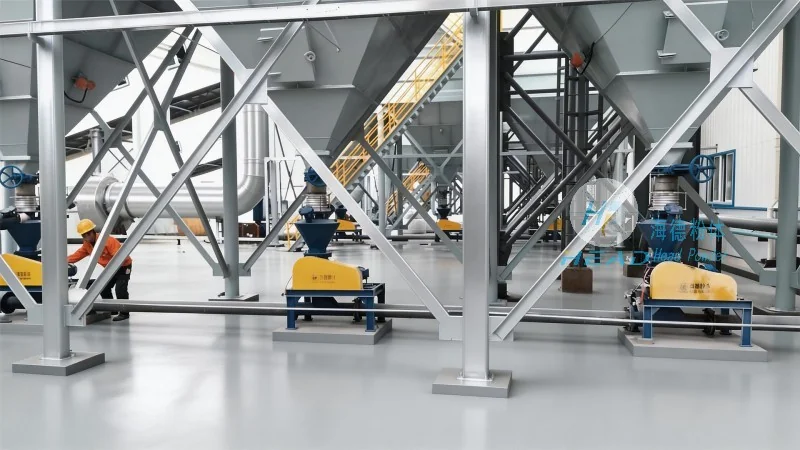
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and implementing advanced pneumatic conveying systems tailored to the specific needs of quartz stone transport. With years of experience in the industry, HeadPowder has developed innovative solutions that address the unique challenges of handling abrasive and high-density materials. The company's expertise lies in customizing pneumatic systems to meet the operational requirements of clients, ensuring optimal performance, reliability, and cost-effectiveness. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for businesses seeking efficient and sustainable quartz stone transportation solutions.
In conclusion, pneumatic conveying plays a vital role in the efficient and effective transportation of quartz stone. Its ability to handle abrasive materials, reduce equipment wear, and minimize environmental impact makes it an ideal solution for modern industrial applications. By leveraging the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can implement advanced pneumatic conveying systems that enhance productivity, lower costs, and ensure compliance with industry standards. As the demand for high-quality quartz stone products continues to grow, the role of efficient material handling technologies like pneumatic conveying will remain indispensable in maintaining competitive advantage and operational excellence.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top