With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the efficient and reliable transport of sodium phosphate is crucial for various industrial applications. This article provides an overview of sodium phosphate conveying systems, with a focus on the advantages and features of pneumatic conveying technology. The system is designed to handle sodium phosphate with precision, ensuring minimal loss and optimal performance in material handling processes.
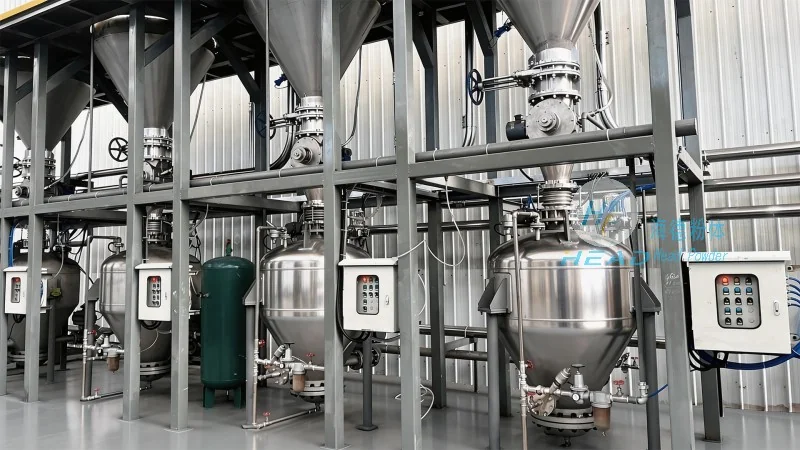
Pneumatic conveying offers several key benefits when transporting sodium phosphate. Firstly, it eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and operational downtime. Secondly, the system can handle a wide range of particle sizes and moisture contents, making it versatile for different production environments. Additionally, pneumatic conveying systems provide better control over the flow rate, allowing for precise dosing and mixing of sodium phosphate in manufacturing processes. The enclosed design also minimizes dust exposure, enhancing workplace safety and compliance with environmental regulations.
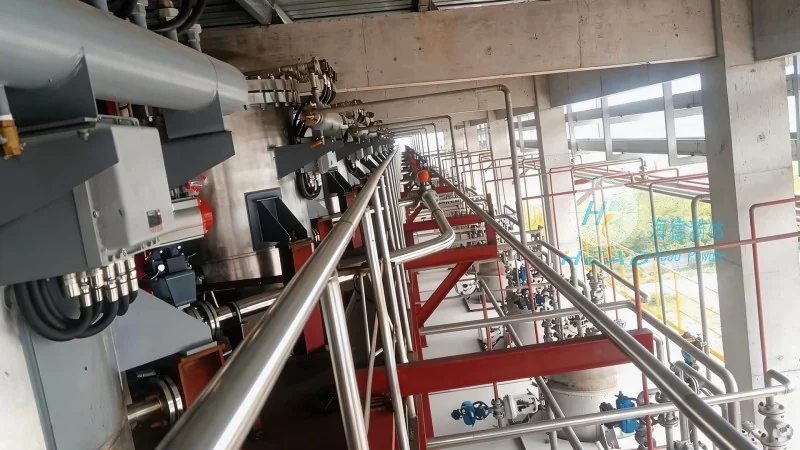
The sodium phosphate conveying system by Shandong HeadPowder Engineering Co., Ltd. incorporates advanced features tailored to industrial needs. The system utilizes high-efficiency air pumps and specialized pipelines to ensure consistent material transport. It includes adjustable speed controls that allow operators to modulate the conveying rate based on production requirements. Furthermore, the system is equipped with monitoring sensors that provide real-time data on flow rates and pressure, enabling proactive maintenance and preventing system failures. The robust construction of the equipment ensures durability and long-term performance, even under demanding operational conditions.
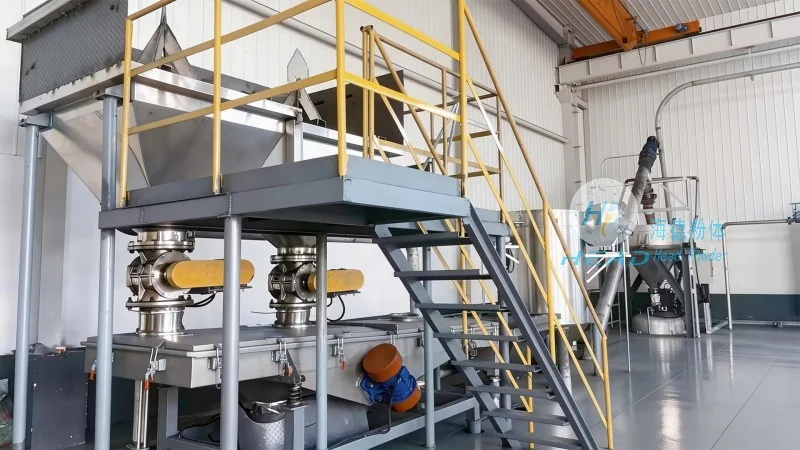
Sodium phosphate conveying systems are widely used in industries such as food processing, pharmaceuticals, and chemical manufacturing. In food processing, the system ensures hygienic handling of sodium phosphate, which is a common food additive. In pharmaceutical applications, the precise control over material transport is critical for maintaining product quality and consistency. The chemical industry benefits from the system's ability to handle various forms of sodium phosphate, including powders and granules. Overall, the advantages of pneumatic conveying, combined with the advanced features of the system, result in improved operational efficiency, reduced costs, and enhanced product quality.
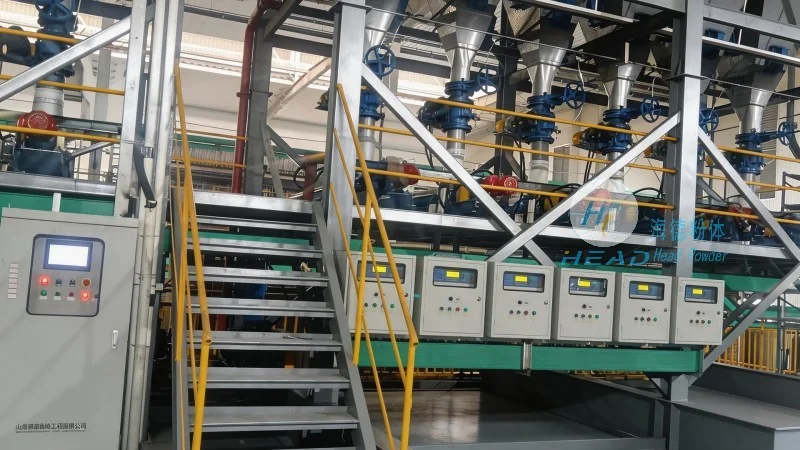
Shandong HeadPowder Engineering Co., Ltd. offers a comprehensive solution for sodium phosphate conveying through its advanced pneumatic conveying systems. By leveraging the benefits of pneumatic technology and incorporating robust design features, the system ensures reliable and efficient transport of sodium phosphate. With its focus on durability, precision, and safety, the system meets the demands of modern industrial applications, providing businesses with a competitive edge in their respective fields. Based in Shandong, China, HeadPowder continues to innovate and deliver high-quality conveying solutions tailored to the needs of global industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top