With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
High-calcium materials, such as limestone or calcium carbonate, are integral to numerous industrial processes across sectors including chemical manufacturing, food production, and pharmaceuticals. The efficient and reliable transportation of these powders is essential for maintaining production efficiency and upholding product quality standards. Pneumatic conveying systems have become a preferred solution for handling high-calcium materials due to their ability to transport powders without direct contact, minimizing contamination risks and enhancing process flexibility.
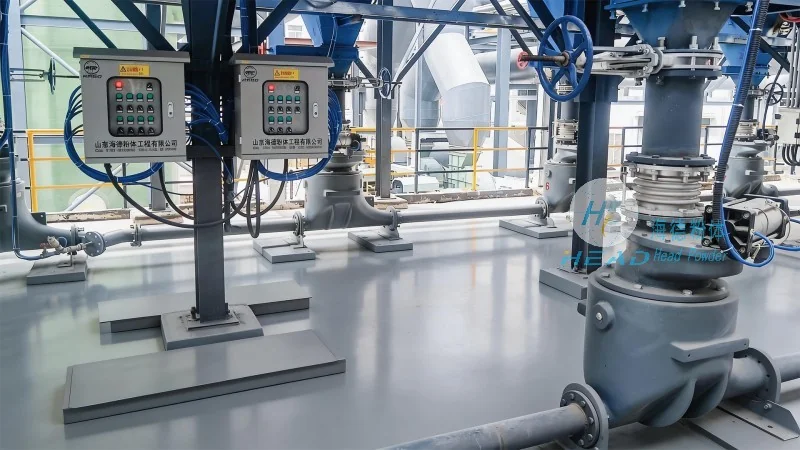
Developed by Shandong HeadPowder Engineering Co., Ltd., the high-calcium pneumatic conveying system is engineered to address the unique challenges posed by calcium-rich powders. Key features include advanced material handling capabilities, robust construction to withstand abrasive materials, and integrated control systems for precise flow regulation. The system utilizes a combination of positive and negative pressure conveying modes, enabling flexible operation across diverse production scenarios. Additionally, the design incorporates corrosion-resistant components to ensure longevity and reduce maintenance requirements.
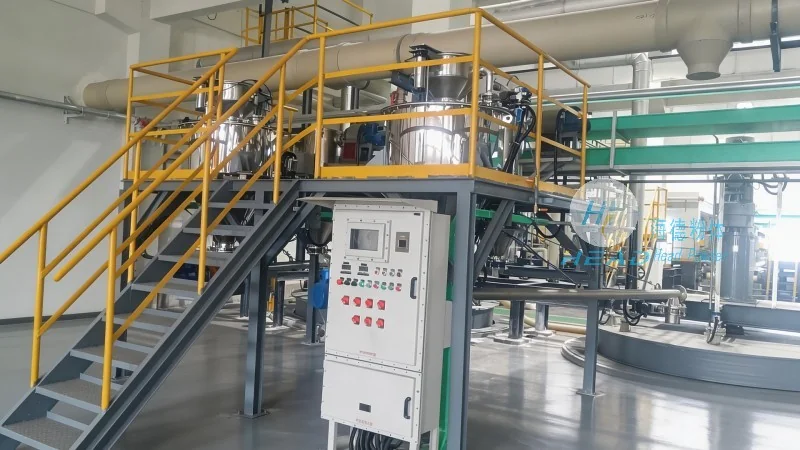
Shandong HeadPowder Engineering Co., Ltd. has optimized the high-calcium pneumatic conveying system for superior performance. Technical specifications include a maximum conveying capacity of up to 50 tons per hour, with adjustable flow rates to accommodate varying production demands. The system operates at pressures ranging from 0.5 to 2.0 bar, ensuring efficient material transport while minimizing energy consumption. Performance metrics indicate a material recovery rate exceeding 99%, with low dust emissions and minimal product degradation. These specifications make the system suitable for both large-scale industrial applications and smaller processing facilities.
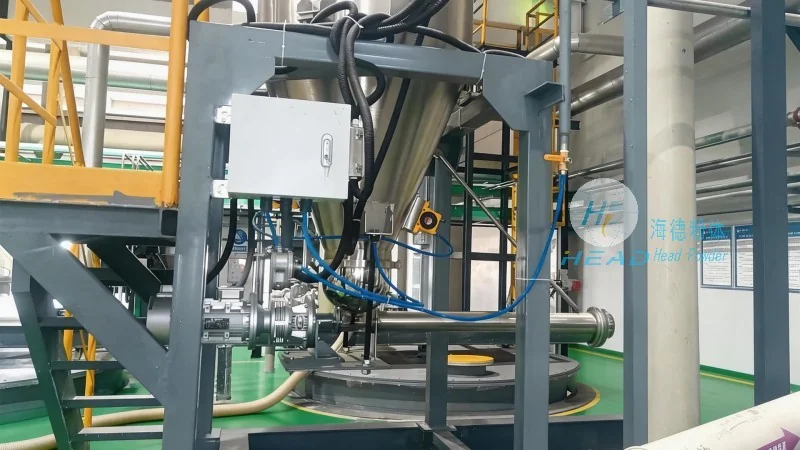
The high-calcium pneumatic conveying system is particularly well-suited for industries reliant on calcium-based raw materials. In chemical manufacturing, it facilitates the transport of limestone and calcium carbonate from storage silos to processing units, streamlining production workflows. In the food industry, the system ensures hygienic handling of calcium supplements and additives, maintaining product purity and compliance with regulatory standards. Pharmaceutical manufacturers also benefit from the system's ability to handle calcium-based excipients with minimal contamination, enhancing product safety and quality. Overall, the system contributes to increased operational efficiency, reduced downtime, and lower maintenance costs, making it a cost-effective solution for high-calcium material handling.
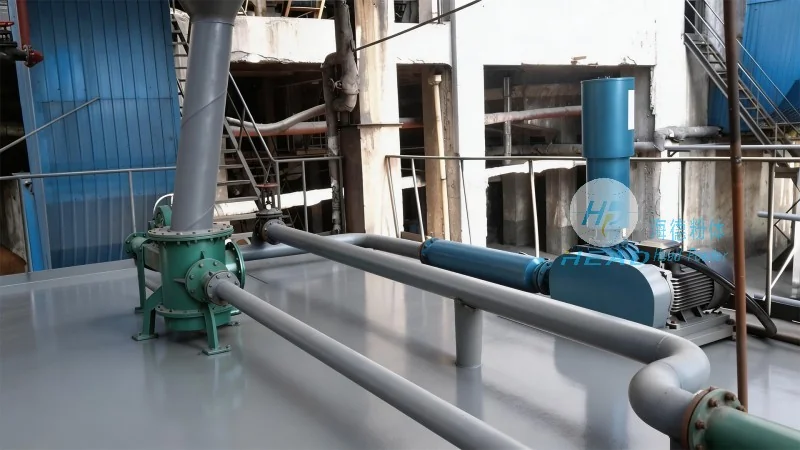
Proper installation and regular maintenance are critical to maximizing the lifespan and performance of the high-calcium pneumatic conveying system. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive installation services, including site assessment and system integration to ensure optimal performance. Routine maintenance involves periodic inspection of components such as air filters, conveyor pipes, and valves to prevent blockages and ensure consistent operation. The system's modular design allows for easy access to internal parts, reducing downtime during maintenance. Additionally, the company offers training programs for operators to enhance their understanding of system operation and troubleshooting, further ensuring the system's reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top