With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Mannitol is a widely utilized organic compound, particularly prominent in the pharmaceutical and food industries due to its unique physical properties, such as its high solubility and stability. However, the physical nature of mannitol—as a fine, crystalline powder—presents significant logistical challenges during the manufacturing process. Transporting this material from storage silos to processing units or packaging lines requires a method that preserves the integrity of the powder while ensuring operational efficiency. Traditional mechanical conveying methods, such as screw conveyors or bucket elevators, often struggle with issues like high wear, powder degradation, and contamination risks. Consequently, the industry has turned toward advanced pneumatic conveying technologies to address these hurdles. This shift necessitates a partnership with a specialized entity capable of providing robust engineering solutions tailored to the specific needs of this delicate material.
Handling mannitol powder is not merely a matter of moving material from point A to point B; it involves navigating complex technical requirements. The fine particles are prone to dusting, which poses serious safety hazards, including explosion risks in certain environments. Furthermore, the abrasive nature of the powder can degrade standard equipment over time, leading to frequent maintenance and downtime. A pneumatic conveying system must be engineered to handle these characteristics effectively. The system needs to manage air pressure and flow rates precisely to ensure that the powder is conveyed gently enough to prevent attrition (breaking down of particles) while maintaining a high enough velocity to prevent settling or blockages. Addressing these challenges requires a deep understanding of fluid dynamics and material handling engineering.
Selecting the right partner for material handling infrastructure is critical for the long-term success of a production facility. A generic supplier may offer standard equipment that does not account for the nuances of the specific product being handled. In contrast, a specialized manufacturer brings years of technical expertise and industry-specific knowledge. Shandong Headpowder Engineering Co., Ltd. has established itself as a premier entity in this field, focusing exclusively on the intricacies of powder transport. As a dedicated mannitol powder pneumatic conveying manufacturer, the company understands the importance of equipment longevity and hygiene standards required in pharmaceutical-grade environments. Their expertise ensures that every component of the system is selected based on rigorous testing and quality assurance protocols, providing clients with machinery that is both reliable and durable.
One size does not fit all in industrial engineering, especially when dealing with bulk materials. A generic approach to powder transport can lead to inefficiencies and increased operational costs. Therefore, a comprehensive mannitol powder pneumatic conveying scheme must be custom-designed to fit the specific layout and production goals of the facility. This involves a detailed analysis of the plant's spatial constraints, the required production capacity, and the specific physical properties of the mannitol being processed. The design process should consider factors such as the distance between the source and destination, the elevation changes, and the need for containment to prevent environmental contamination. By developing a bespoke scheme, engineers can optimize the air-to-material ratio, minimize energy consumption, and ensure a smooth, uninterrupted flow of material throughout the production cycle.
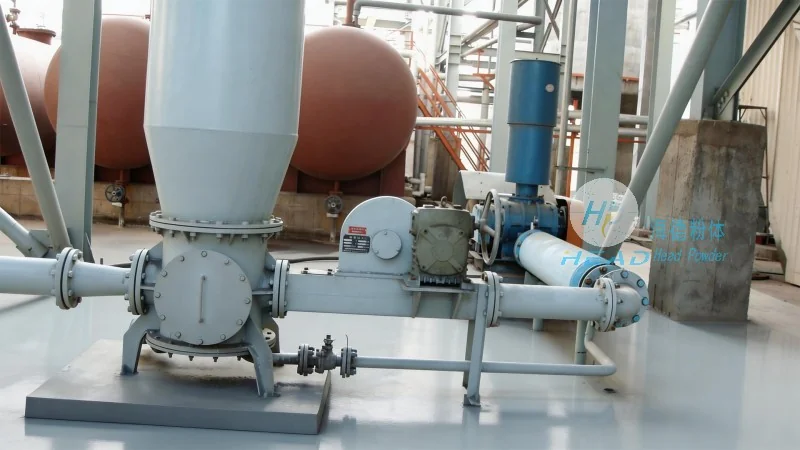
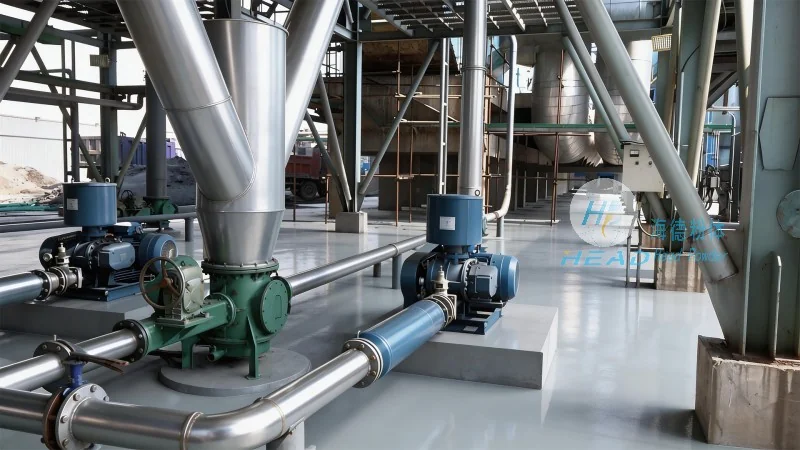
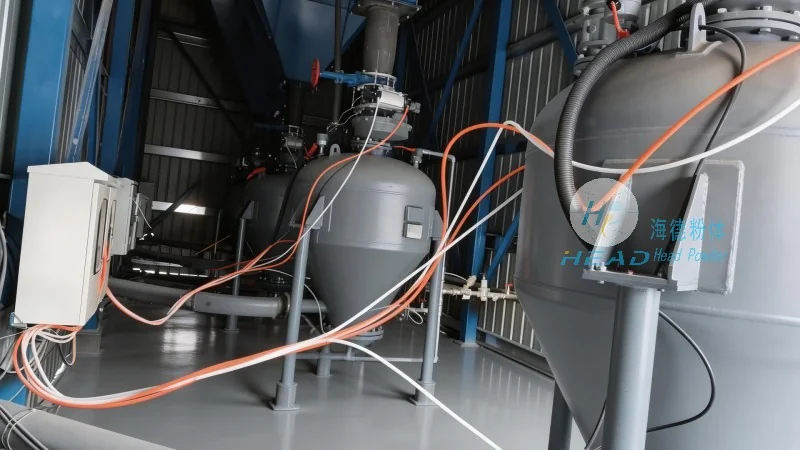
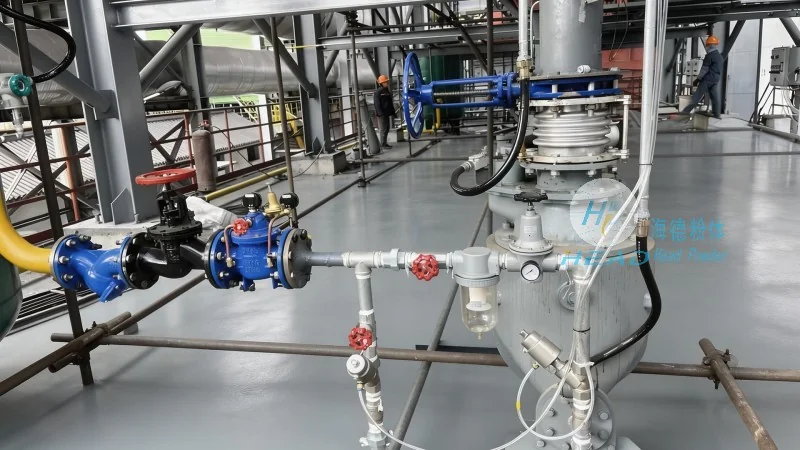
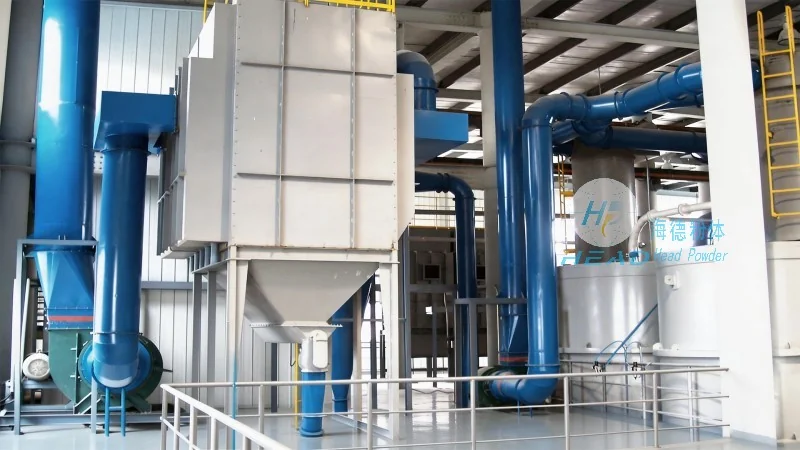
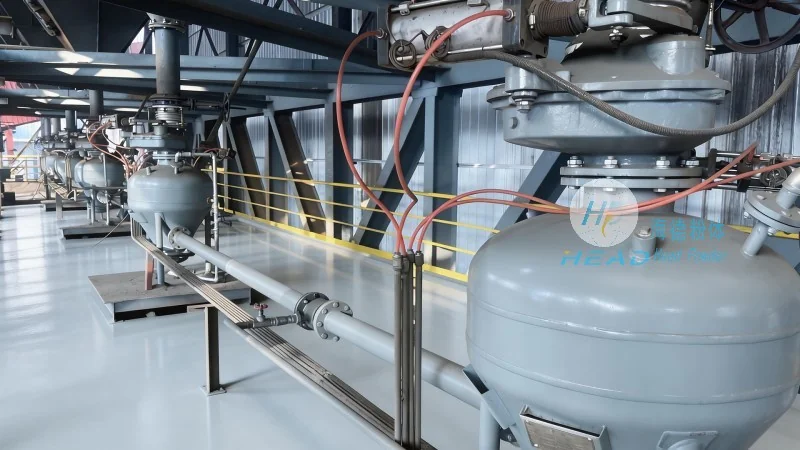
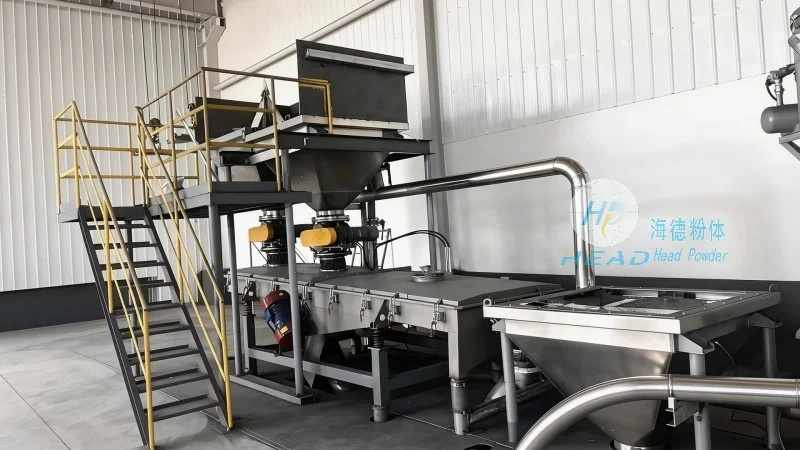
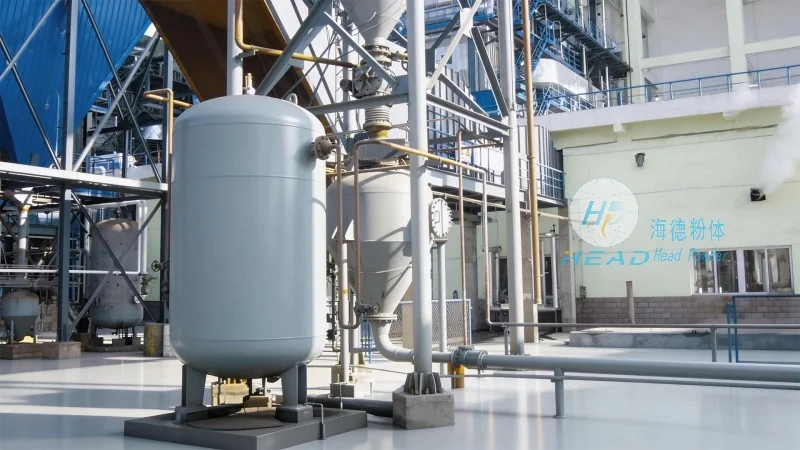
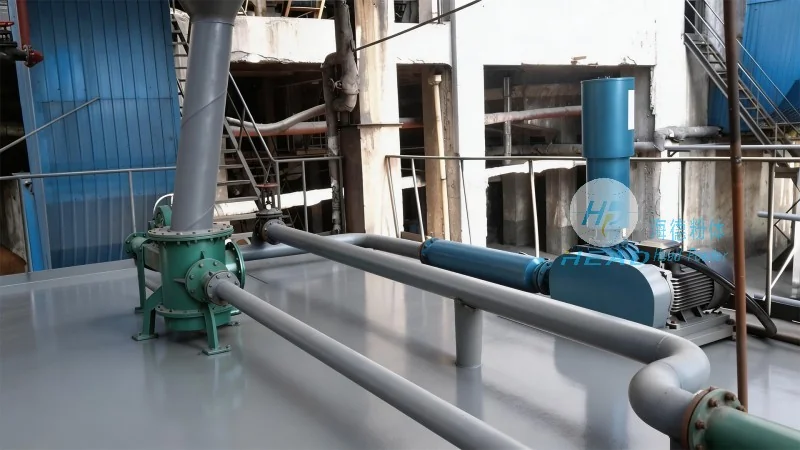
A successful pneumatic conveying project relies on the seamless integration of various components into a cohesive mannitol powder conveying system. This system typically includes a vacuum generator or blower, a feed hopper with a dosing device, a high-pressure pipeline, and a receiving vessel equipped with dust filtration systems. The quality of these components determines the overall performance of the system. As a leading engineering firm, Shandong Headpowder Engineering Co., Ltd. ensures that every element of the system—from the selection of wear-resistant pipes to the calibration of control valves—is manufactured to exacting standards. The systems are designed to be user-friendly, allowing for easy operation and minimal maintenance. Whether the requirement is for a dilute-phase system for short distances or a dense-phase system for longer hauls, the provided equipment is engineered to deliver consistent and reliable performance under varying operational conditions.
Investing in a high-quality pneumatic conveying solution offers numerous advantages beyond simple transportation. The primary benefit is the significant reduction in cross-contamination risks. Since the conveying process is fully enclosed, there is no exposure of the powder to the external environment, which is crucial for maintaining the purity and sterility of the product. Additionally, these systems drastically reduce the physical labor required for material handling, thereby improving workplace safety and reducing the likelihood of workplace injuries associated with manual lifting or operating heavy machinery. The automation provided by a modern pneumatic system also allows for precise inventory management and real-time monitoring, enabling operators to adjust flow rates instantly based on production demands. These operational efficiencies translate directly into cost savings and higher overall productivity for the facility.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top