With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Environmental regulations in Norway are among the strictest in the world, requiring power plants to implement advanced flue gas desulfurization (FGD) technologies to meet emission standards. In the case of the Bergen power plant, the primary challenge was the efficient and reliable transport of limestone powder, which is a critical raw material for the wet scrubbing process. Limestone powder is a fine, abrasive, and potentially cohesive material that poses significant difficulties for traditional mechanical conveying methods. The plant required a solution that could handle large volumes of material with minimal maintenance, ensuring continuous operation without interruption. This necessity led to the search for a robust pneumatic conveying system capable of operating under varying environmental conditions typical of the region.
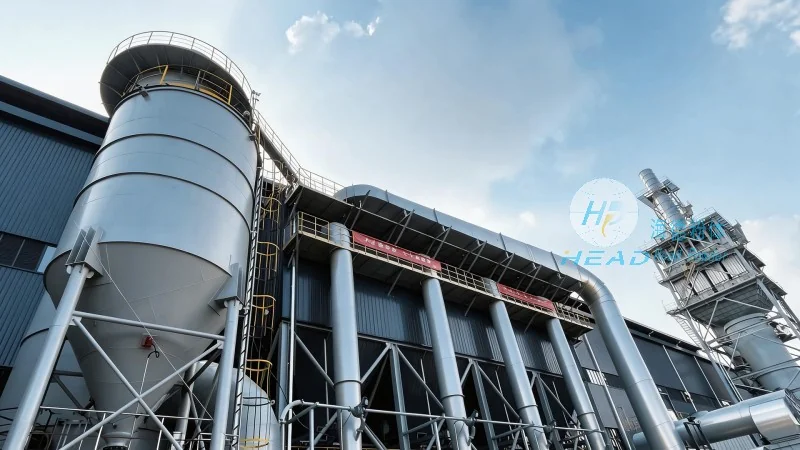
The selection of the right technology was paramount to the success of the project. The engineering team evaluated various options, ultimately deciding on a system that leveraged the specific advantages of pressure vessels and air compression technology. The goal was to create a closed-loop system that prevented dust leakage, protected the environment, and maintained the chemical properties of the limestone powder during transfer. The project in Bergen serves as a prime example of how modern engineering can solve complex material handling problems in the energy sector.
To address the transportation needs, the project implemented a specialized **pneumatic conveying case** solution designed for heavy-duty industrial applications. The core of this system is the **bulk material pneumatic conveying** technology, which utilizes air pressure to move materials through a pipeline network. This method is particularly effective for limestone powder, which is prone to bridging and clogging in hoppers. By utilizing the force of compressed air, the system ensures that the powder flows smoothly from the storage silo to the reaction tower, maintaining a consistent flow rate essential for the FGD process.
The system architecture is built around a series of storage silos equipped with advanced feeding mechanisms. The limestone powder is loaded into a pressure vessel, known as a "binerator" or bulk loading tank. Once loaded, the vessel is sealed and pressurized. The high-pressure air forces the powder into the transportation pipeline, where it is carried to the destination. This process is highly efficient and allows for the precise dosing of the powder into the scrubber. The Bergen project demonstrated that pneumatic conveying is not only suitable for fine powders but also for abrasive materials like limestone, provided the system is engineered with appropriate wear-resistant materials and flow aids.
Implementing a bulk material pneumatic conveying system offers numerous advantages over mechanical conveyors such as screw feeders or belt conveyors. In the Bergen power plant scenario, the pneumatic system eliminated the risk of material degradation. Mechanical conveyors can sometimes cause excessive friction and heat generation, which is undesirable for limestone powder. Furthermore, pneumatic conveying is inherently dust-tight. In a power plant environment, preventing dust escape is crucial for air quality and operator safety. The enclosed nature of the system ensures that the limestone powder remains contained within the piping and vessels, significantly reducing the environmental footprint of the plant.
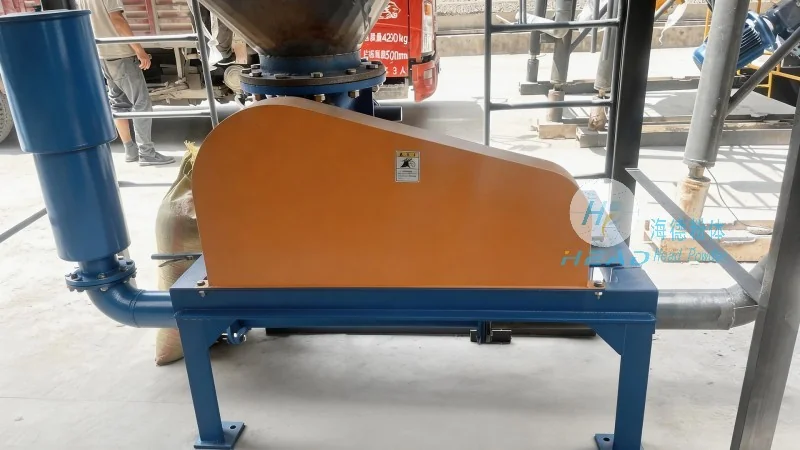
Another critical factor in the Bergen case was the distance and layout of the plant. The pneumatic system is flexible in terms of layout, allowing for straight-line runs with minimal bends. This reduces the pressure drop and wear on the pipeline. The system also features automatic cleaning capabilities, ensuring that the pipeline remains clear of residue after each batch transfer. This reliability is vital for a power plant that cannot afford unplanned downtime. The success of this installation highlights the versatility and reliability of modern pneumatic conveying systems in handling industrial minerals.
The engineering standards applied to the Bergen project reflect a commitment to quality and safety, aligning with **European pneumatic conveying** standards. The design team focused on optimizing the air-to-material ratio to ensure that the limestone powder was transported without excessive air usage, which improves energy efficiency. The system utilizes high-quality valves and sensors to monitor pressure and flow in real-time, ensuring stable operation. The piping and vessel materials were selected based on their ability to withstand the abrasive nature of limestone, ensuring a long service life even in harsh operating environments.
The control system of the Bergen plant is fully automated, allowing for remote operation and monitoring. This reduces the need for manual intervention, thereby lowering the risk of human error. The system is designed to handle variations in material flow, ensuring that the desulfurization process remains consistent regardless of external factors. By adhering to strict engineering protocols, the project achieved a high level of operational efficiency. This case study serves as a benchmark for other power plants in the region looking to upgrade their material handling infrastructure.
The successful execution of the Bergen power plant project was made possible by the expertise of Shandong Headpowder Engineering Co., Ltd. Based in Shandong, China, the company has established itself as a leading provider of pneumatic conveying solutions and bulk material handling equipment. Headpowder specializes in the design, manufacturing, and installation of complete systems, ranging from individual components to complex turnkey projects. The company’s dedication to innovation and quality has earned it a reputation as a trusted partner for industrial clients across the globe.
Headpowder’s engineering team possesses deep knowledge of powder mechanics and fluid dynamics. They work closely with clients to understand their specific requirements, whether it is the transportation of limestone, cement, fly ash, or other industrial powders. The company’s facility in Shandong is equipped with state-of-the-art manufacturing technology, ensuring that every component meets rigorous quality control standards. By integrating advanced software for simulation and design, Headpowder can predict system performance and optimize configurations before physical installation begins.
Shandong Headpowder Engineering Co., Ltd. prides itself on its customer-centric approach. The company understands that a pneumatic conveying system is a long-term investment. Therefore, they focus on providing not only high-quality equipment but also comprehensive after-sales service. This includes training for plant operators, routine maintenance schedules, and readily available spare parts. The company’s global footprint allows it to support projects in diverse geographical locations, adapting to local regulations and environmental conditions.
The Headpowder brand is synonymous with reliability and performance. The company continuously invests in research and development to improve its technologies. From optimizing the design of the **bulk material pneumatic conveying** valves to developing more energy-efficient compressors, Headpowder is always looking for ways to enhance system performance. This forward-thinking approach ensures that their clients receive the most advanced solutions available in the market. The Bergen project is a testament to the company's ability to deliver complex solutions that meet the highest international standards.
For clients interested in implementing similar solutions for their power plants or industrial facilities, Shandong Headpowder Engineering Co., Ltd. offers expert consultation and support. The company’s team of engineers is ready to analyze your specific material handling needs and design a customized system. Whether you are looking to upgrade an existing system or install a new one, Headpowder provides end-to-end services from design to commissioning.
If you require further information regarding the project or wish to discuss your own requirements, please contact Mr. Zhang, the project manager at Headpowder. He can be reached via WeChat at 15662777102. The team at Shandong Headpowder is committed to providing professional advice and ensuring the success of your pneumatic conveying projects. With a focus on quality, efficiency, and customer satisfaction, Headpowder is your ideal partner for bulk material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top