

Principle and Working Scene Characteristics of Molybdenum Oxide Material Handling System Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced material handling systems tailored for molybdenum oxide processing. The company's expertise lies in developing efficient equipment that ensures safe and reliable transportation of molybdenum oxide, a critical component in various industrial applications.
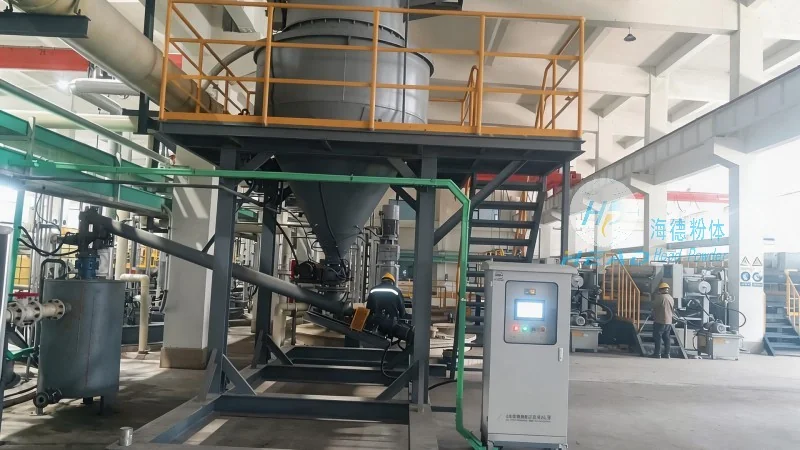
Understanding the Core Principles of Molybdenum Oxide Material Handling Systems
The molybdenum oxide material handling system operates on a sophisticated principle designed to manage the unique properties of molybdenum oxide. This system integrates multiple components, including conveyors, storage silos, and control mechanisms, to facilitate the seamless transfer of material from storage to processing units. The design emphasizes durability and corrosion resistance, as molybdenum oxide can be reactive under certain conditions. Advanced materials and engineering techniques are employed to prevent material degradation and equipment wear, ensuring long-term operational efficiency.
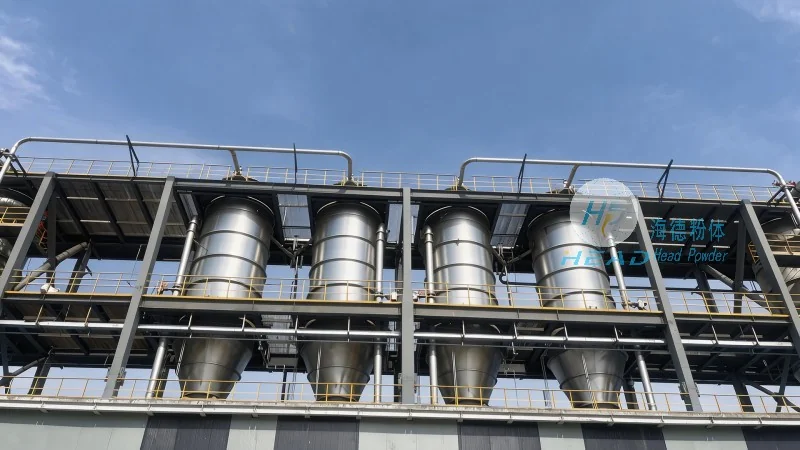
Key Working Scene Characteristics of the Equipment
HeadPowder's molybdenum oxide material handling systems are deployed in diverse industrial settings, each with distinct operational requirements. In mining and processing facilities, the equipment is used to handle bulk molybdenum oxide from extraction sites to refining plants. The systems are engineered to handle high volumes with minimal downtime, supporting continuous production cycles. In chemical and metallurgical industries, the equipment ensures precise dosing and mixing of molybdenum oxide in reaction processes, maintaining consistent product quality. The working scenes also include environmental considerations, as the systems are designed to minimize dust emissions and comply with safety regulations, protecting both personnel and the environment.
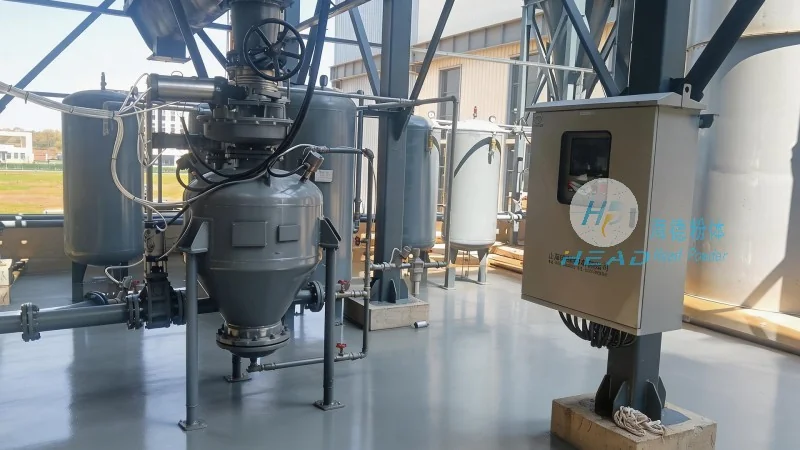
Technical Advantages and Application Scenarios
One of the primary advantages of HeadPowder's molybdenum oxide material handling systems is their adaptability to different operational scales. Whether for small-scale laboratory use or large-scale industrial production, the equipment can be customized to meet specific throughput and material handling needs. The systems incorporate advanced sensors and automation controls, enabling real-time monitoring and adjustment of material flow. This automation reduces human error and enhances safety, making the equipment suitable for high-risk environments. The working scenes also include integration with other processing equipment, such as crushers, classifiers, and reactors, creating a cohesive material flow system that optimizes overall production efficiency.
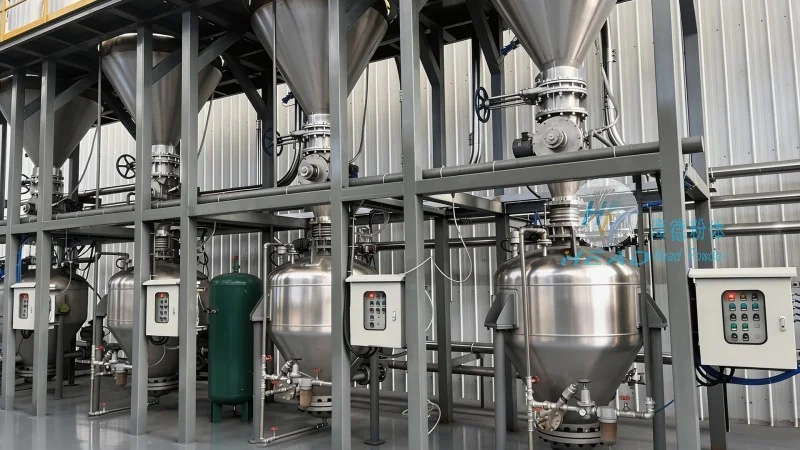
Company Background and Commitment to Quality
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has established itself as a trusted provider of material handling solutions for the molybdenum oxide industry. The company's commitment to innovation and quality is reflected in its state-of-the-art manufacturing facilities and rigorous quality control processes. With a team of experienced engineers and technicians, HeadPowder ensures that each system is designed and built to meet international standards and customer specifications. The company's focus on customer satisfaction and long-term partnerships has enabled it to serve a wide range of clients across various industries, including mining, chemical, and metallurgical sectors.