With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Red bean material handling systems are specialized equipment designed to efficiently transport and manage red bean materials in various industrial and agricultural settings. These systems are engineered to optimize the flow of red bean products from storage to processing or packaging stages, ensuring smooth and reliable operation. The core principle behind such systems involves the integration of mechanical components, control mechanisms, and material handling technologies tailored to the unique characteristics of red bean handling, including size, density, and moisture content.
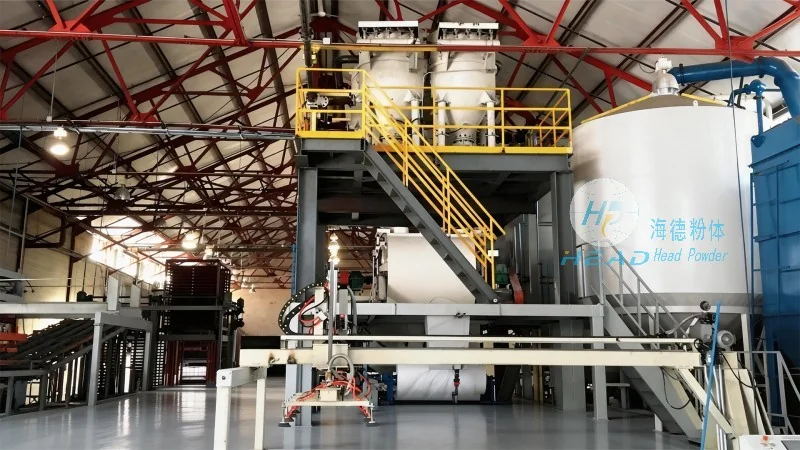
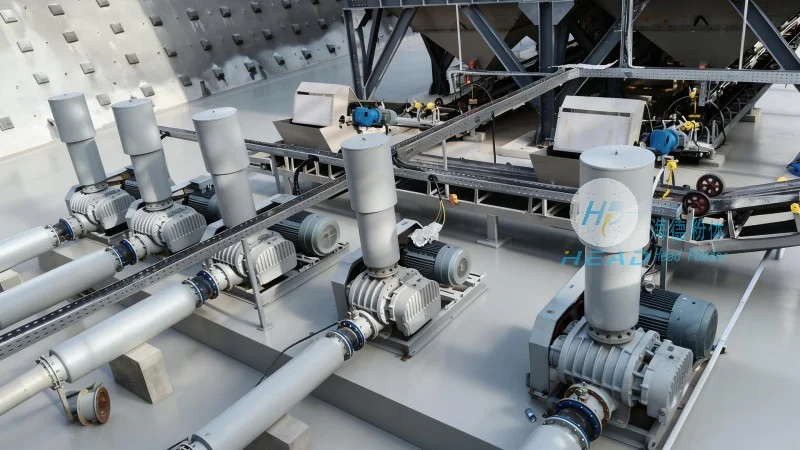
The fundamental working principle of red bean material handling systems revolves around the use of conveyor belts, elevators, and other transport mechanisms to move red beans through different stages of the production process. These systems typically operate by feeding red beans into a hopper or storage container, where they are then transferred to the primary conveyor system. From there, the red beans are transported to processing units, such as cleaning or sorting equipment, or directly to packaging lines. The control systems in these systems ensure that the flow rate, speed, and direction of the red bean movement are precisely regulated to maintain consistent quality and efficiency. Additionally, many modern red bean material handling systems incorporate sensors and automation technologies to enhance operational accuracy and reduce human error, further improving overall performance.
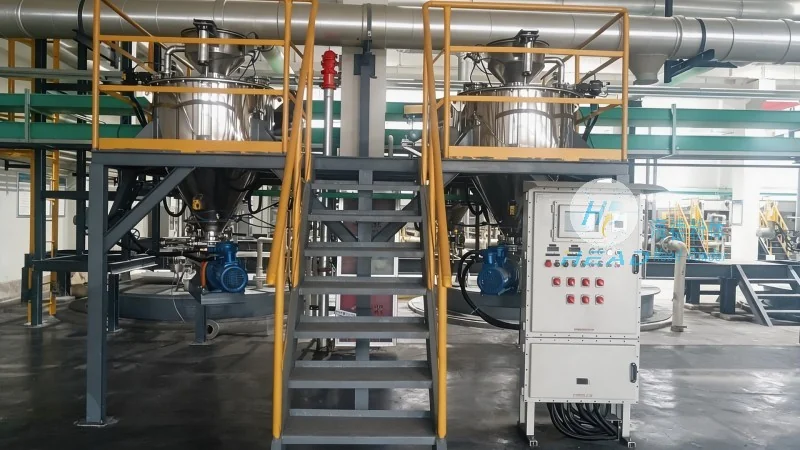
Red bean material handling systems are commonly employed in a variety of working scenes, each with distinct requirements and operational characteristics. In agricultural processing facilities, these systems are used to handle freshly harvested red beans from fields, transporting them to storage silos or processing plants. The working scene in such environments often involves large volumes of raw material, requiring robust and high-capacity handling equipment to maintain production efficiency. In contrast, in food processing plants, the working scene may focus on the secondary processing of red beans, such as roasting, grinding, or packaging, where the material handling systems must ensure hygienic and contamination-free operation. The characteristics of the working scene also influence the design of the material handling system, including the choice of conveyor type (e.g., belt conveyors, screw conveyors, or bucket elevators) and the integration of safety features to protect both the equipment and personnel. Furthermore, the working scene may vary based on the scale of the operation, from small-scale farms to large industrial processing facilities, each requiring customized solutions to meet specific production needs.
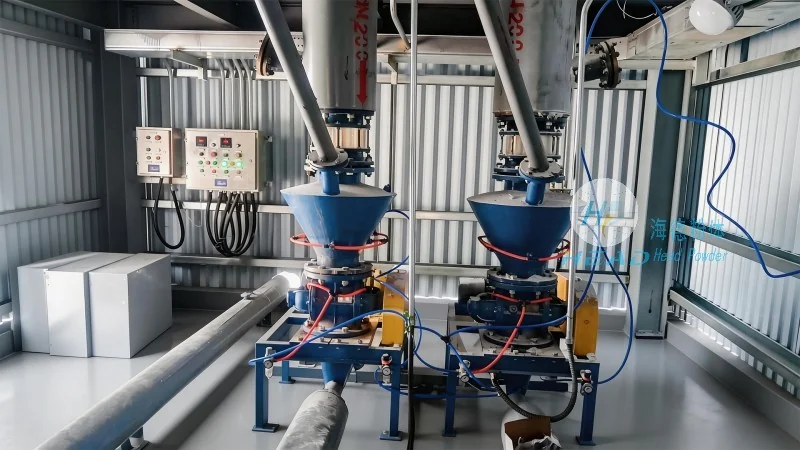
HeadPowder, the manufacturer of red bean material handling systems, is a leading company based in Shandong, China. With a strong commitment to quality and innovation, HeadPowder specializes in designing and manufacturing advanced material handling solutions tailored to the needs of the red bean industry. The company's headquarters is located in Shandong, where it operates a state-of-the-art research and development center, manufacturing facility, and customer service team. HeadPowder's expertise lies in the integration of mechanical engineering, automation technology, and material science to develop systems that enhance the efficiency and reliability of red bean handling processes. The company adheres to international standards and quality control measures to ensure that its products meet the highest industry benchmarks, providing customers with durable and cost-effective solutions for their material handling needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top