With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
White gray powder conveying systems are essential equipment in various industrial applications, designed to efficiently transport bulk materials like white and gray powders. Understanding their operational principles and typical working environments is crucial for selecting the right system for specific industrial needs.
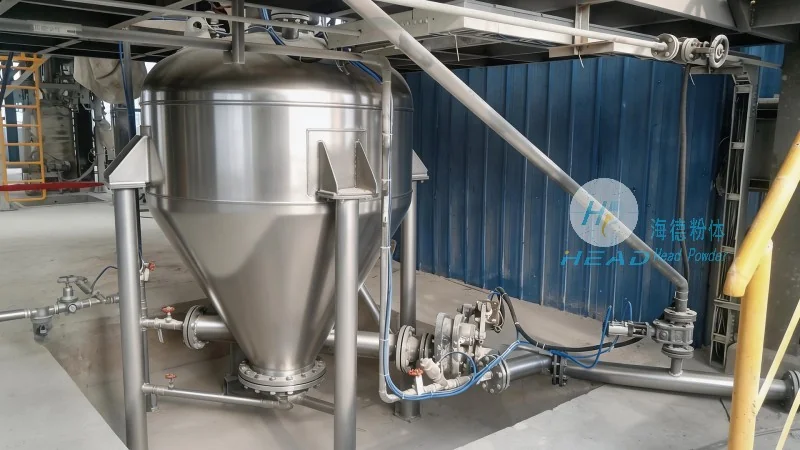
The fundamental principle of these systems revolves around the use of mechanical or pneumatic methods to move powder materials from a source to a destination. Mechanical conveying systems typically employ screw conveyors, belt conveyors, or bucket elevators, which utilize rotational motion or gravity to transport powders. Pneumatic conveying systems, on the other hand, use compressed air or other gases to create a flow of powder through pipes. For white and gray powders, which often have fine particle sizes and can be prone to caking or agglomeration, specialized designs are employed to ensure smooth and efficient transport.
Key components of a white gray powder conveying system include the hopper for material storage, the conveyor mechanism (either mechanical or pneumatic), and the control system for regulating flow rates and pressure. The design of these components is critical to prevent material degradation, blockages, or contamination, which are common issues in powder handling. For instance, the hopper may be equipped with a discharge valve or a rotary valve to control the flow of powder into the conveyor, while the conveyor itself may feature a smooth interior surface to minimize friction and prevent powder buildup.
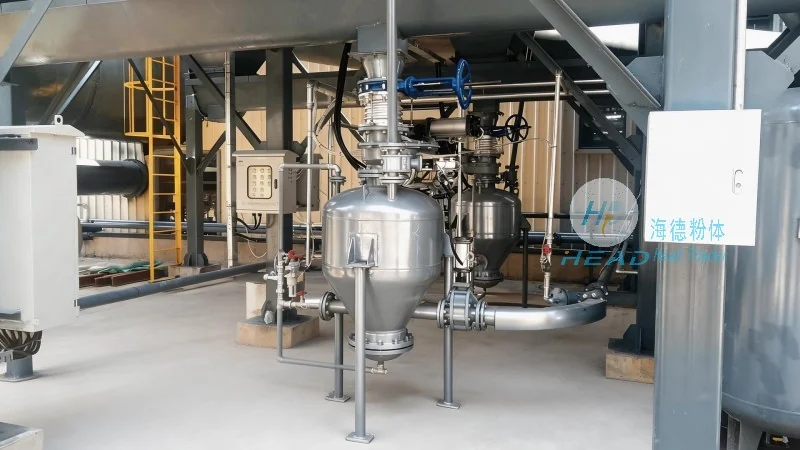
White gray powder conveying systems are widely used in industries such as construction, chemical manufacturing, food processing, and pharmaceuticals. The working scene characteristics vary based on the specific application, but generally include high-volume material handling, precise control over powder flow, and the need for minimal material loss or contamination. In construction, these systems are used to transport cement, lime, or other building materials to different parts of a site, ensuring efficient material distribution and reducing manual labor. In chemical manufacturing, they handle various powders like pigments, catalysts, or raw materials, where accurate dosing and consistent flow are essential for production processes.
In food processing, the systems must meet stringent hygiene standards, with components made of food-grade materials and designed to prevent cross-contamination. The working environment may involve high temperatures or moisture, requiring specialized materials and sealing mechanisms to maintain product quality. Similarly, in pharmaceutical applications, the conveying systems are designed to handle sensitive powders, with features like dust collection, filtration, and sterile processing to ensure compliance with regulatory standards.
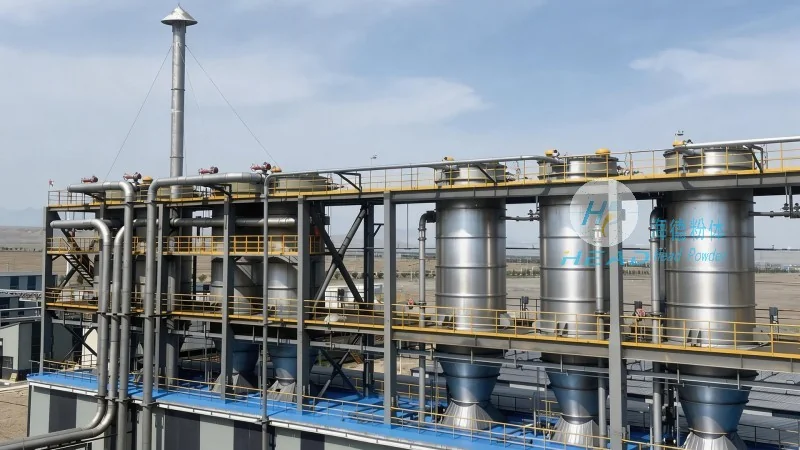
The choice of a white gray powder conveying system depends on the specific working environment and operational requirements. For example, in outdoor construction sites, systems may need to be weather-resistant and durable to withstand harsh conditions. In contrast, indoor pharmaceutical facilities require systems that are easy to clean and maintain, with minimal dead zones where powder can accumulate. Another consideration is the scale of operation; large-scale industrial plants may use multiple conveying lines and integrated control systems to manage high throughput, while smaller applications may opt for simpler, single-line systems.
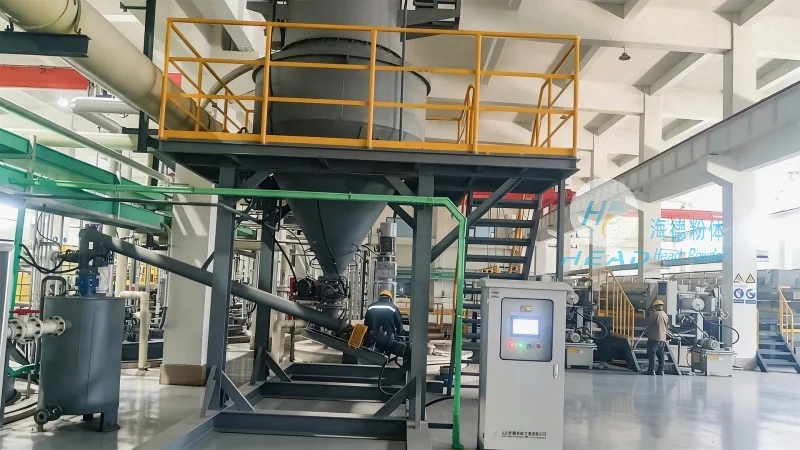
Efficiency and reliability are paramount in any working scene. The systems must be able to handle varying powder properties, such as different particle sizes, moisture content, or flowability, without compromising performance. Advanced control systems, including sensors and automation, are often integrated to monitor and adjust parameters in real-time, ensuring optimal operation. Additionally, safety features like emergency stop buttons, pressure relief valves, and dust suppression systems are standard to protect operators and the environment.
White gray powder conveying systems play a vital role in modern industrial operations, offering efficient and reliable solutions for material transport. The principles and working characteristics of these systems are tailored to meet the diverse needs of various industries, from construction to pharmaceuticals. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality conveying systems that adhere to industry standards and customer requirements. With a focus on innovation and customer satisfaction, HeadPowder ensures that their systems are durable, efficient, and suitable for a wide range of working environments.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top