With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Bicarbonate of soda, also known as sodium bicarbonate, is a widely used chemical in various industries. The efficient transportation of this material from one location to another is crucial for industrial processes. Pneumatic conveying systems offer a reliable and effective solution for handling bicarbonate of soda, ensuring smooth operation and minimal downtime. This article explores the underlying principles of such equipment and highlights key working scene characteristics that make it suitable for different industrial applications.
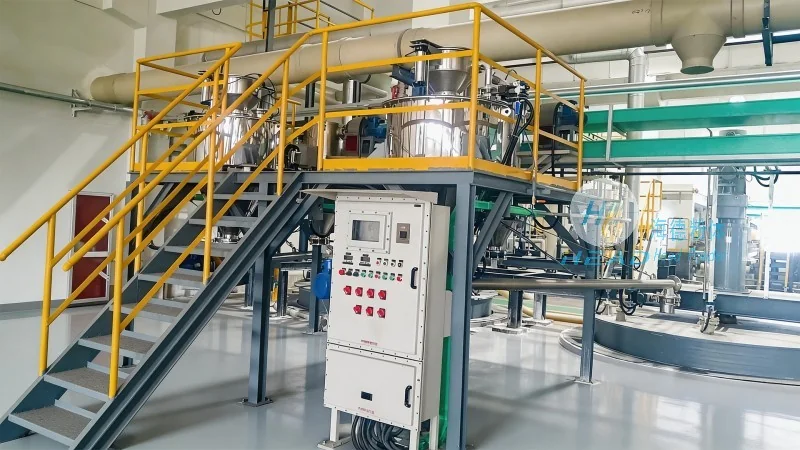
Pneumatic conveying, or air conveying, is a method of transporting bulk materials through a pipeline using compressed air. In the case of bicarbonate of soda, the system typically operates by creating a pressure differential between the material source and the destination. The equipment uses a blower or compressor to generate airflow, which draws the powder into the pipeline. The velocity of the air is carefully controlled to ensure the material is conveyed without causing excessive wear or degradation. The system may employ different types of conveying, such as dilute phase or dense phase, depending on the material characteristics and distance to be covered. For bicarbonate of soda, which is a fine powder, a dilute phase system is often preferred as it allows for efficient and low-cost transportation over moderate distances. The principle involves the interaction between the air flow and the powder particles, where the air provides the necessary force to move the material through the pipeline. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and improving safety in the workplace.

The working scene characteristics of bicarbonate of soda pneumatic conveying equipment are tailored to meet the specific demands of industrial environments. One of the primary characteristics is its ability to handle fine powders without clogging or blockages. The design of the equipment, including the inlet and outlet configurations, is optimized to prevent material accumulation and ensure consistent flow. Another important characteristic is the system's adaptability to different production scales. Whether used in small-scale laboratory settings or large-scale industrial plants, the equipment can be scaled to accommodate varying material volumes. The working scene also considers the environmental factors, such as dust control and noise reduction. Modern pneumatic conveying systems incorporate dust collection and filtration mechanisms to maintain a clean working environment and comply with environmental regulations. Additionally, the equipment is designed for easy integration into existing production lines, minimizing the need for extensive modifications to the facility. This adaptability makes it a versatile solution for various industries, including food processing, pharmaceuticals, and chemical manufacturing.
The application scenarios for bicarbonate of soda pneumatic conveying equipment span across multiple industries. In the food industry, it is commonly used for transporting baking soda in baking and confectionery production. The equipment ensures that the powder is delivered to mixing and processing units without contamination or loss. In the pharmaceutical sector, the system is employed to transport raw materials for the production of medications, maintaining strict hygiene standards. The dense phase conveying option is particularly useful here to prevent product degradation and ensure consistent quality. In chemical manufacturing, the equipment is used for handling bicarbonate of soda in production lines, where precise control over the material flow is essential. The operational efficiency of the system is a critical factor in these scenarios. The ability to convey material quickly and reliably reduces production time and increases overall productivity. Furthermore, the low maintenance requirements of pneumatic conveying systems contribute to cost savings over the long term. The system's reliability is enhanced by the use of high-quality components and regular maintenance schedules, ensuring minimal downtime and consistent performance. This operational efficiency makes the equipment a preferred choice for industries that require continuous and uninterrupted production processes.
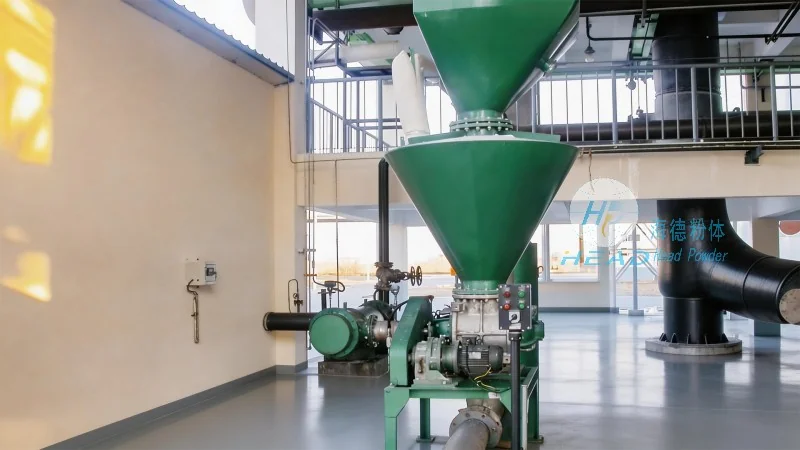
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of pneumatic conveying systems for various bulk materials. With a focus on providing tailored solutions for industries handling bicarbonate of soda and other fine powders, the company leverages years of experience and advanced technology to deliver high-performance equipment. The company's headquarters is located in Shandong, China, where it maintains a state-of-the-art manufacturing facility equipped with the latest design and testing equipment. The team of engineers and technicians at headpowder is dedicated to understanding the unique requirements of each client and developing customized solutions that meet their specific needs. Technical support and after-sales service are provided to ensure the equipment operates at optimal levels throughout its lifecycle. The company adheres to international quality standards and complies with relevant regulations, ensuring the safety and reliability of its products. By partnering with headpowder, industries can benefit from reliable pneumatic conveying systems that enhance their operational efficiency and reduce material handling costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top