With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Calcium hydroxide, commonly known as slaked lime, is a widely used chemical in various industrial and construction applications. The efficient and reliable transport of this powder is crucial for maintaining production efficiency and ensuring product quality. Pneumatic conveying systems have emerged as a preferred solution for handling calcium hydroxide powder due to their ability to transport materials in a dust-free environment, reducing operational hazards and improving process control. This article explores the fundamental principles behind calcium hydroxide powder pneumatic conveying systems and highlights the key working scene characteristics that make them suitable for diverse industrial applications.
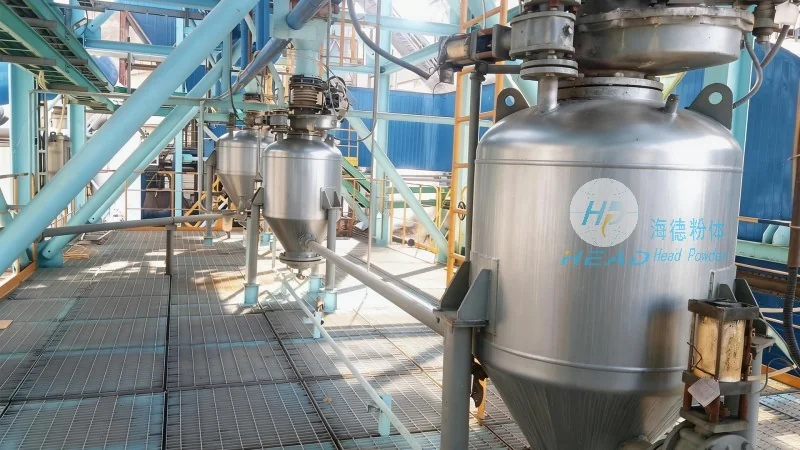
Pneumatic conveying is a method of transporting bulk materials through a pipeline using a stream of air or other gas. In the context of calcium hydroxide powder, this technology involves the use of a positive pressure or negative pressure system to move the powder from a source to a destination. The positive pressure system, also known as a pressure system, uses a blower or compressor to generate air pressure that pushes the powder through the pipeline. Conversely, the negative pressure system, or vacuum system, uses a vacuum pump to create a suction effect that draws the powder into the pipeline. Both systems have their advantages and are selected based on the specific requirements of the application, such as the distance to be covered, the volume of material to be transported, and the need for dust control.
A typical calcium hydroxide powder pneumatic conveying system consists of several critical components that work in tandem to ensure smooth and efficient operation. These components include the material feed hopper, which holds the calcium hydroxide powder and regulates the flow rate; the conveying line, which is a sealed pipeline that transports the powder; the air supply system, which provides the necessary air pressure or vacuum; and the separation and collection equipment, which separates the powder from the air at the receiving end. Additionally, the system may include a filter system to capture any fine particles that escape during the conveying process, ensuring compliance with environmental regulations and maintaining a clean working environment.
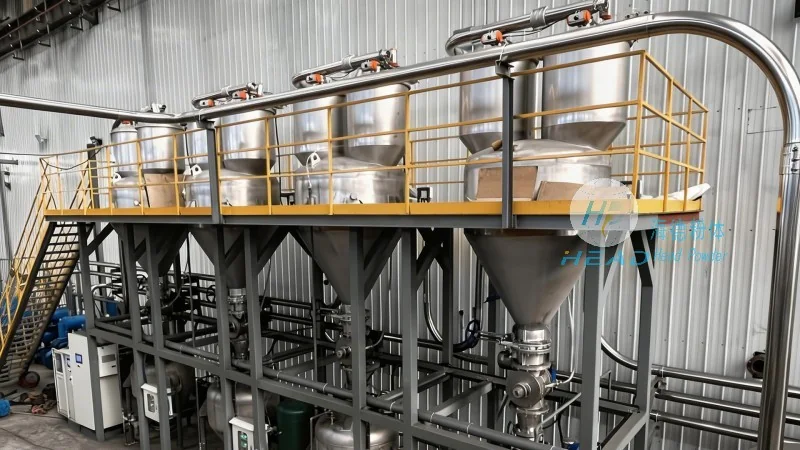
The operation of a calcium hydroxide powder pneumatic conveying system is based on the principle of fluidization and suspension. When air is introduced into the conveying line at a sufficient velocity, it creates a fluidized bed of powder, where the particles are suspended in the air stream. This suspension allows the powder to be transported through the pipeline without the need for mechanical components like belts or buckets. The velocity of the air is carefully controlled to ensure that the powder particles remain suspended without being damaged or agglomerated. The system's design ensures that the air velocity is maintained above the minimum fluidization velocity, which is the critical velocity required to keep the powder particles in a fluidized state. This principle allows for the efficient and gentle transport of calcium hydroxide powder, preserving its quality and preventing caking or degradation.
The working scene characteristics of calcium hydroxide powder pneumatic conveying systems are tailored to meet the specific demands of various industrial applications. These characteristics include the ability to handle large volumes of material, the flexibility to transport powder over long distances, and the capability to operate in both positive and negative pressure modes. The systems are designed to be compact and space-efficient, making them suitable for installation in confined spaces such as industrial plants or construction sites. Additionally, the systems are equipped with advanced control systems that allow for real-time monitoring of the conveying process, enabling operators to adjust parameters such as air pressure and flow rate to optimize performance. The dust-free operation of the system is a significant advantage, as it reduces the risk of respiratory hazards and minimizes the need for additional dust suppression measures. This characteristic makes the system particularly suitable for applications where product purity and worker safety are paramount, such as in the food processing, pharmaceutical, and construction industries.
Calcium hydroxide powder pneumatic conveying systems are widely used in various industries due to their versatility and efficiency. In the construction industry, these systems are used to transport calcium hydroxide for mortar and concrete production, ensuring consistent material quality and reducing the risk of contamination. In the chemical industry, the systems are used to handle calcium hydroxide in the production of other chemicals, such as calcium chloride and calcium carbonate. The pharmaceutical industry also utilizes these systems for the transport of calcium hydroxide in the manufacturing of calcium supplements and other medicinal products. Each application requires a customized system design to meet the specific requirements of the process, including the material's particle size, moisture content, and handling requirements.
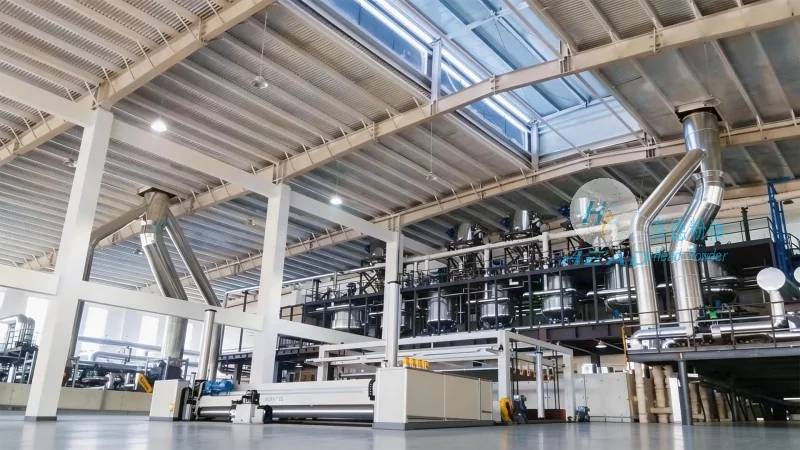
There are several advantages to using calcium hydroxide powder pneumatic conveying systems over traditional methods such as bucket elevators or belt conveyors. One of the primary advantages is the ability to operate in a dust-free environment, which enhances worker safety and reduces the risk of product contamination. The systems are also more flexible and can be easily reconfigured to accommodate changes in production volume or process requirements. Additionally, the systems are more energy-efficient compared to mechanical conveyors, as they use less power to transport the same amount of material. The gentle handling of the powder by the air stream also helps to preserve the material's quality, reducing the risk of caking or degradation. Finally, the systems are more compact and require less space for installation, making them suitable for installation in confined areas.
Calcium hydroxide powder pneumatic conveying systems are a reliable and efficient solution for transporting calcium hydroxide powder in various industrial applications. The systems are based on proven pneumatic conveying technology and are designed to meet the specific requirements of different industries. The working scene characteristics of these systems, including their dust-free operation, flexibility, and energy efficiency, make them a preferred choice for many applications. As a leading provider of engineering solutions for bulk material handling, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to the needs of its clients. With a focus on quality and innovation, the company has established itself as a trusted partner in the industry, providing reliable and efficient solutions for the transport of calcium hydroxide powder and other bulk materials. Based in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. leverages its expertise and experience to deliver high-performance pneumatic conveying systems that meet the highest standards of safety, efficiency, and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top