With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for organic fertilizer granules. Our systems are engineered to meet the unique challenges of transporting bulk organic fertilizers efficiently and reliably, ensuring minimal product degradation and optimal operational performance.
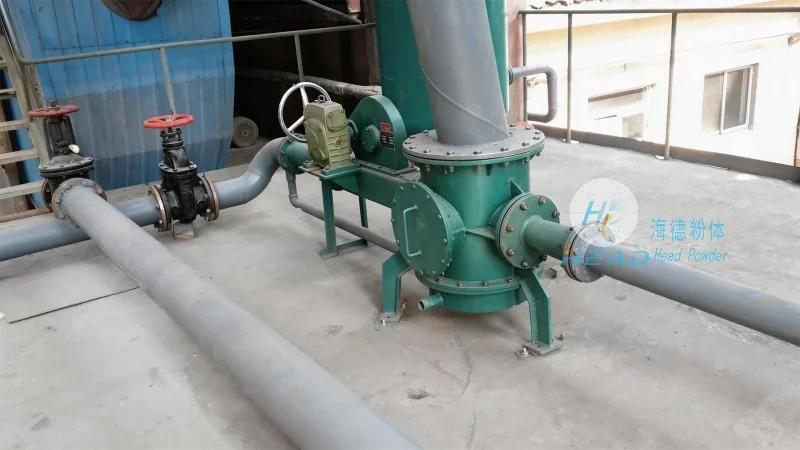
Our organic fertilizer granule pneumatic conveying system is a comprehensive solution designed to handle the transportation of granular organic fertilizers from storage silos to processing or packaging facilities. The system integrates several key components that work in tandem to ensure smooth and efficient material flow. These components include a high-capacity hopper for material storage, a rotary valve for controlled discharge, a pneumatic conveying pipeline network, and a receiver for final material deposition. Each component is selected and sized based on the specific characteristics of the organic fertilizer, such as particle size, moisture content, and bulk density, to optimize system performance and minimize operational issues.
Compared to traditional mechanical conveying methods, pneumatic conveying offers several distinct advantages when handling organic fertilizer granules. Firstly, it provides a completely enclosed system, which is crucial for maintaining product hygiene and preventing contamination from external sources. This is particularly important for organic fertilizers, which are often sensitive to moisture and microbial growth. Secondly, pneumatic systems can handle a wide range of particle sizes and shapes without the risk of blockages or wear on equipment, as seen in screw or belt conveyors. Thirdly, the system's flexibility allows for multiple delivery points from a single source, enabling efficient distribution to various processing or packaging lines. Additionally, the reduced need for mechanical parts minimizes maintenance requirements and operational downtime, leading to lower long-term costs and higher overall system reliability.
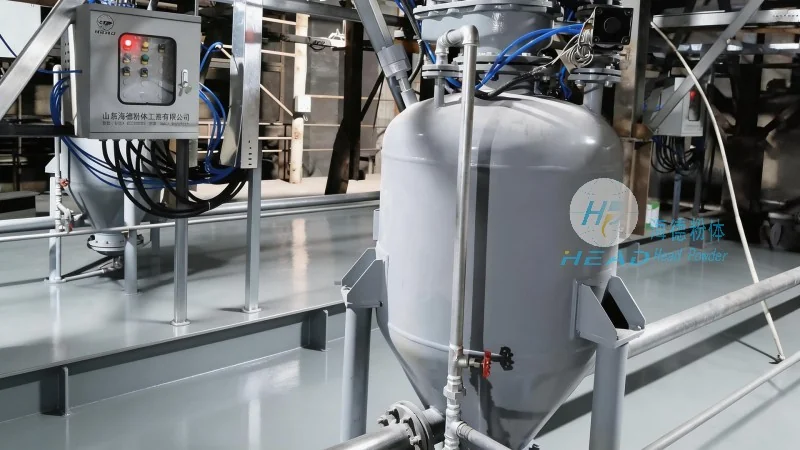
HeadPowder understands that each fertilizer production facility has unique operational requirements. Therefore, our pneumatic conveying systems are highly customizable to meet specific project needs. We offer a range of system configurations, from low-pressure to high-pressure designs, depending on the distance and elevation changes required for material transport. The system can be scaled to accommodate varying production capacities, from small-scale batch operations to large-scale continuous production lines. Furthermore, we provide integration services to connect the conveying system with existing plant infrastructure, ensuring seamless operation without disrupting current production processes. Our engineering team works closely with clients to assess their specific needs, develop tailored system solutions, and provide detailed design documentation and support throughout the project lifecycle.
The installation and commissioning of our organic fertilizer granule pneumatic conveying system follow a rigorous and systematic process to ensure optimal performance and safety. The process begins with a thorough site assessment to identify the optimal locations for the hopper, pipeline routing, and receiver. This assessment considers factors such as existing infrastructure, space constraints, and material flow patterns. Once the site is prepared, the components are installed according to the detailed engineering drawings. The hopper and rotary valve are positioned to ensure proper material flow and minimize the risk of bridging or segregation. The pipeline network is installed with appropriate supports and insulation to prevent heat loss or condensation, which could affect the organic fertilizer's properties. After installation, the system undergoes a series of tests, including air leak tests, pressure tests, and material flow tests, to verify that all components are functioning correctly and that the system meets the specified performance criteria. Commissioning is performed by our experienced technicians who conduct operational checks, adjust system parameters, and provide training to the client's staff to ensure they can operate and maintain the system effectively. This comprehensive approach ensures that the system is ready for full-scale operation as soon as possible, minimizing downtime and maximizing productivity.
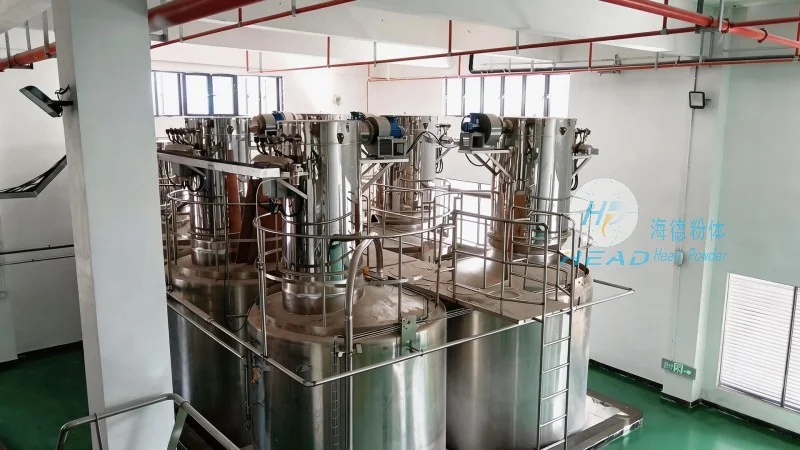
Proper maintenance is essential to ensure the long-term reliability and efficiency of the organic fertilizer granule pneumatic conveying system. HeadPowder offers comprehensive maintenance and support services to help clients keep their systems in optimal condition. Our maintenance programs include regular inspections, preventive maintenance tasks, and scheduled component replacements to minimize the risk of unexpected failures. We provide spare parts and replacement components that are specifically designed for our systems, ensuring compatibility and optimal performance. Our technical support team is available to provide assistance with troubleshooting, system adjustments, and operational guidance. In addition, we offer training programs for clients' staff to enhance their understanding of the system's operation and maintenance procedures. This proactive approach to maintenance helps to extend the system's lifespan, reduce operational costs, and ensure consistent performance over time.
One of our recent projects involved the installation of a pneumatic conveying system for an organic fertilizer production plant in Shandong, China. The plant required a system to transport granular organic fertilizer from storage silos to the packaging line, covering a distance of approximately 200 meters with a vertical lift of 15 meters. The system was designed to handle a production capacity of 50 tons per hour. During the installation and commissioning phase, our team worked closely with the plant's operations team to ensure that the system was integrated smoothly with existing equipment. The system was tested and optimized to achieve the required flow rates and pressure levels. After commissioning, the system has been operating reliably, with minimal downtime and consistent material flow. The plant has reported significant improvements in operational efficiency and product quality, as the enclosed system has helped to maintain the fertilizer's moisture content and prevent contamination. This success highlights the effectiveness of our pneumatic conveying systems in meeting the specific needs of fertilizer production facilities and delivering measurable benefits to our clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top