

Working Principle and Features of Powder Bin Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in advanced solutions for powder handling and material transport. This article explores the working principle and key characteristics of powder bin pneumatic conveying systems, providing insights into how these systems efficiently manage bulk powder materials.
About Shandong HeadPowder Engineering Co., Ltd.
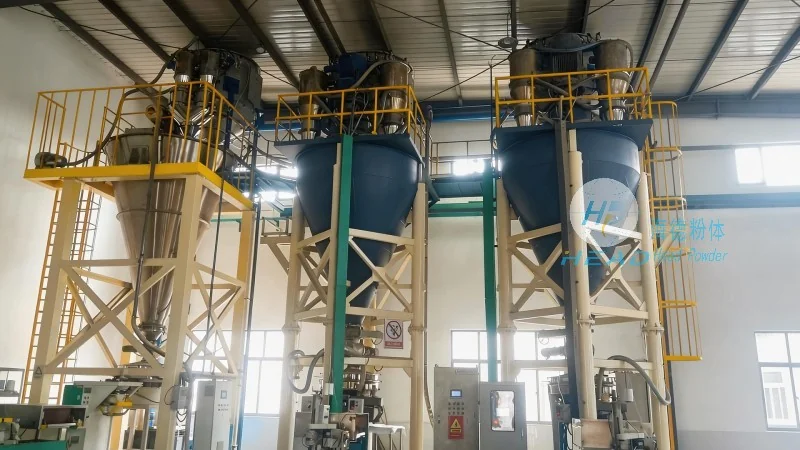
As a leading manufacturer in the field of powder engineering, Shandong HeadPowder Engineering Co., Ltd. is committed to delivering high-quality pneumatic conveying systems. The company focuses on innovation and customer satisfaction, establishing itself as a trusted partner for industries requiring reliable and efficient powder handling solutions. The company’s headquarters is located in Shandong, China, where it operates a state-of-the-art production facility and research center.
Working Principle of Powder Bin Pneumatic Conveying
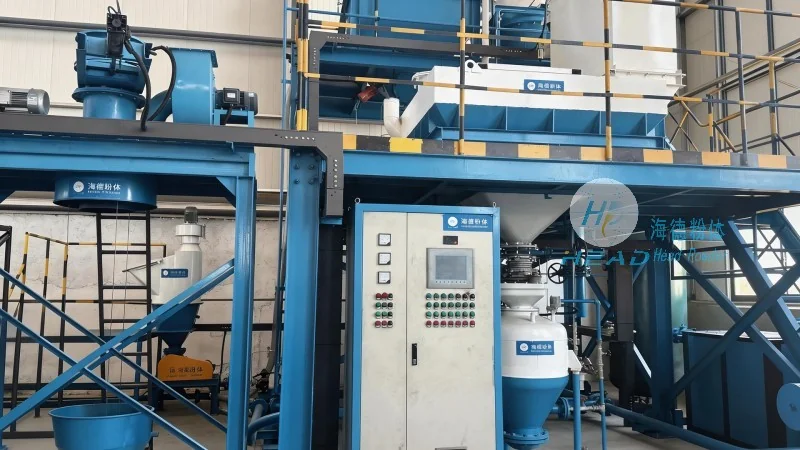
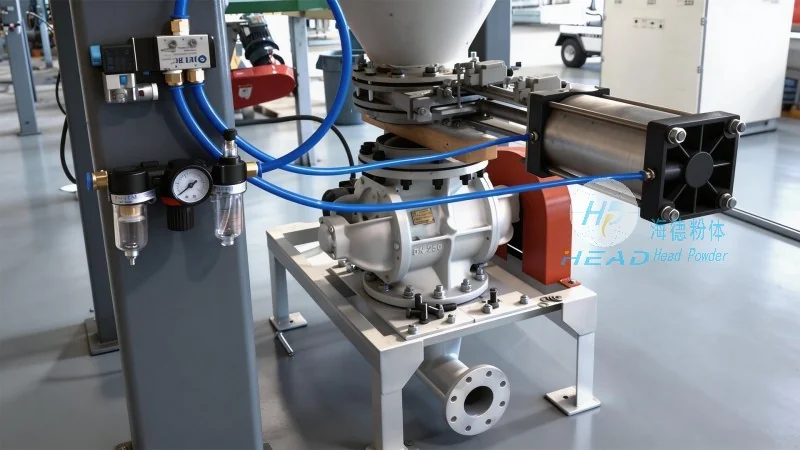
Powder bin pneumatic conveying systems operate on the principle of transporting bulk powder materials using compressed air or vacuum. The system typically includes a powder bin, a conveying line, and a receiver or discharge point. The process starts with powder being drawn from the bin by the air flow. As the air moves through the conveying line, it creates a low-pressure zone that pulls the powder particles along with it. This air-powder mixture travels through the pipeline to the destination, where it is separated from the air and deposited into the receiver. The working principle involves several key components: the bin’s design, the air supply system, and the pipeline configuration. The bin is equipped with a hopper and a discharge valve that controls the flow of powder into the conveying line. The air supply system provides the necessary pressure or vacuum to move the powder, while the pipeline ensures efficient transport of the air-powder mixture. The receiver at the end of the line collects the powder and may include a filter to remove any residual particles from the air stream.
Key Features of Powder Bin Pneumatic Conveying Systems
Powder bin pneumatic conveying systems offer several advantages suitable for diverse industrial applications. One primary feature is their high efficiency in transporting bulk powder over long distances. The systems can handle a wide range of powder types, including fine powders, granules, and even abrasive materials, without causing mechanical wear or damage to particles. Another key feature is the ability to maintain a closed system, which helps prevent dust emissions and ensures environmental compliance. The systems are designed for easy maintenance and operation, with components that are accessible and replaceable as needed. Additionally, the flexibility of pneumatic conveying allows for easy integration with existing production lines and equipment, reducing the need for major facility modifications. The systems are capable of handling varying flow rates and material characteristics, making them adaptable to different production requirements. Furthermore, the use of compressed air or vacuum provides a clean and hygienic transport method, which is especially important in industries such as food, pharmaceuticals, and chemicals where product purity is critical.
Applications and Benefits
The applications of powder bin pneumatic conveying systems span multiple industries. They are commonly used in the food and beverage industry for transporting ingredients like flour, sugar, and spices. In the pharmaceutical industry, these systems handle active pharmaceutical ingredients (APIs) and other powders requiring strict contamination control. The chemical industry also benefits from these systems when transporting raw materials and intermediates. The benefits of using these systems include improved safety, as the closed system reduces dust explosion risks and inhalation hazards. It also enhances productivity by eliminating manual powder handling, which is time-consuming and labor-intensive. The systems contribute to cost savings by reducing material loss and minimizing downtime from maintenance or equipment failure. Overall, the combination of efficiency, reliability, and flexibility makes powder bin pneumatic conveying systems a preferred choice for industries needing consistent and safe powder handling solutions.
Conclusion
In summary, powder bin pneumatic conveying systems are advanced and effective solutions for bulk powder transport. The working principle, which relies on air flow to move powder through a pipeline, ensures efficient and reliable operation. The key features—high efficiency, closed system operation, and adaptability—make these systems suitable for various industrial applications. Shandong HeadPowder Engineering Co., Ltd. continues to innovate in this field, providing customized solutions that meet clients’ specific needs. By understanding the working principle and features of these systems, industries can make informed decisions about implementing efficient powder handling solutions that enhance productivity and safety.