

Working Principle and Features of Dry Coffee Pneumatic Conveying Equipment
Efficient and hygienic material handling is crucial in the coffee processing industry, where maintaining product quality and ensuring operational reliability are top priorities. Among the various technologies available, dry coffee pneumatic conveying equipment stands out as a sophisticated solution for transporting coffee beans and ground coffee with precision and care. This article delves into the working principle and key features of such equipment, highlighting how it addresses the unique challenges of coffee handling while enhancing overall production efficiency.
Understanding the Working Principle of Dry Coffee Pneumatic Conveying Equipment
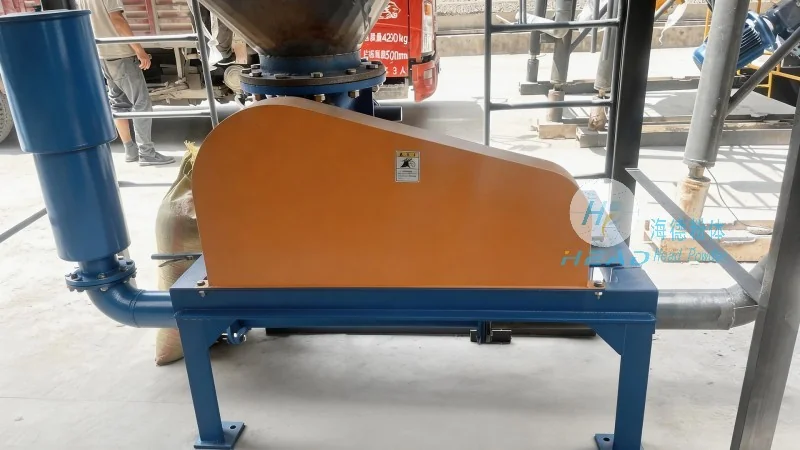
Dry coffee pneumatic conveying systems operate on the fundamental principle of using air to move dry materials through a sealed pipeline. The process typically involves two main modes: positive pressure and negative pressure, each tailored to specific operational needs and material characteristics. In positive pressure systems, a fan or blower generates high-pressure air that forces the coffee particles through the pipeline, ensuring consistent flow and preventing material degradation. Conversely, negative pressure systems create a vacuum that draws the coffee into the pipeline, which is often preferred for applications requiring gentle handling and minimal product impact. The choice between these modes depends on factors such as the type of coffee (whole beans or ground), the distance of transport, and the desired level of product protection.
At the core of the system is the hopper or feeder, which holds the coffee and releases it into the pipeline in controlled quantities. This component is critical for maintaining a steady flow and preventing blockages or uneven distribution. The pipeline itself is usually made of stainless steel or other food-grade materials to ensure compliance with hygiene standards and to resist corrosion from coffee oils and moisture. Along the pipeline, various components like cyclones, filters, and silos are integrated to separate air from the coffee, clean the air, and store the material, respectively. The entire system is designed to minimize product loss, maintain consistent moisture levels, and prevent contamination, all of which are essential for preserving the quality of coffee products.
Key Features and Advantages of Dry Coffee Pneumatic Conveying Equipment
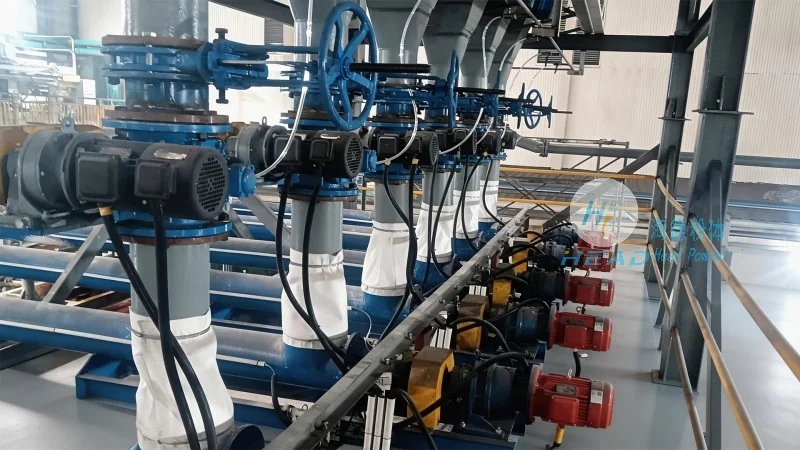
One of the most significant advantages of dry coffee pneumatic conveying equipment is its ability to handle dry, free-flowing materials like coffee beans and ground coffee without the need for mechanical components that could cause wear or damage. This design reduces maintenance costs and extends the lifespan of the equipment, making it a cost-effective solution for long-term use. Additionally, the sealed pipeline system eliminates the risk of cross-contamination between different batches of coffee, ensuring that each product maintains its unique flavor profile and quality characteristics.
Another key feature is the system's flexibility in terms of layout and integration. Unlike traditional belt or bucket elevators, pneumatic conveying systems can be easily reconfigured to accommodate changes in production volume or facility layout. This adaptability is particularly valuable in coffee processing plants, where production schedules and product lines may evolve over time. The equipment also offers excellent control over the conveying speed and pressure, allowing operators to adjust the flow rate based on real-time production needs and to prevent overloading or underloading of downstream processes.
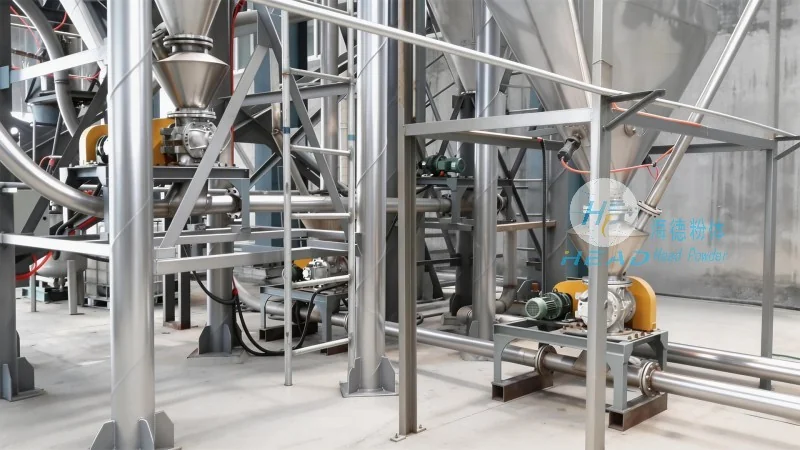
Hygiene and sanitation are paramount in the food industry, and dry coffee pneumatic conveying equipment excels in this area. The stainless steel construction and sealed design prevent dust accumulation and make cleaning and maintenance straightforward. Regular cleaning protocols can be easily implemented, ensuring that the equipment remains in compliance with food safety regulations. Furthermore, the absence of moving parts in contact with the coffee reduces the risk of mechanical damage or contamination, which is critical for maintaining the integrity of high-value coffee products.
About Shandong HeadPowder Engineering Co., Ltd.
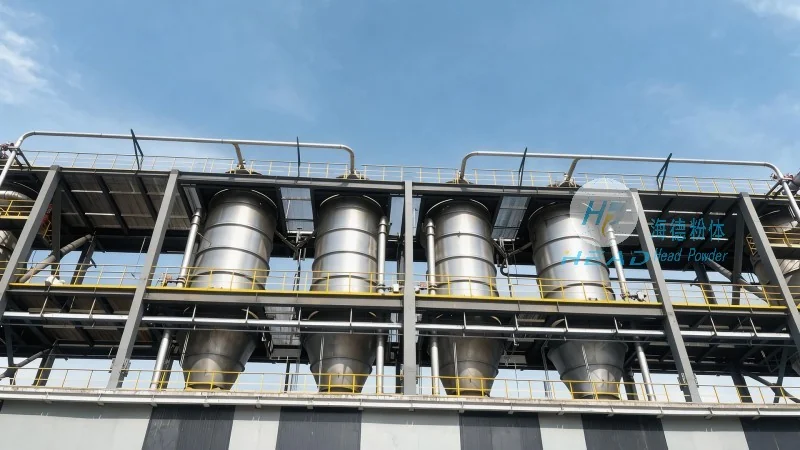
As a leading manufacturer of industrial conveying solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized dry coffee pneumatic conveying equipment tailored to the specific needs of coffee processing facilities. With years of experience in the industry, the company has developed a deep understanding of the unique challenges faced by coffee producers, from maintaining product quality to optimizing operational efficiency. HeadPowder's equipment is designed and manufactured with precision engineering, using high-quality materials and advanced technology to ensure reliability, durability, and performance.
HeadPowder is committed to delivering solutions that not only meet but exceed industry standards. The company's products are backed by rigorous testing and quality control processes, ensuring that each unit is built to withstand the demands of continuous operation in coffee processing environments. With a focus on customer satisfaction and long-term partnerships, HeadPowder provides comprehensive support, including installation, maintenance, and technical assistance, to help coffee producers maximize the performance of their conveying systems. HeadPowder's headquarters is located in Shandong, China, where the company leverages its local expertise and resources to serve clients both domestically and internationally.