With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
This section provides an overview of bin pump material pneumatic conveying systems, which are widely used in industrial applications for transporting bulk materials over long distances or through complex layouts. The system combines the principles of pneumatic conveying with the functionality of a bin pump to achieve efficient material handling. These systems are particularly valuable in industries where traditional bulk material transport methods, such as belt conveyors or bucket elevators, may be impractical due to space constraints, material characteristics, or the need for flexible operation.
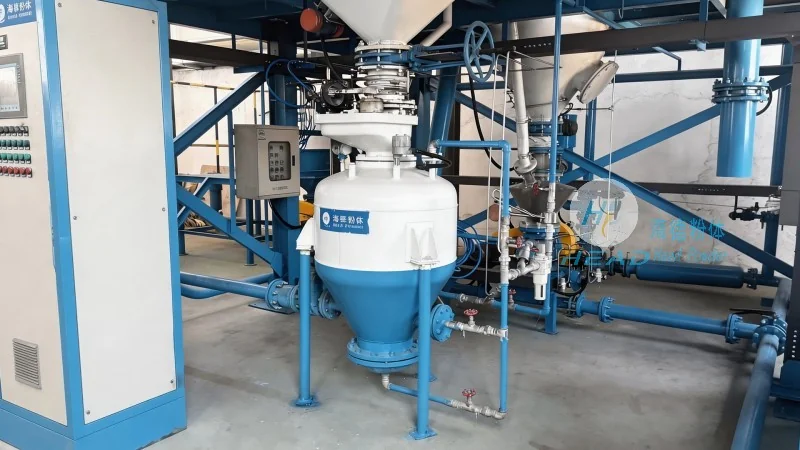
Bin pump material pneumatic conveying is a technology that utilizes a bin pump as the primary transport device, coupled with a pneumatic conveying system to move bulk materials from a storage bin to a processing or discharge point. This method is especially effective for materials that are difficult to handle by conventional means, including powders, granules, fine particles, and even some bulk solids with high moisture content or abrasive properties. The system operates by creating a pressure differential within the conveying line, which draws the material from the bin into the pump and then transports it to the destination. The bin pump, often referred to as an airlock or rotary valve, acts as a controlled discharge mechanism, ensuring a steady and controlled flow of material into the pneumatic line.
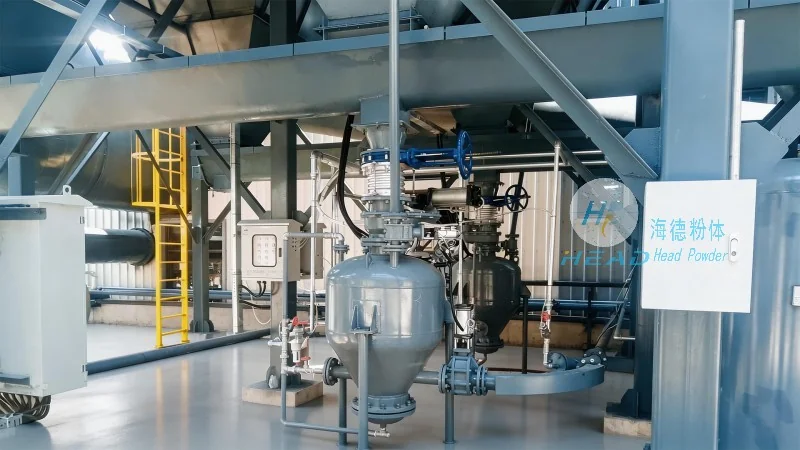
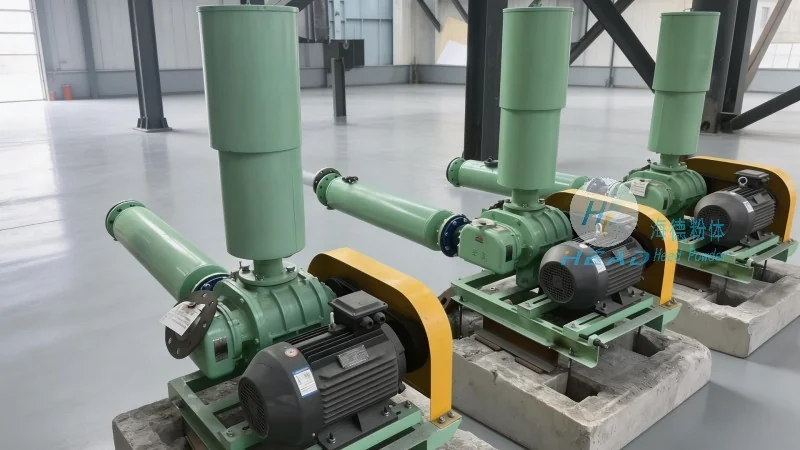
The core components of a bin pump material pneumatic conveying system include the storage bin, the bin pump (airlock), the pneumatic conveying line, and the air compressor. The storage bin holds the bulk material, typically in a hopper or silo, and provides a consistent supply of material to the system. The bin pump is positioned at the bottom of the bin and functions as a controlled discharge device, releasing material into the conveying line under pressure. The air compressor generates the necessary air pressure to move the material through the line, creating a flow of air and material. The working principle involves the bin pump rotating to create a vacuum or pressure that pulls the material into the pump chamber. Once the chamber is filled, the pump rotates to push the material through the outlet into the conveying line, where compressed air propels it to the destination. This process is repeated continuously, ensuring a steady flow of material.
The design of bin pump material pneumatic conveying systems follows several key principles to ensure optimal performance, reliability, and energy efficiency. First, the selection of the appropriate bin pump size and type is critical, as it must match the material characteristics (e.g., particle size distribution, flowability, angle of repose, and moisture content) and the required conveying capacity. For example, cohesive or sticky materials may require a larger pump with a higher rotation speed to ensure proper discharge. Second, the air-to-material ratio is a crucial design parameter, as it determines the efficiency of the conveying process and the energy consumption. A higher air-to-material ratio can increase conveying speed but may also lead to higher energy costs and potential material degradation due to excessive air flow. Engineers typically optimize this ratio based on the material's properties and the system's layout. Third, the system layout, including the length and diameter of the conveying line, must be carefully designed to minimize pressure losses and ensure smooth material flow. The line diameter is usually selected based on the material's particle size and the required flow rate, while the length is constrained by the maximum pressure drop that the system can handle. Additionally, the inclusion of filters and cyclones in the system helps to maintain air quality and prevent material buildup in the conveying line, reducing maintenance requirements and improving overall system performance.
Bin pump material pneumatic conveying systems are widely used in various industrial sectors, including chemical, pharmaceutical, food, mining, and cement. They are particularly suitable for applications that require the transport of materials over long distances, through vertical or horizontal layouts, or into elevated storage tanks. For instance, in chemical plants, these systems are used to convey raw materials from storage silos to processing units, while in food processing facilities, they transport ingredients like flour or sugar to mixing and packaging equipment. The benefits of this technology include high conveying efficiency, low maintenance requirements, and the ability to handle a wide range of materials. Compared to traditional methods like belt conveyors or bucket elevators, pneumatic conveying systems are more flexible and can be easily integrated into existing facilities. They also offer the advantage of a closed-loop operation, which reduces dust emissions and improves workplace safety by containing material within the system. Furthermore, the system can operate continuously without the need for manual intervention, increasing productivity and reducing labor costs.
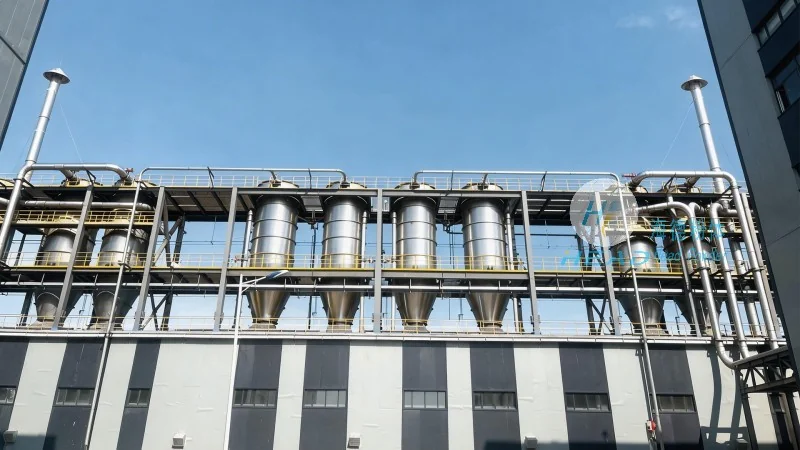
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of bin pump material pneumatic conveying systems. With years of experience in the industry, the company specializes in providing customized solutions tailored to the specific needs of its clients. HeadPowder's product line includes a range of bin pumps, pneumatic conveying lines, and related accessories, all designed and manufactured using advanced technology and high-quality materials to ensure reliability and durability. The company's team of engineers and technicians work closely with clients to understand their material handling requirements, process flow, and operational constraints, and develop optimal solutions that meet their specific needs. HeadPowder is committed to quality and customer satisfaction, with a focus on delivering systems that are efficient, cost-effective, and easy to maintain. The company's headquarters is located in Shandong, China, and it serves clients both domestically and internationally, with a reputation for excellence in the material handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top