

What is High-Pressure Bin Pump Powder Pneumatic Conveying? And What Are Its Design Principles?
High-pressure bin pump powder pneumatic conveying is a specialized method used in industrial settings to transport bulk solid materials through a pipeline system using compressed air or other gas as the conveying medium. This technology is particularly effective for handling fine powders and granular materials, offering advantages such as low maintenance, high efficiency, and the ability to transport materials over long distances without the need for mechanical components like screws or belts. The system typically involves a storage bin, a high-pressure pump, and a pipeline network, making it suitable for applications in sectors like chemical, pharmaceutical, food, and mining.
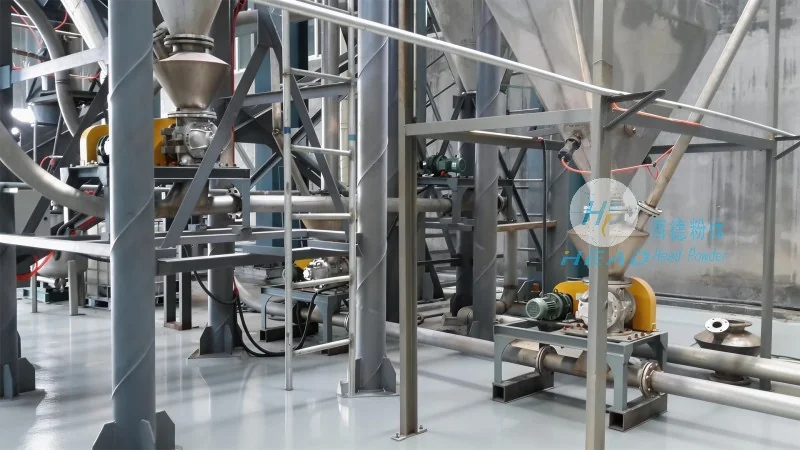
Core Components and Functionality
The high-pressure bin pump system consists of several key components that work in tandem to ensure reliable material transport. The storage bin, often equipped with a hopper and a discharge valve, holds the bulk material. The high-pressure pump, which is the heart of the system, generates the necessary pressure to move the material through the pipeline. As the pump operates, it draws material from the bin and mixes it with the conveying gas, creating a slurry-like mixture that is then propelled through the pipeline to the destination point. The conveying gas, usually air or nitrogen, is pressurized to a level that ensures the material is transported efficiently without clogging or degradation.
Design Principles and Operational Considerations
The design of a high-pressure bin pump system is guided by several fundamental principles aimed at optimizing performance and reliability. One of the primary considerations is the selection of appropriate materials for the pump and pipeline components to withstand the high pressures and abrasive nature of the conveyed materials. The system's pressure rating is a critical design parameter, as it determines the maximum distance and volume of material that can be transported. Additionally, the design must account for the specific properties of the material being conveyed, including its density, flowability, and moisture content, to ensure proper feeding and prevent blockages. The control system, which regulates the pump's operation and the flow of the conveying gas, plays a vital role in maintaining consistent material transport and preventing overpressurization or underfeeding.
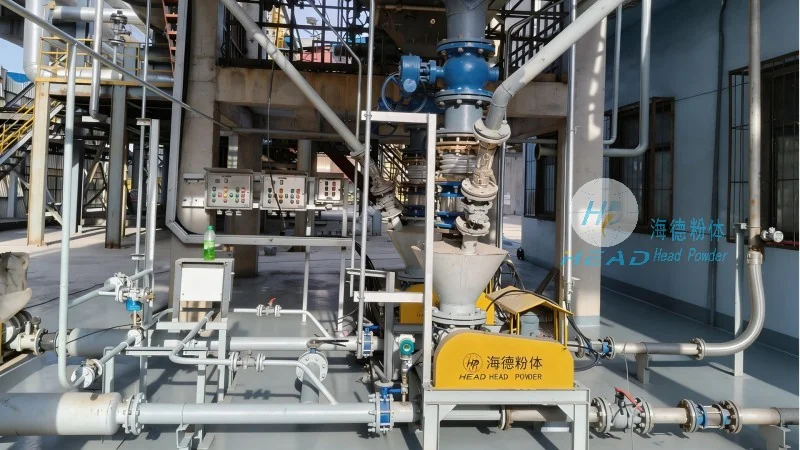
Advantages of High-Pressure Bin Pump Conveying
Compared to traditional conveying methods like vacuum or positive displacement systems, high-pressure bin pump pneumatic conveying offers several distinct advantages. It provides a more uniform and consistent flow of material, reducing the risk of segregation and ensuring that the material reaches the destination with minimal degradation. The system is also highly flexible, allowing for changes in the conveying route or material type without significant modifications. Furthermore, the absence of moving parts in the pipeline reduces maintenance requirements and extends the service life of the equipment. This makes it an ideal solution for applications where reliability and efficiency are paramount.
Applications in Industrial Settings
High-pressure bin pump systems are widely used in various industrial applications where the transport of bulk powders is essential. In the chemical industry, they are employed to move raw materials and finished products between processing units, ensuring a continuous and controlled flow. The pharmaceutical sector utilizes these systems for the handling of sensitive powders, maintaining strict hygiene and contamination control. In the food industry, high-pressure bin pumps are used to convey ingredients and finished products, adhering to food safety regulations. Additionally, the mining and mineral processing industries benefit from this technology for transporting ore and other bulk materials from storage bins to processing plants.
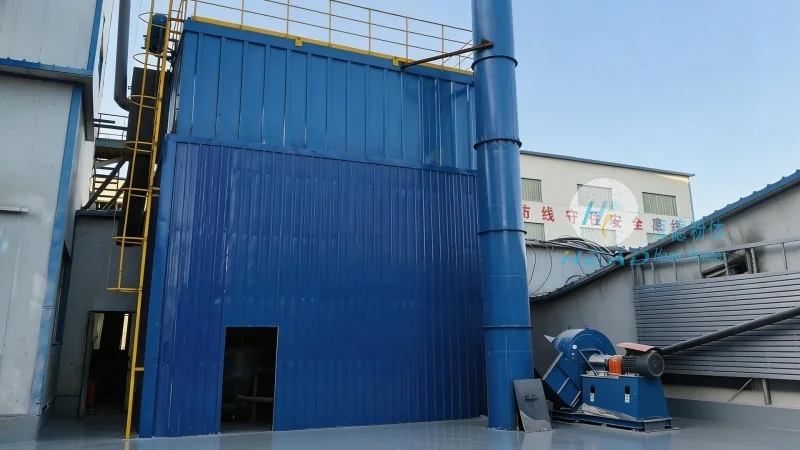
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of high-pressure bin pump systems and related pneumatic conveying equipment. With a focus on innovation and quality, the company has established itself as a trusted partner in the industry, providing customized solutions tailored to the specific needs of its clients. HeadPowder's products are designed to meet the highest standards of performance and reliability, ensuring that they deliver optimal results in demanding industrial environments. The company's commitment to research and development has enabled it to introduce advanced features and technologies that enhance the efficiency and effectiveness of its conveying systems.
Conclusion and Future Directions
High-pressure bin pump powder pneumatic conveying represents a sophisticated and efficient method for transporting bulk solid materials, offering significant advantages over traditional conveying technologies. As industrial demands for reliable and efficient material handling continue to grow, the importance of high-quality conveying systems like those offered by Shandong HeadPowder Engineering Co., Ltd. becomes increasingly evident. By adhering to rigorous design principles and leveraging advanced technologies, these systems provide a sustainable solution for the transport of powders and granular materials, supporting the productivity and success of various industrial operations.