

What is Dust-Free Powder Pneumatic Conveying? And What Are Its Design Principles?
Understanding dust-free powder pneumatic conveying systems is crucial for industries that handle fine powders, as these systems offer efficient, clean, and reliable methods for transporting materials. This article will explore the fundamental concepts of dust-free powder pneumatic conveying and delve into the core design principles that make such systems effective.
Introduction to Dust-Free Powder Pneumatic Conveying
Dust-free powder pneumatic conveying, also known as closed-loop or positive pressure conveying, is a technology used to transport dry powders and granules through a pipeline using air or other gases. Unlike traditional open systems that can lead to dust emissions and contamination, dust-free systems are designed to contain the material within a sealed environment, ensuring minimal environmental impact and product purity. This method is widely adopted in pharmaceutical, food, chemical, and other industries where product integrity and safety are paramount.
Key Components of a Dust-Free Powder Pneumatic Conveying System
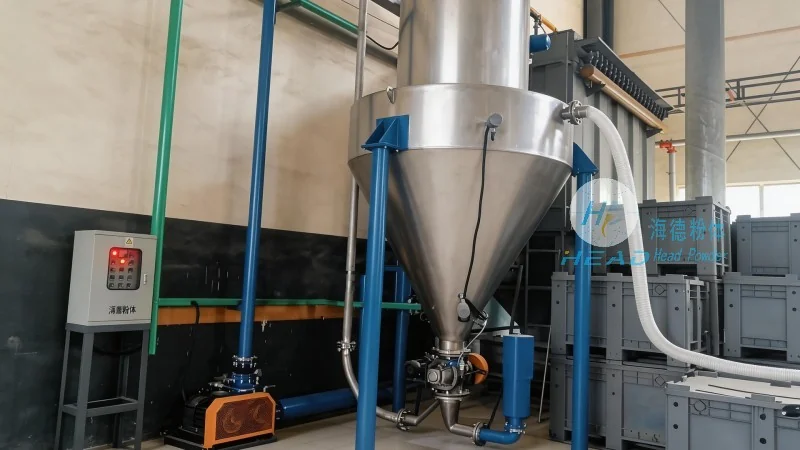
The effectiveness of a dust-free powder pneumatic conveying system relies on several critical components that work in tandem to ensure smooth operation. These components include the material feed hopper, which holds the powder and controls the flow rate; the conveyor line, typically made of stainless steel or other corrosion-resistant materials to prevent contamination; the air or gas source, such as a blower or compressor, which provides the necessary pressure to move the material; and the control valves and sensors that regulate the system's performance. Each component is carefully selected and integrated to maintain the dust-free environment throughout the conveying process.
Design Principles for Optimal Performance
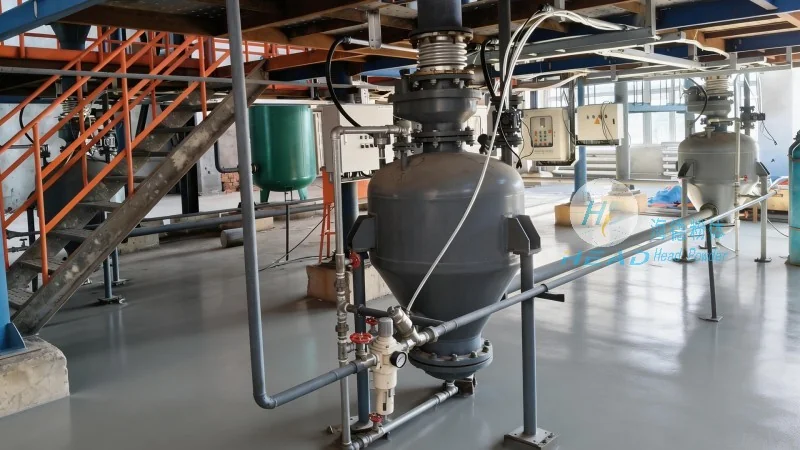
The design principles of dust-free powder pneumatic conveying systems are centered around efficiency, reliability, and product protection. One of the primary principles is maintaining a positive pressure within the system to prevent external air from entering and contaminating the material. This is achieved by using sealed hoppers, airlocks, and other containment devices that ensure the material remains within the system. Another key principle is the selection of appropriate air velocities and flow rates, which must be optimized to prevent material degradation or blockages. The system's design also considers the material's properties, such as particle size, density, and flowability, to determine the best conveying method (e.g., dilute phase or dense phase). Additionally, the use of stainless steel or other inert materials in the construction of the system helps to prevent chemical reactions or contamination from the environment.
Applications and Benefits of Dust-Free Powder Pneumatic Conveying
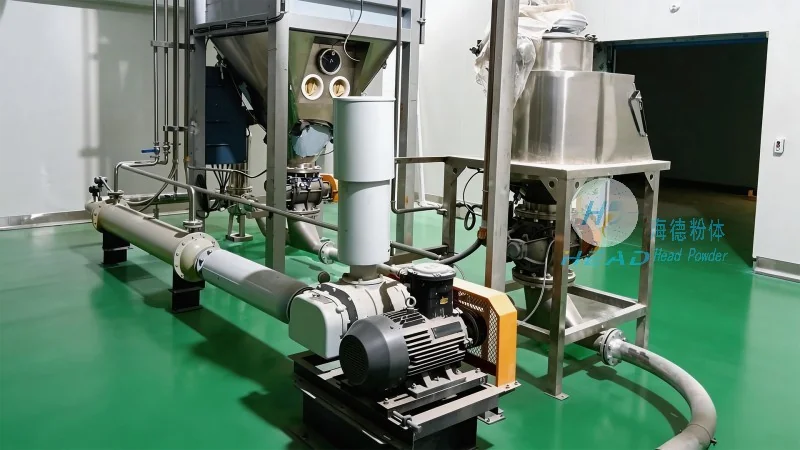
Dust-free powder pneumatic conveying systems are used in a wide range of applications across various industries. In the pharmaceutical industry, these systems are essential for transporting active pharmaceutical ingredients (APIs) and other sensitive materials, as they maintain product purity and prevent cross-contamination. In the food industry, they are used to convey ingredients like flour, sugar, and spices, ensuring that the final product is free from dust and contaminants. The chemical industry also benefits from these systems when handling hazardous or reactive powders, as they provide a safe and controlled environment for material transport. The primary benefits of dust-free powder pneumatic conveying include improved product quality, reduced environmental impact, increased operational efficiency, and enhanced safety for workers. By eliminating the need for manual handling and open storage, these systems also reduce the risk of dust explosions and other safety hazards.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of dust-free powder pneumatic conveying systems. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient material handling solutions. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. HeadPowder specializes in designing and manufacturing customized dust-free conveying systems tailored to the specific needs of its clients, ensuring that each system meets the highest standards of performance and safety. The company's commitment to customer satisfaction and product excellence has earned it a reputation as a leading provider in the industry.