With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Sugar processing is a critical industry that requires efficient and reliable equipment to handle raw materials and finished products. Among the essential machinery in this sector, sugar material handling equipment plays a pivotal role in ensuring smooth operations. This equipment is designed to transport, store, and manage sugar in various forms, from raw cane to refined crystals. Understanding the components and design principles of such equipment is crucial for optimizing production processes and maintaining product quality.
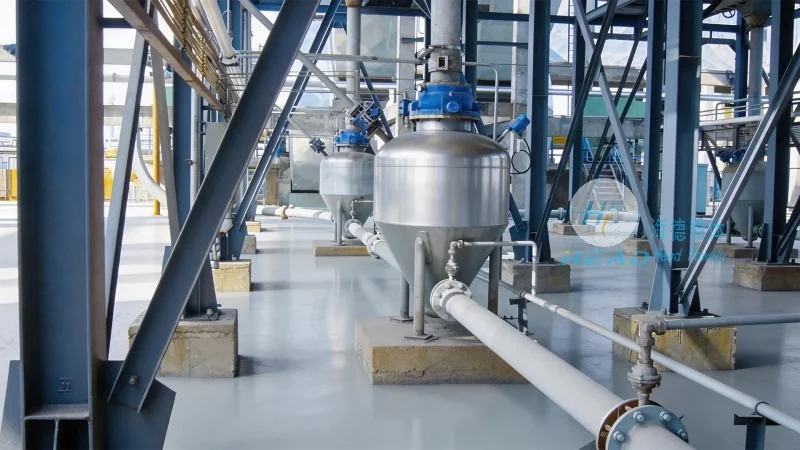
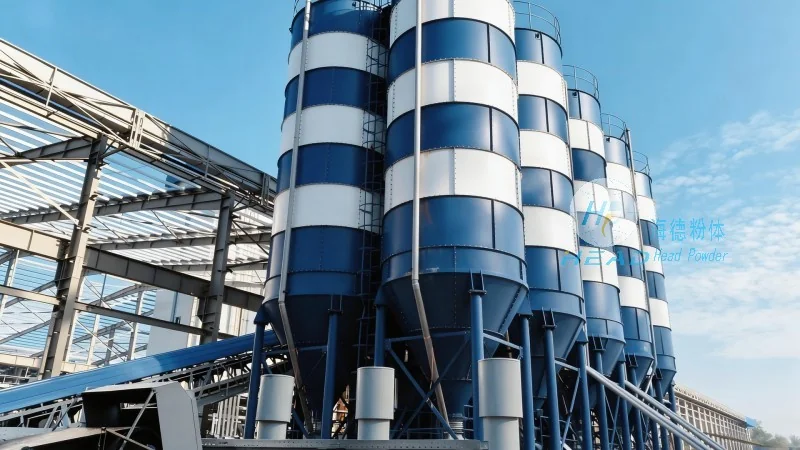
Sugar material handling systems typically consist of several key components that work in tandem to facilitate the movement of sugar. These components include conveyors, elevators, storage silos, and feeding mechanisms. Conveyors, such as belt conveyors or screw conveyors, are commonly used to transport bulk sugar over short to medium distances. Elevators, like bucket elevators or chain conveyors, are employed to lift sugar vertically, often from storage areas to processing units. Storage silos are essential for holding large quantities of sugar, providing a stable environment that prevents moisture and contamination. Feeding mechanisms, including rotary valves or screw feeders, regulate the flow of sugar into processing equipment, ensuring consistent and controlled input.
The design of sugar material handling equipment is guided by several key principles aimed at maximizing efficiency, durability, and safety. One of the primary principles is the minimization of product degradation. Sugar is hygroscopic and can easily absorb moisture, leading to clumping and quality issues. Therefore, equipment is designed with materials that are non-stick and resistant to moisture, such as stainless steel or food-grade plastics. Additionally, the design emphasizes low friction surfaces to prevent sugar crystals from adhering to equipment parts, which can cause blockages and reduce efficiency.
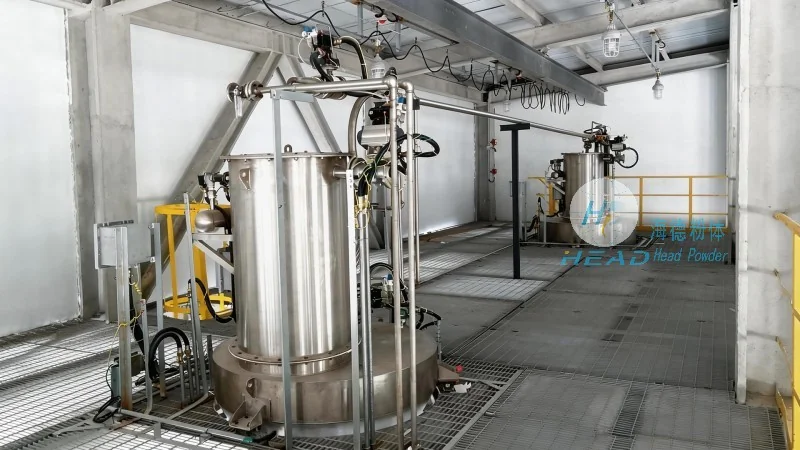
Another critical design principle is the prevention of contamination. Sugar handling equipment must be constructed to avoid cross-contamination between different types of sugar or between raw and processed materials. This is achieved through sealed systems, separate conveyor lines, and thorough cleaning protocols. The equipment is also designed to minimize dust generation, as sugar dust can be a fire hazard and affect air quality in processing facilities. Proper ventilation and dust collection systems are integrated into the design to mitigate these risks.
The choice of materials for sugar material handling equipment is a critical factor in its long-term performance and reliability. Stainless steel is a popular material due to its corrosion resistance, durability, and ease of cleaning. It is particularly suitable for handling refined sugar, which is more prone to contamination and requires a hygienic environment. For raw sugar or bulk cane sugar, materials like carbon steel with protective coatings may be used, as they can withstand the abrasive nature of the material. The equipment is also designed with smooth, rounded edges and internal surfaces to prevent the accumulation of sugar and facilitate cleaning. Regular maintenance, including lubrication and part replacement, is essential to ensure the equipment operates efficiently and extends its service life.
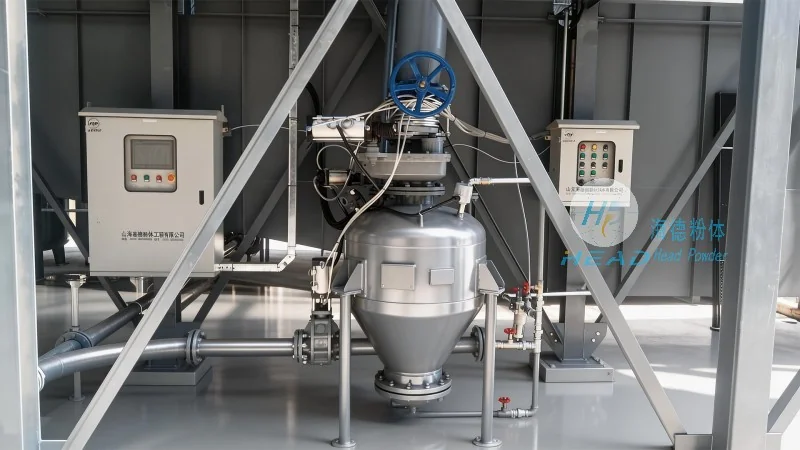
Sugar material handling equipment is not an isolated component but an integral part of the entire processing system. It must be seamlessly integrated with other machinery, such as sugar mills, evaporators, and crystallizers, to ensure a continuous flow of materials. The design of the equipment considers the specific requirements of each processing stage, such as the type of sugar being handled, the required flow rate, and the desired output. For example, in a sugar refining plant, the equipment must be capable of handling both raw sugar and refined crystals, with adjustable settings to accommodate different product specifications. The integration also involves coordinating with control systems, which monitor and regulate the flow of sugar, ensuring that the processing plant operates at optimal efficiency.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of sugar material handling equipment. Based in Shandong, China, the company specializes in designing and producing high-quality machinery tailored to the needs of the sugar industry. HeadPowder's expertise lies in understanding the unique challenges of sugar processing, such as the hygroscopic nature of sugar and the need for hygienic, efficient equipment. The company's products are designed with the latest technology and materials to ensure durability, reliability, and compliance with industry standards. HeadPowder provides comprehensive solutions, including custom-designed equipment, installation, and maintenance services, to help sugar processing plants optimize their operations and improve product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top