

What is a Shredded Paper Powder Conveying System? And What Are Its Design Principles?
Shredded paper powder conveying systems are specialized equipment designed to handle and transport finely processed paper waste into processing or recycling facilities. These systems are critical in industries that rely on paper recycling, as they ensure efficient movement of the shredded material from collection points to processing units. The design of such systems involves several key components and principles that work together to achieve optimal performance and reliability.
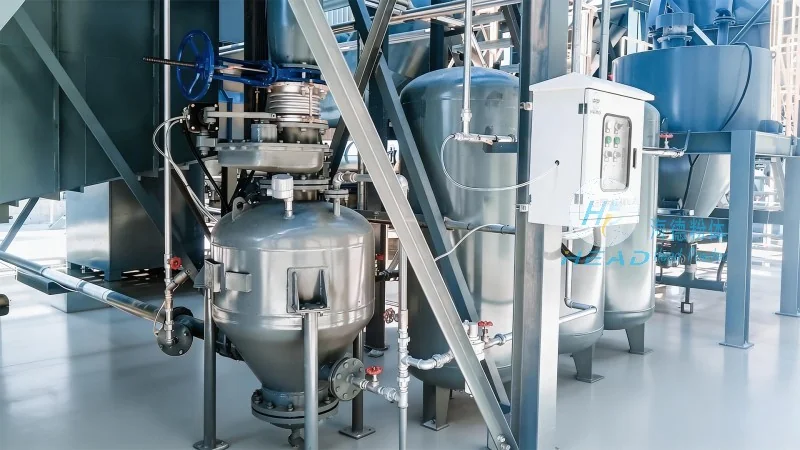
Key Components of a Shredded Paper Powder Conveying System
The core components of a shredded paper powder conveying system typically include a hopper for material storage, a conveyor mechanism (such as a screw conveyor or pneumatic system), and control systems for operation. The hopper is designed to hold the shredded paper powder, ensuring a consistent feed to the conveyor. The conveyor itself is engineered to handle the fine, powdery nature of the material, preventing blockages and ensuring smooth transport. Control systems are integrated to monitor and regulate the flow, speed, and pressure within the system, enhancing operational efficiency and safety.
Design Principles for Efficient Material Handling
Efficient design of a shredded paper powder conveying system is based on several fundamental principles. First, the system must accommodate the unique properties of shredded paper powder, including its fine particle size and potential for static electricity. This requires specialized materials for the conveyor and hopper to prevent material buildup and ensure easy cleaning. Second, the system must be designed for durability and low maintenance, as it will be operating continuously in industrial environments. This includes using robust components that can withstand the abrasive nature of the material and regular wear and tear. Third, the system should be scalable, allowing for adjustments in capacity based on the volume of shredded paper being processed. This flexibility is crucial for adapting to varying production demands.
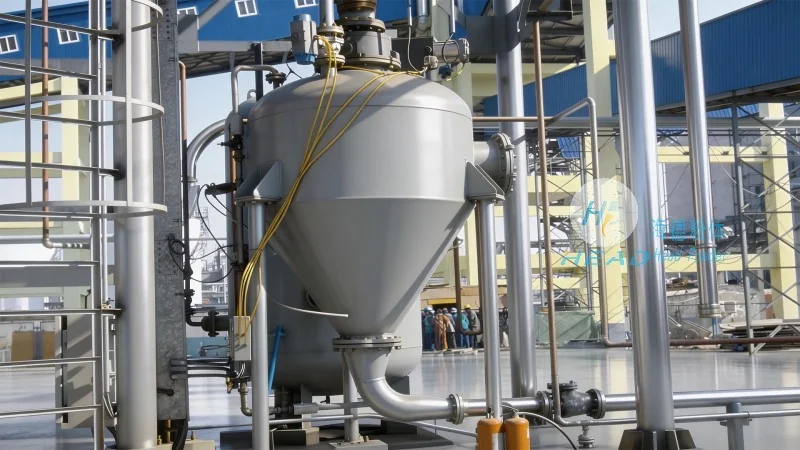
How the System Works: From Hopper to Processing Unit
The operation of a shredded paper powder conveying system begins with the collection of shredded paper in the hopper. The material is then fed into the conveyor mechanism, which transports it to the processing unit. In a pneumatic conveying system, for example, the shredded powder is carried by a stream of air through a pipeline to the destination. This method is particularly effective for fine powders, as it minimizes material loss and ensures a consistent flow. The control system monitors the pressure and flow rate, adjusting the air volume as needed to maintain optimal performance. Once the material reaches the processing unit, it is further processed or recycled, completing the cycle.
Benefits of Using a Shredded Paper Powder Conveying System
Implementing a shredded paper powder conveying system offers several benefits for industrial operations. Firstly, it enhances operational efficiency by ensuring a continuous and reliable flow of material, reducing downtime and increasing productivity. Secondly, it improves safety by containing the material within the system, preventing dust and powder dispersion into the environment. This reduces the risk of respiratory issues and other health hazards for workers. Thirdly, it promotes sustainability by facilitating the recycling process, contributing to environmental conservation. The system also reduces labor costs by automating the material handling process, allowing workers to focus on other critical tasks.
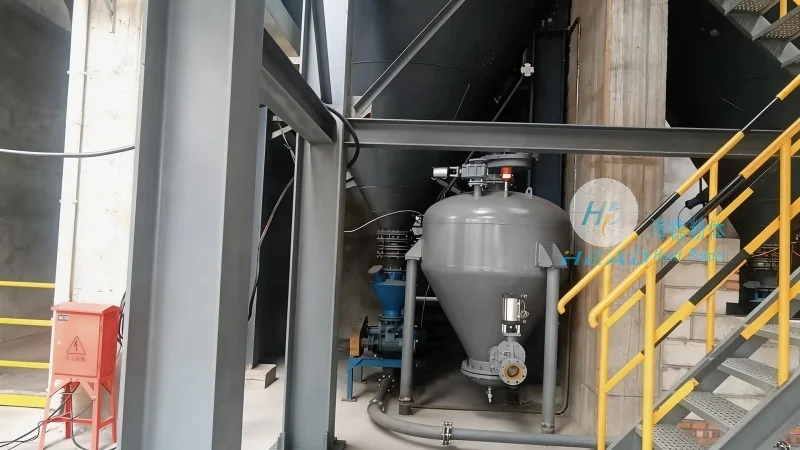
Customization and Integration with Existing Systems
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized shredded paper powder conveying systems tailored to the specific needs of clients. The company, known as headpowder, offers a range of solutions that can be integrated with existing industrial setups. Customization options include adjusting the capacity, conveyor type, and control systems to match the client's production requirements. The company's engineers work closely with clients to understand their operational needs and provide solutions that optimize performance and reduce costs. By leveraging their expertise in powder handling technology, headpowder ensures that each system is designed for maximum efficiency and reliability.
Conclusion: The Importance of Efficient Shredded Paper Powder Conveying
In conclusion, shredded paper powder conveying systems are essential equipment for industries involved in paper recycling and waste processing. The design principles and components of these systems are carefully engineered to handle the unique challenges of transporting fine, powdery materials. By using such systems, companies can improve their operational efficiency, enhance safety, and contribute to environmental sustainability. Shandong HeadPowder Engineering Co., Ltd., as a leading provider in this field, offers high-quality, customized solutions that meet the diverse needs of industrial clients. With their commitment to innovation and quality, headpowder continues to play a vital role in advancing the efficiency of shredded paper powder handling and processing.