With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for various industrial applications. The sulfur pellet pneumatic conveying system is a critical component in many chemical and processing industries, enabling efficient and safe transport of bulk materials like sulfur pellets. This article delves into the fundamental principles behind such systems, highlighting the technical aspects and operational efficiency they offer.
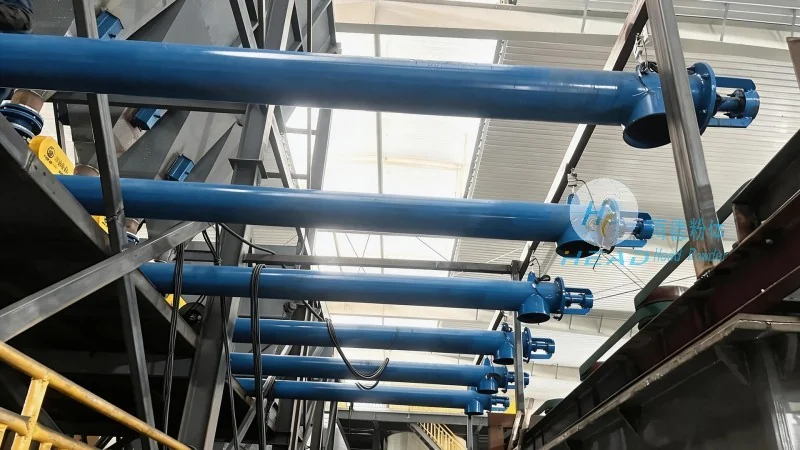
The pneumatic conveying system operates on the principle of using air or gas as the conveying medium to transport solid materials through a pipeline. In the case of sulfur pellets, the system typically employs a positive pressure or negative pressure (or a combination of both) approach to move the material from the source to the destination. The key components include a material feeder, a conveying line, a separator, and a receiver. The material feeder ensures a consistent flow of sulfur pellets into the system, while the conveying line transports the material using pressurized air. The separator then separates the conveyed material from the air, and the receiver collects the final product. This process minimizes material handling risks and enhances operational safety compared to traditional mechanical conveying methods.
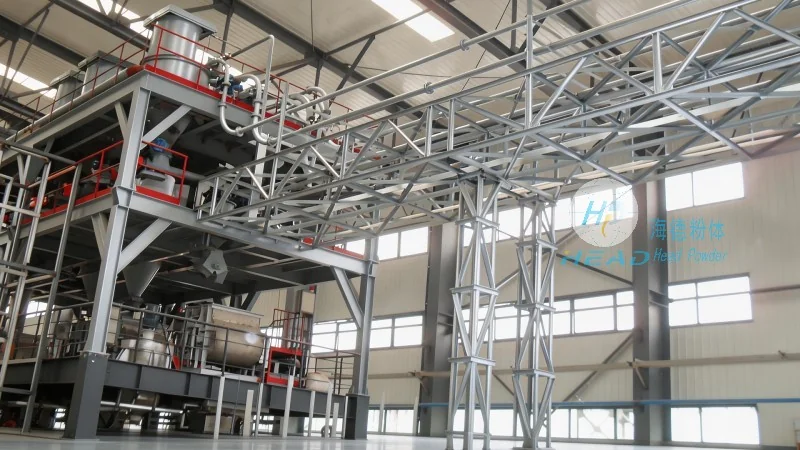
Each component of the sulfur pellet pneumatic conveying system plays a vital role in ensuring efficient operation. The material feeder, often a rotary valve or a screw feeder, controls the flow rate of sulfur pellets into the system, preventing overloading and maintaining a steady feed. The conveying line, usually made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of sulfur pellets and the pressure of the conveying medium. The air compressor or blower provides the necessary pressure to move the material through the line, with the pressure level adjusted based on the distance and material characteristics. The separator, which can be a cyclone or a bag filter, removes the bulk of the material from the air stream, ensuring that the air is clean before it is discharged or recirculated. The receiver, typically a hopper or a silo, stores the conveyed sulfur pellets until they are further processed or shipped.
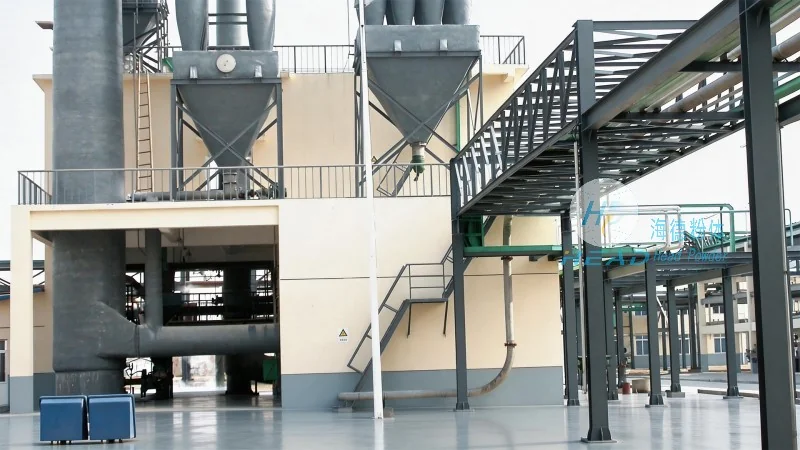
Implementing a pneumatic conveying system for sulfur pellets offers several advantages over traditional methods. Firstly, it reduces the risk of dust exposure and material contamination, as the material is contained within the pipeline. This enhances workplace safety and compliance with environmental regulations. Secondly, the system minimizes material degradation and loss, as the pellets are not subjected to mechanical stress or impact during transport. Thirdly, it improves operational efficiency by automating the material handling process, reducing labor costs and increasing throughput. Additionally, the system can be easily integrated with other processing equipment, such as reactors or storage tanks, to form a seamless production line. The flexibility of pneumatic conveying also allows for adjustments in flow rate and pressure to accommodate varying production demands.
As a reputable engineering company, HeadPowder has extensive experience in designing and installing pneumatic conveying systems tailored to the specific needs of clients. The company's team of engineers and technicians leverages advanced technology and industry best practices to develop customized solutions that optimize material transport efficiency and operational safety. With a focus on quality and reliability, HeadPowder ensures that its systems meet or exceed industry standards, providing long-term performance and minimal maintenance requirements. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including system maintenance, troubleshooting, and performance optimization services.
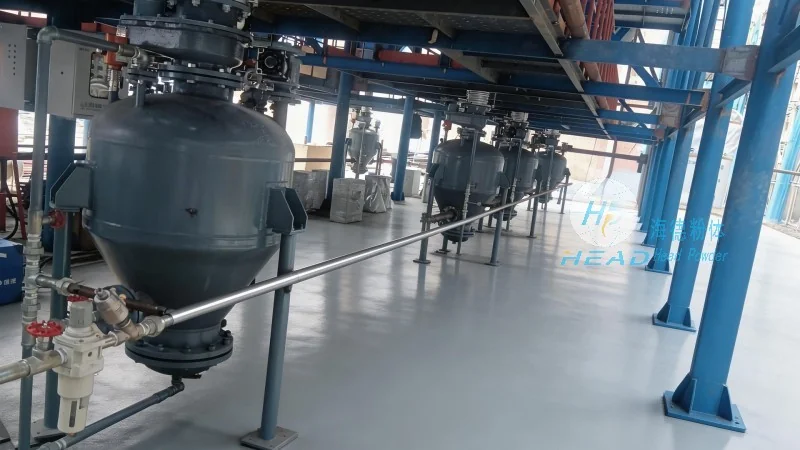
The sulfur pellet pneumatic conveying system represents a sophisticated and efficient solution for transporting bulk materials in industrial settings. By understanding the core principles and components of such systems, as well as the advantages they offer, industries can enhance their operational capabilities and improve overall productivity. HeadPowder, with its expertise and dedication to quality, continues to be a trusted partner in providing reliable pneumatic conveying solutions for sulfur pellet transport and other industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top